Direct Cooling Block Ice Machine Factory - Industrial Ice Equipment Manufacturing Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

direct cooling block ice machine factory

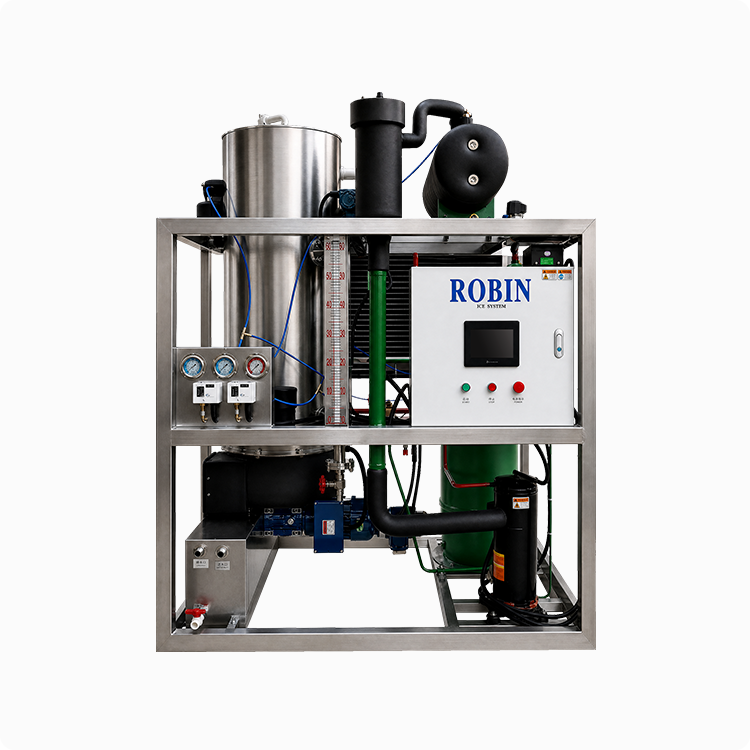
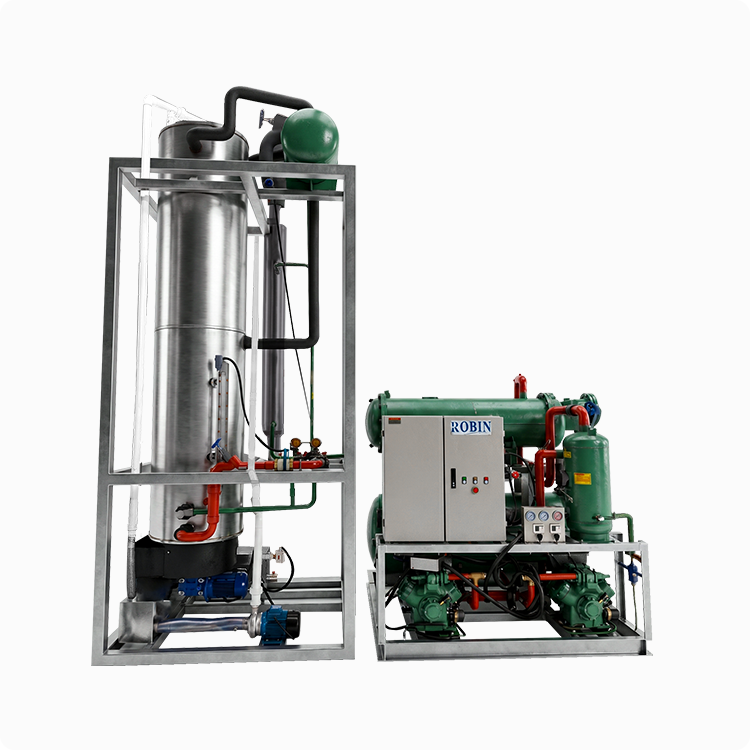
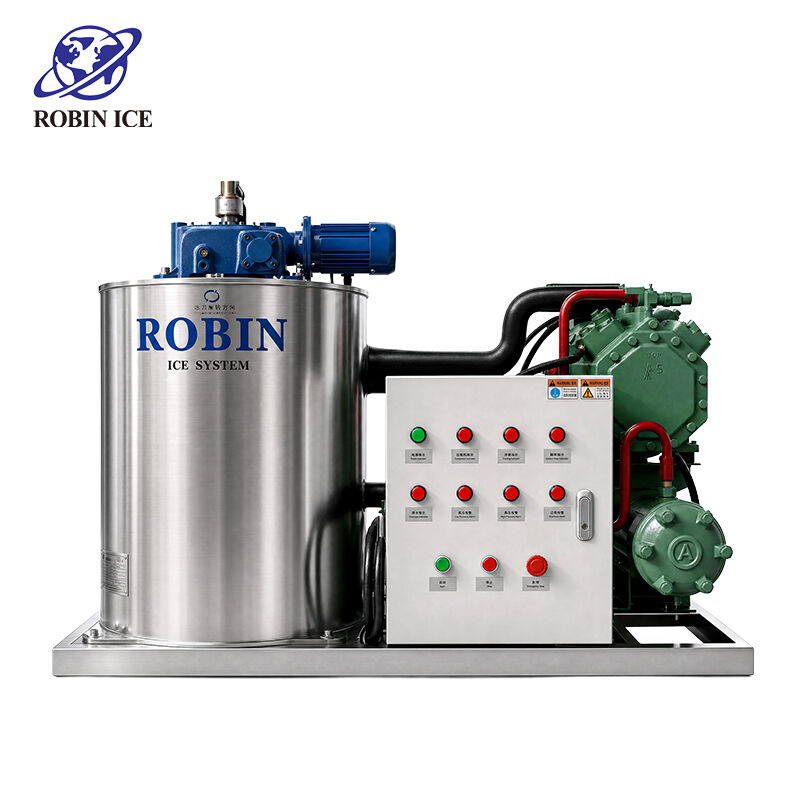
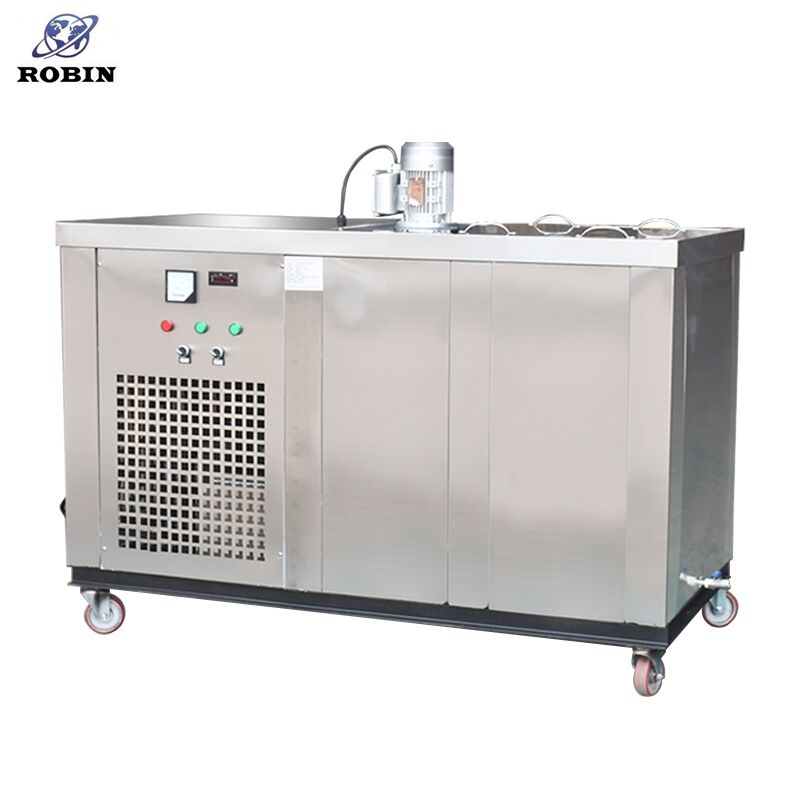
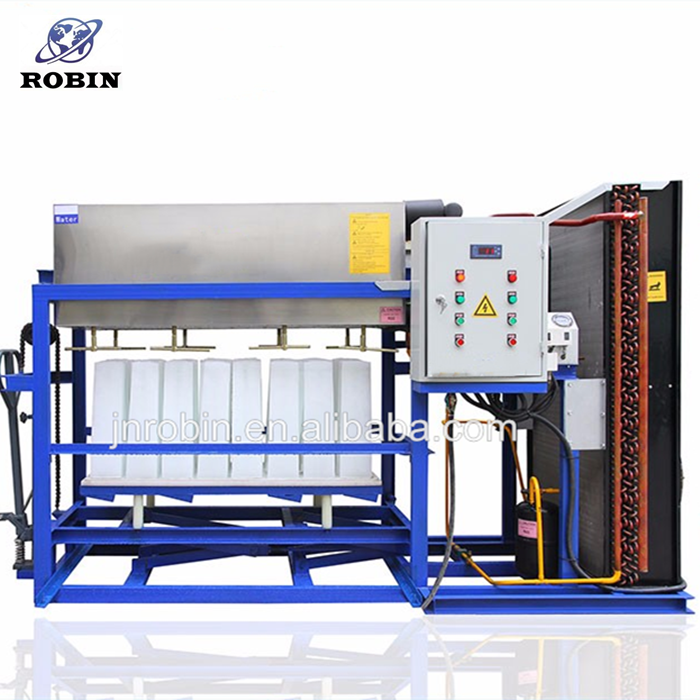
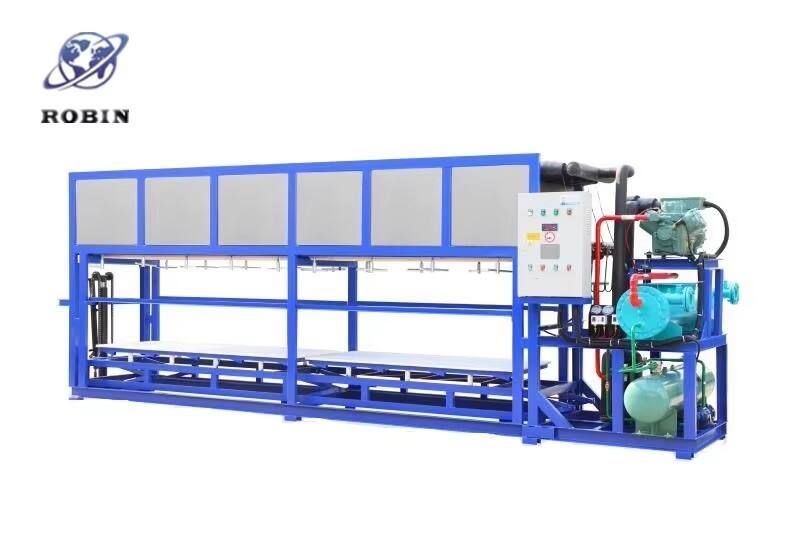
A direct cooling block ice machine factory represents a specialized manufacturing facility dedicated to producing industrial-grade ice-making equipment that creates large, solid blocks of ice through direct refrigeration technology. These factories engineer and assemble sophisticated machinery designed to freeze water into dense, uniform blocks ranging from 25 to 300 kilograms per piece. The direct cooling method distinguishes itself by eliminating intermediate heat transfer fluids, instead using refrigerant that directly contacts the ice-forming containers to achieve rapid and efficient freezing. Modern direct cooling block ice machine factories integrate advanced automation systems, precision temperature controls, and energy-efficient compressors to deliver reliable performance across diverse climatic conditions. The primary function of these facilities involves manufacturing equipment capable of producing crystal-clear ice blocks used extensively in fisheries, food preservation, concrete cooling, chemical processing, and tropical climate applications. Manufacturing processes within a direct cooling block ice machine factory encompass metal fabrication, refrigeration system assembly, electrical component integration, and rigorous quality testing protocols. Engineers at these factories continuously refine designs to enhance ice production capacity, reduce energy consumption, and extend equipment lifespan. The technological infrastructure includes CNC machining centers for precision component manufacturing, welding stations for tank construction, and specialized testing chambers that simulate extreme operating environments. A reputable direct cooling block ice machine factory maintains strict quality control standards, ensuring each unit meets international safety certifications and performance benchmarks. These factories typically offer customization options, allowing clients to specify ice block dimensions, daily production volumes, and auxiliary features such as automatic harvesting systems or brine circulation enhancements. The global demand for block ice in developing regions and industrial sectors drives continuous innovation within direct cooling block ice machine factory operations, pushing manufacturers to develop more compact, efficient, and user-friendly solutions that address specific market needs while maintaining competitive pricing structures.


New Products

Choosing equipment from a direct cooling block ice machine factory delivers substantial practical benefits that directly impact operational efficiency and profitability. The direct cooling technology eliminates the need for brine or secondary refrigerants, which significantly reduces maintenance requirements and operational complexity. Users experience faster ice production cycles because the refrigerant makes direct contact with freezing containers, transferring cold energy more efficiently than indirect methods. This translates to higher daily output using less electricity, cutting energy costs by up to 30 percent compared to traditional brine systems. The machinery produced by a direct cooling block ice machine factory requires minimal supervision once installed, freeing staff to focus on other business activities rather than constantly monitoring ice production. Equipment durability stands out as another major advantage, with robust construction ensuring machines operate reliably for 15 to 20 years with proper maintenance. The absence of corrosive brine solutions means fewer component replacements and lower long-term ownership costs. Ice quality produced by direct cooling systems surpasses alternatives, creating crystal-clear blocks with superior density that melt slower and preserve products longer. This quality advantage proves especially valuable for fishing industries where ice clarity indicates purity and freshness to customers. Installation simplicity represents another practical benefit, as direct cooling block ice machine factory equipment typically requires less complex plumbing and fewer auxiliary systems than brine-based alternatives. Businesses can begin production quickly after installation without extensive training periods. The compact footprint of modern direct cooling systems allows installation in space-constrained facilities, maximizing valuable floor area for other operations. Temperature precision offered by advanced control systems ensures consistent ice quality regardless of ambient conditions, eliminating production variability that can disrupt supply chains. Environmental advantages also matter to forward-thinking businesses, as direct cooling block ice machine factory products use eco-friendly refrigerants that comply with international environmental regulations. The reduced water consumption during production cycles helps businesses in water-scarce regions operate sustainably. Scalability provides flexibility for growing businesses, with modular designs allowing capacity expansion by adding units rather than replacing entire systems. Technical support from established direct cooling block ice machine factory manufacturers ensures rapid troubleshooting and parts availability, minimizing costly downtime. The return on investment typically occurs within two to three years due to energy savings and increased production efficiency. Businesses gain competitive advantages through reliable ice supply that meets peak demand periods without quality compromises or production delays.

Tips And Tricks

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

01

May

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

In food processing and manufacturing environments, maintaining a reliable and uninterrupted supply of ice is not a luxury — it is an operational necessity. From chilling fresh produce to controlling temperatures during meat processing, the dema...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

20

May

How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

Aquaculture operations depend on precise temperature control at every stage of the supply chain, from harvest tanks to processing floors to distribution centers. A flake ice machine for fish sits at the center of this cold chain, producing thin, flat...
View More
How Is Flake Ice Machine for Fish Used in Seafood Processing Facilities?

26

May

How Is Flake Ice Machine for Fish Used in Seafood Processing Facilities?

In seafood processing facilities, temperature control is not a preference — it is a biological necessity. From the moment a fish is harvested to the point it reaches a consumer's plate, maintaining a consistently low temperature determines whet...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

direct cooling block ice machine factory

Advanced Direct Refrigeration Technology Maximizes Production Efficiency

Advanced Direct Refrigeration Technology Maximizes Production Efficiency

The cornerstone innovation of any reputable direct cooling block ice machine factory lies in its proprietary direct refrigeration technology that fundamentally transforms ice production economics. Unlike conventional systems that rely on intermediate cooling mediums such as brine solutions or glycol mixtures, direct cooling technology positions refrigerant-filled evaporator plates in immediate contact with water-filled ice cans. This engineering approach eliminates thermal resistance layers that slow heat transfer in traditional systems, enabling refrigerant to extract heat directly from water at maximum efficiency. The thermodynamic advantage becomes immediately apparent in production timelines, with complete freezing cycles shortened by 20 to 40 percent depending on block size and ambient conditions. A direct cooling block ice machine factory invests heavily in optimizing evaporator plate design, utilizing computational fluid dynamics to model refrigerant flow patterns and maximize surface contact area. Advanced manufacturing techniques create micro-channel evaporators that distribute refrigerant uniformly across freezing surfaces, preventing hot spots that cause uneven ice formation. The precision engineering ensures every ice block achieves consistent density and clarity, meeting stringent quality standards demanded by premium markets. Energy efficiency gains from direct cooling technology compound over time, with typical installations consuming 25 to 35 percent less electricity than equivalent-capacity brine systems. This efficiency stems from eliminating the energy required to circulate and maintain secondary cooling fluids at precise temperatures. Modern direct cooling block ice machine factory products incorporate variable-speed compressors that adjust refrigeration capacity to match actual demand, further reducing energy waste during partial-load operations. The technology also enhances operational safety by removing the risks associated with brine handling, including chemical exposure, spillage cleanup, and disposal regulations. Maintenance intervals extend significantly because direct systems contain fewer moving parts and eliminate pumps, heat exchangers, and filtration equipment required by brine circulation. Operators appreciate the simplified troubleshooting process, as direct cooling systems present fewer potential failure points. The environmental profile of direct cooling block ice machine factory equipment aligns with global sustainability initiatives, using next-generation refrigerants with low global warming potential while achieving superior performance metrics. Investment in direct cooling technology positions businesses for long-term competitiveness through lower operating costs, higher reliability, and superior product quality that commands premium pricing in discerning markets.
Customizable Production Capacity Meets Diverse Industry Requirements

Customizable Production Capacity Meets Diverse Industry Requirements

A distinguishing characteristic of leading direct cooling block ice machine factory operations is their commitment to manufacturing flexible, scalable equipment that adapts to vastly different industry requirements and operational scales. Recognizing that a small fishing cooperative has fundamentally different needs than a large-scale food processing facility, these factories engineer modular systems with production capacities ranging from 1 ton to over 100 tons of ice daily. The customization process begins with detailed consultation where factory engineers assess specific application requirements, ambient operating conditions, available utilities, and space constraints. This information guides the configuration of compressor capacity, evaporator quantity, ice can dimensions, and auxiliary systems. A direct cooling block ice machine factory maintains extensive component inventories and flexible manufacturing processes that accommodate custom specifications without excessive lead times or cost premiums. The modular architecture allows businesses to start with baseline capacity and expand incrementally as demand grows, protecting initial capital investment while ensuring scalability. Each module operates independently, providing redundancy that maintains partial production even during maintenance or component failure. This reliability proves critical for industries where ice supply interruptions cause significant financial losses or product spoilage. Customization extends to ice block dimensions, with direct cooling block ice machine factory equipment producing blocks from compact 10-kilogram sizes suitable for retail distribution to massive 300-kilogram industrial blocks used in concrete cooling or large-vessel fishing operations. The flexibility accommodates regional preferences and specific application requirements without compromising production efficiency. Advanced control systems developed by direct cooling block ice machine factory engineering teams allow operators to program multiple production profiles, switching between different block sizes or production schedules based on demand patterns. Automation options range from basic timer controls suitable for small operations to sophisticated programmable logic controllers that integrate with facility management systems in large industrial plants. The customization philosophy extends to climate adaptation, with tropical-rated components, enhanced condenser capacity, and corrosion-resistant materials for coastal installations. Cold-climate configurations include heated drain systems and insulated enclosures that maintain optimal operating temperatures in sub-zero environments. A professional direct cooling block ice machine factory provides comprehensive technical documentation, training programs, and ongoing support that ensures operators maximize their customized equipment's potential regardless of technical expertise levels.
Superior Ice Quality Delivers Competitive Market Advantages

Superior Ice Quality Delivers Competitive Market Advantages

The ice quality produced by equipment from a specialized direct cooling block ice machine factory represents a critical competitive differentiator that directly impacts customer satisfaction and market positioning. Direct cooling technology creates exceptionally clear, dense ice blocks that exhibit superior performance characteristics compared to ice produced through alternative methods. The clarity results from controlled freezing rates that allow dissolved gases and impurities to escape before water solidifies, producing transparent blocks that signal purity and quality to end customers. This visual appeal proves particularly valuable in fresh fish markets where ice clarity serves as a proxy indicator for product freshness and handling standards. The density achieved through direct cooling block ice machine factory equipment exceeds that of flake or tube ice by significant margins, translating to slower melting rates that extend product preservation times. Fishing vessels equipped with dense block ice can extend voyage durations without compromising catch quality, directly increasing operational profitability. The uniform freezing process eliminates internal stress fractures that cause premature cracking, ensuring blocks maintain structural integrity during handling and transportation. Food processors value this durability because intact blocks provide more predictable cooling performance and reduce waste from unusable ice fragments. The purity of ice produced by direct cooling block ice machine factory equipment meets food-grade standards without additional treatment, as the direct cooling process avoids contamination risks associated with brine systems where chemical residues might transfer to ice surfaces. This inherent purity reduces regulatory compliance burdens and eliminates concerns about chemical contamination in food contact applications. The consistent quality output from direct cooling systems enables businesses to build reliable brand reputations, commanding premium pricing in markets where quality differentiation matters. Temperature uniformity throughout each block ensures predictable melting behavior, allowing precise cooling calculations in industrial applications such as concrete temperature control during large pours. The hardness of blocks produced by direct cooling block ice machine factory equipment withstands mechanical handling in automated storage and retrieval systems without excessive breakage. This mechanical strength reduces handling losses and maintains operational efficiency in high-volume distribution operations. Quality consistency across production batches eliminates the variability that complicates inventory management and customer relationships. Businesses can confidently commit to supply agreements knowing their direct cooling block ice machine factory equipment will deliver specified quality parameters regardless of seasonal variations or production volumes. The superior ice quality ultimately translates to enhanced customer retention, reduced product losses, extended market reach, and improved profit margins that justify the investment in premium direct cooling block ice machine factory equipment.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000