Hygiene Control and Quality Assurance for Food Safety Compliance
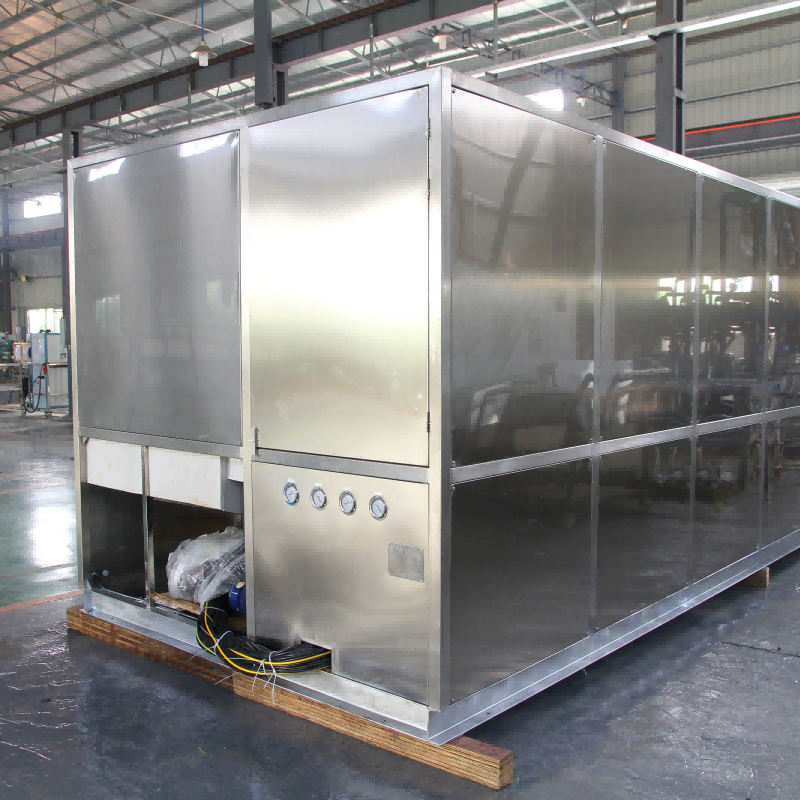
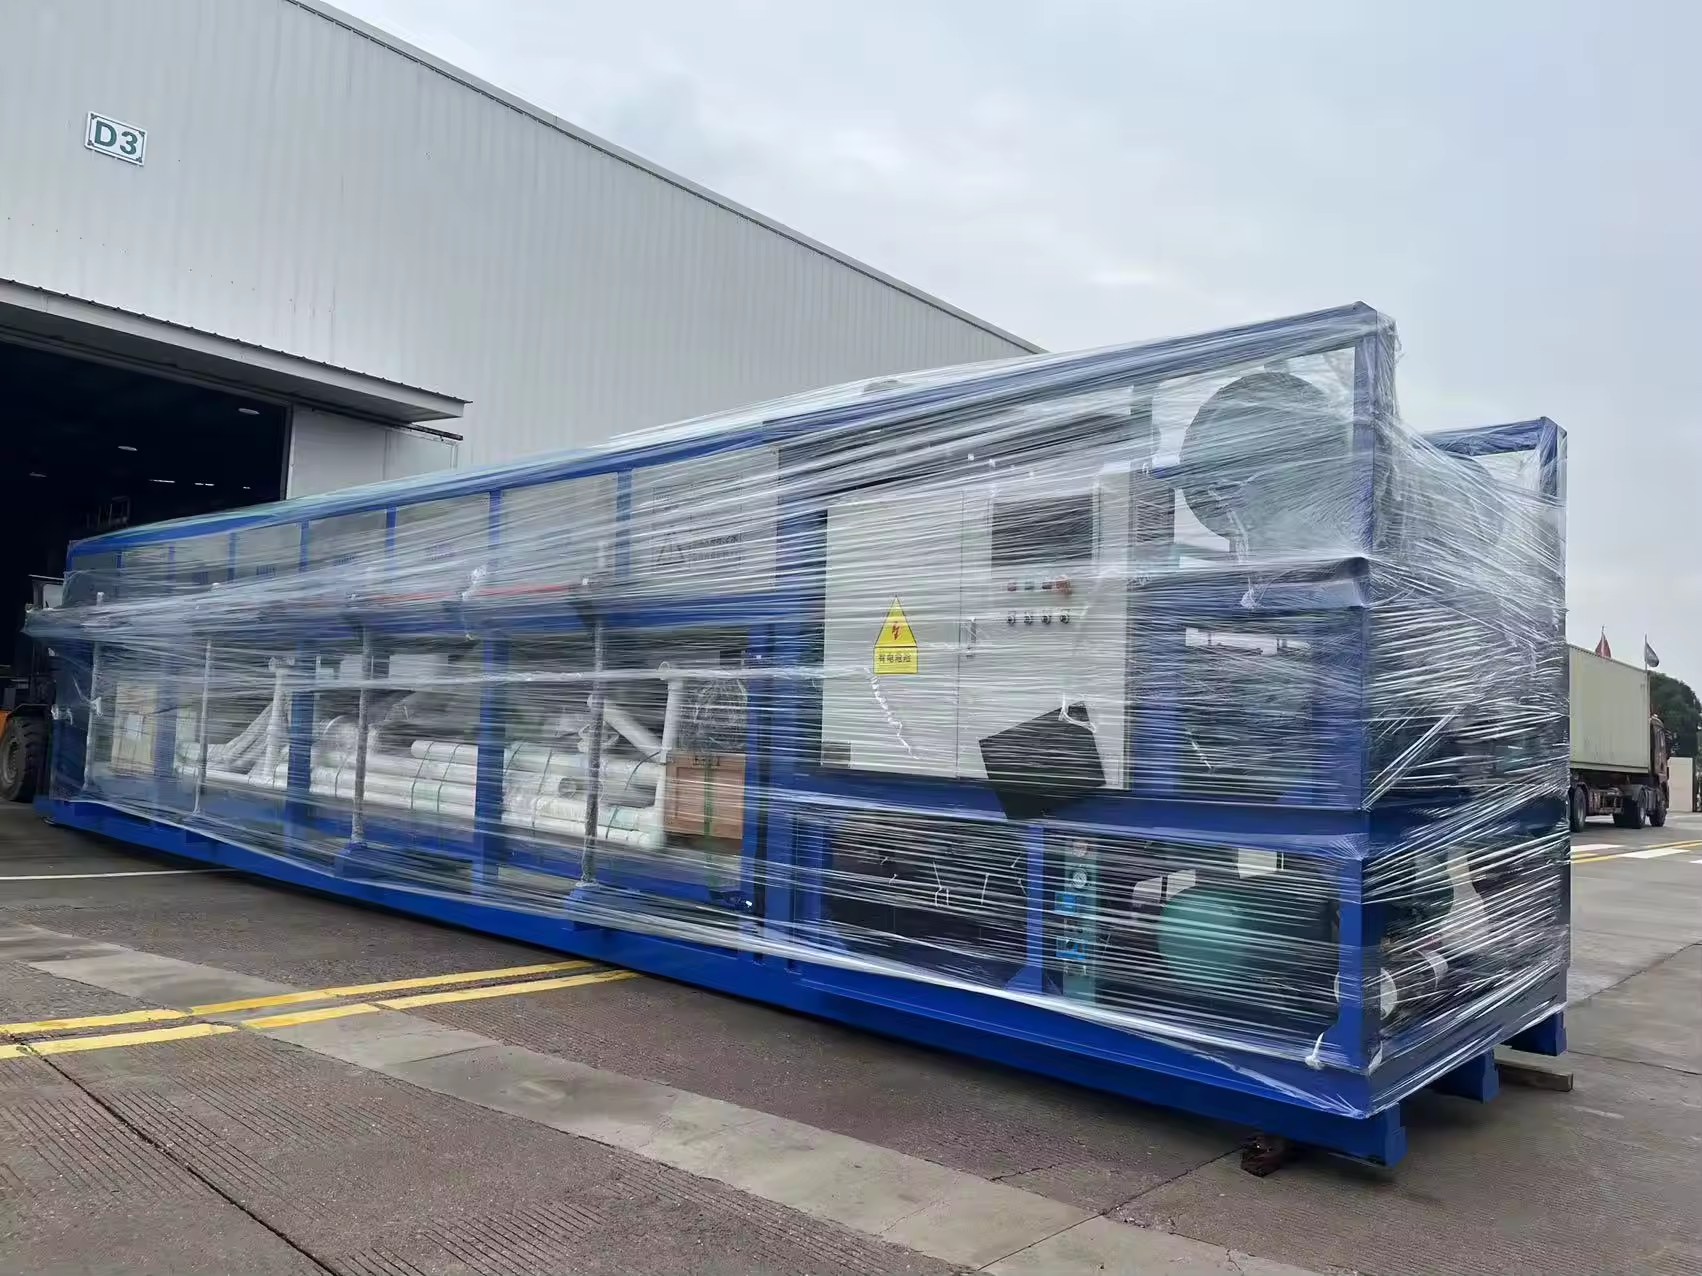
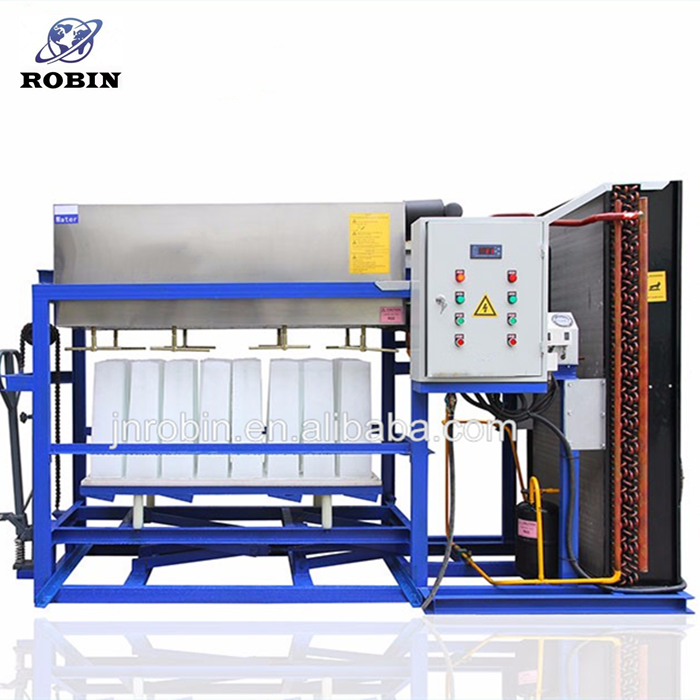
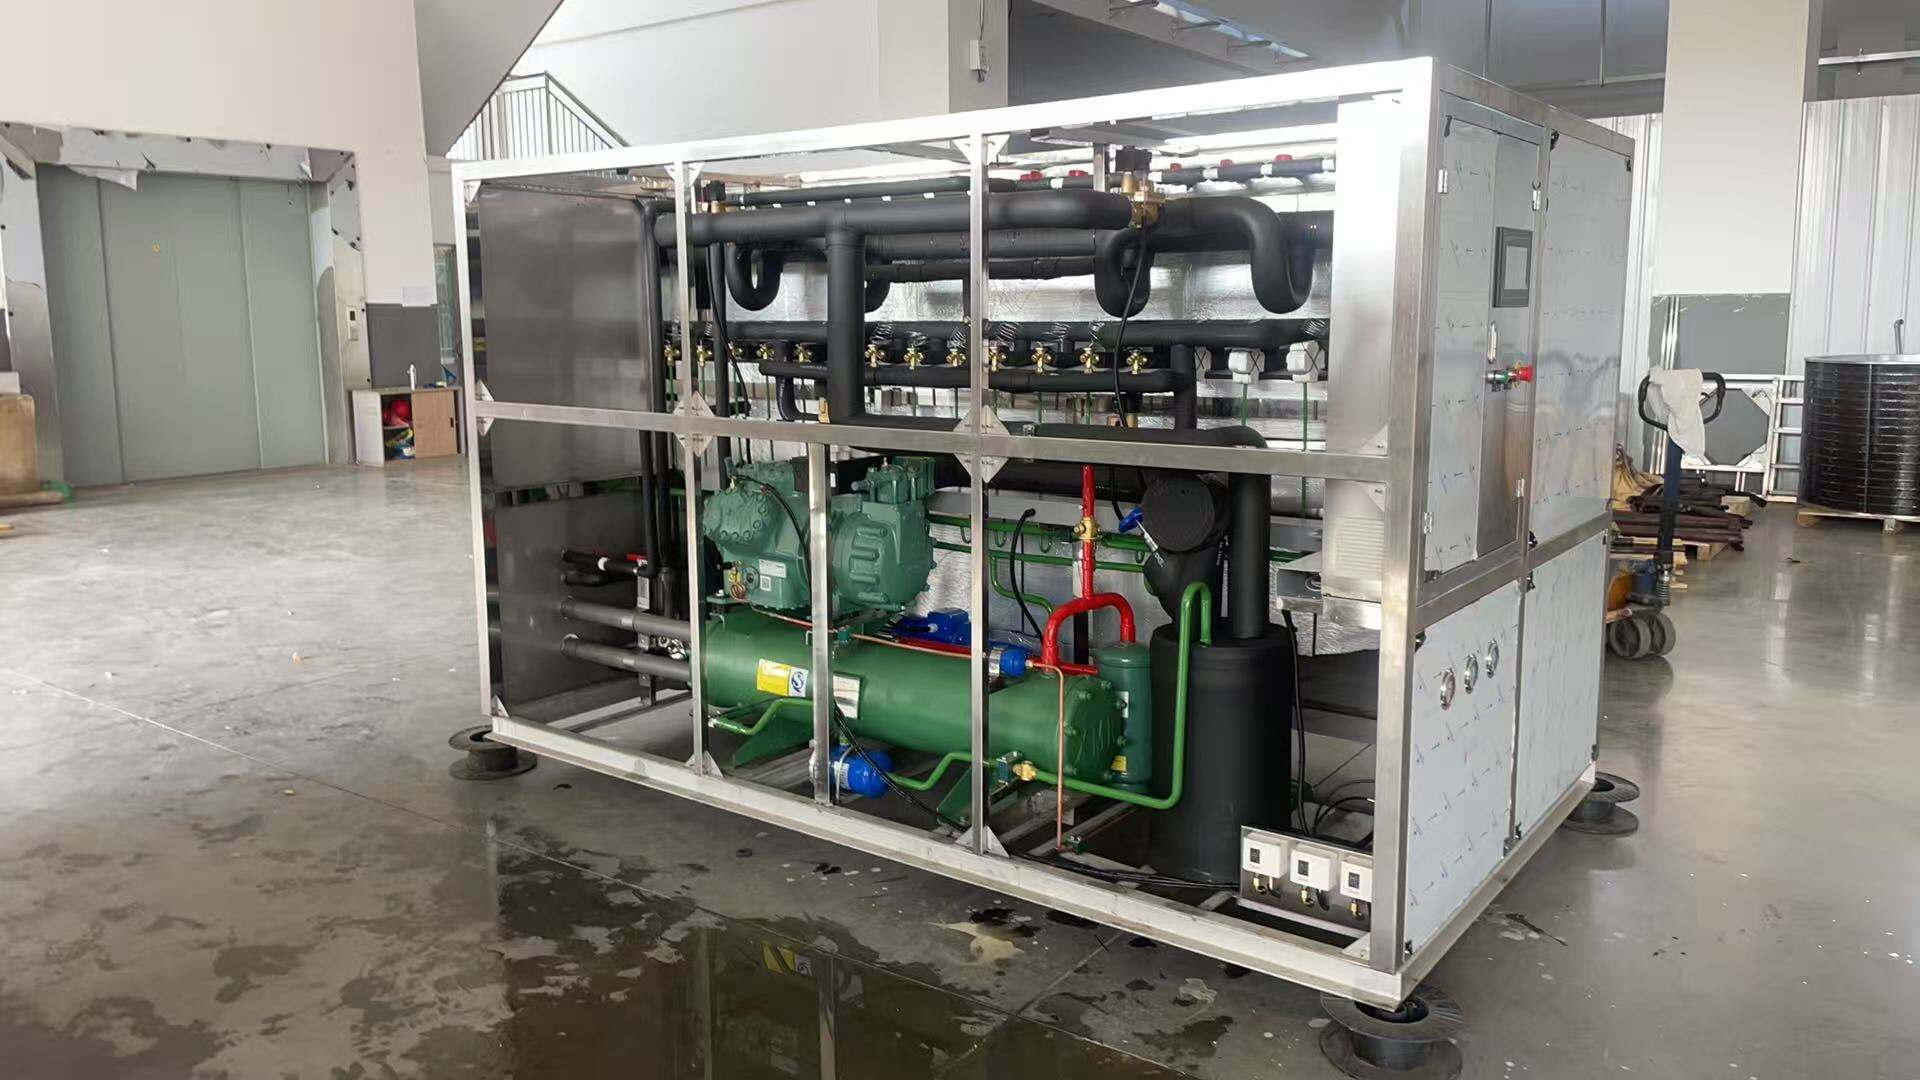
The block ice machine for cold chain provides businesses with complete control over ice quality and hygiene standards, addressing critical food safety concerns that arise when relying on external ice suppliers whose production processes remain invisible to end users. When businesses produce their own ice using a block ice machine for cold chain, they manage every aspect of the production environment, from water source filtration to equipment sanitation, ensuring that ice meets or exceeds the strictest food safety regulations and industry standards. The ability to use filtered, purified water as the raw material eliminates concerns about contaminants, minerals, or biological agents that might compromise product safety or introduce off-flavors that affect the goods being preserved. Modern block ice machine for cold chain systems incorporate food-grade stainless steel construction throughout water contact surfaces, preventing corrosion, bacterial growth, and chemical leaching that could occur with inferior materials. The closed production system minimizes exposure to airborne contaminants, dust, and environmental pollutants that represent significant risks in open ice production or storage facilities operated by third-party suppliers. Businesses can implement comprehensive cleaning protocols tailored to their specific requirements, scheduling sanitation cycles that align with production schedules and regulatory inspection timelines without depending on supplier certifications that may not reflect current conditions. The block ice machine for cold chain enables traceability throughout the production process, documenting water sources, production dates, and quality control measures that support food safety audits and regulatory compliance verification. This documentation capability proves invaluable during inspections or in response to customer inquiries about cold chain integrity, demonstrating professional commitment to quality preservation. The consistent ice quality produced by block ice machine for cold chain equipment eliminates variability that occurs when sourcing from multiple suppliers or different production batches, ensuring that every ice block delivers identical cooling performance and purity standards. Businesses serving sensitive markets such as pharmaceuticals, premium seafood, or organic produce benefit from the ability to certify their entire cold chain process, including ice production, as meeting specialized standards that command premium pricing and customer loyalty. The block ice machine for cold chain supports implementation of Hazard Analysis and Critical Control Points protocols, with ice production identified as a controlled process point where businesses can monitor, measure, and verify compliance with established safety parameters, reducing liability exposure and protecting brand reputation from contamination incidents that could devastate customer trust and market position.

 EN