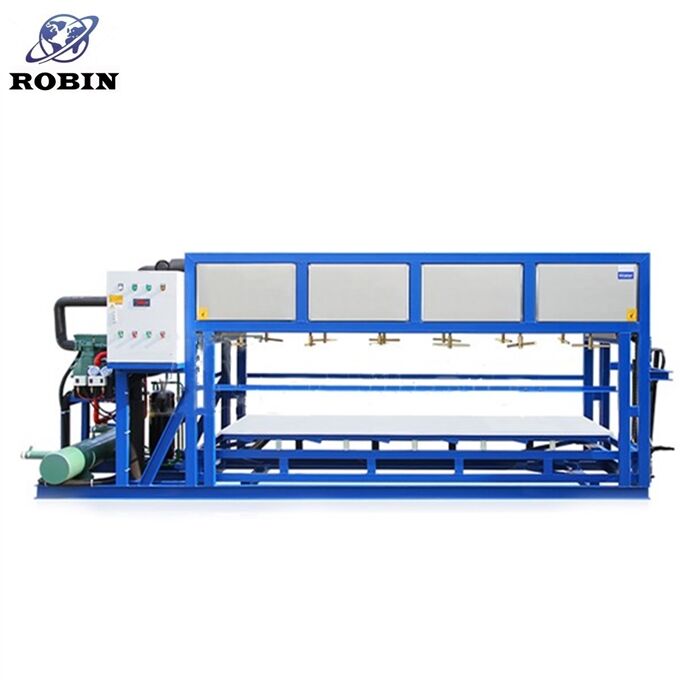
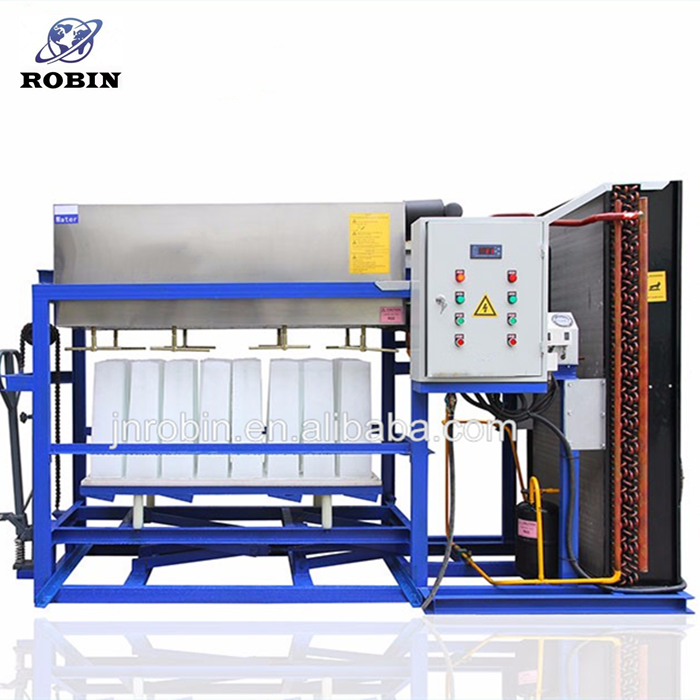
Industrial Direct Cooling Block Ice Machine - High-Efficiency Ice Production Systems

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial direct cooling block ice machine

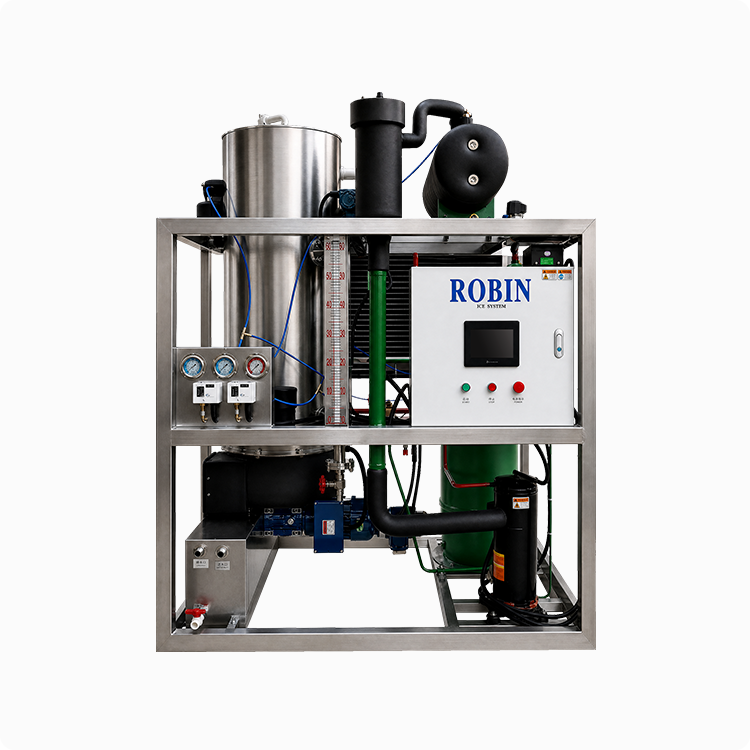
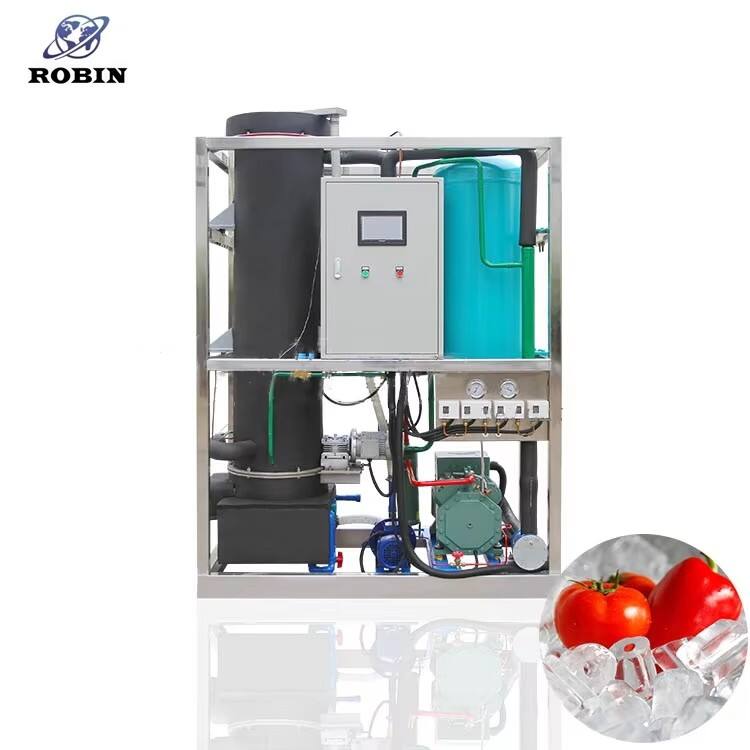
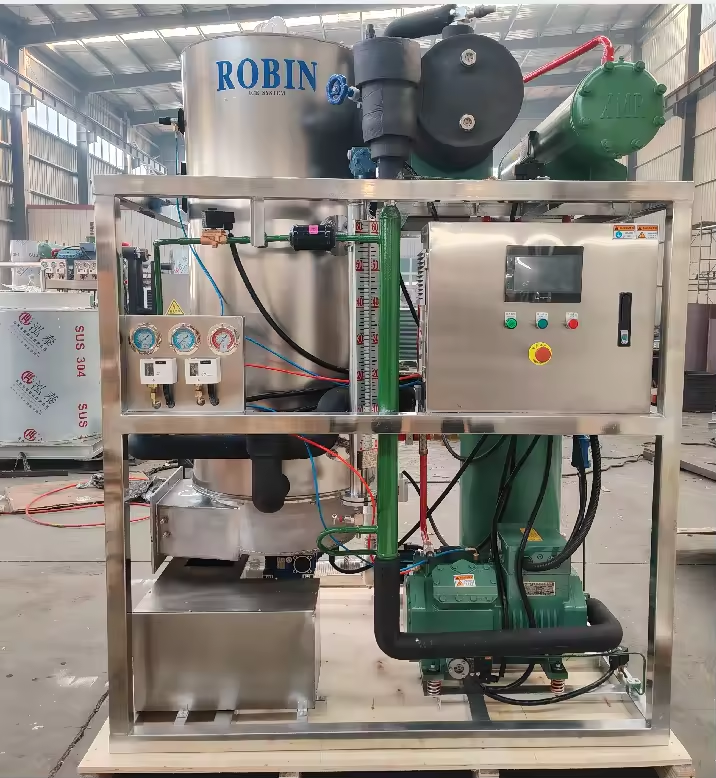
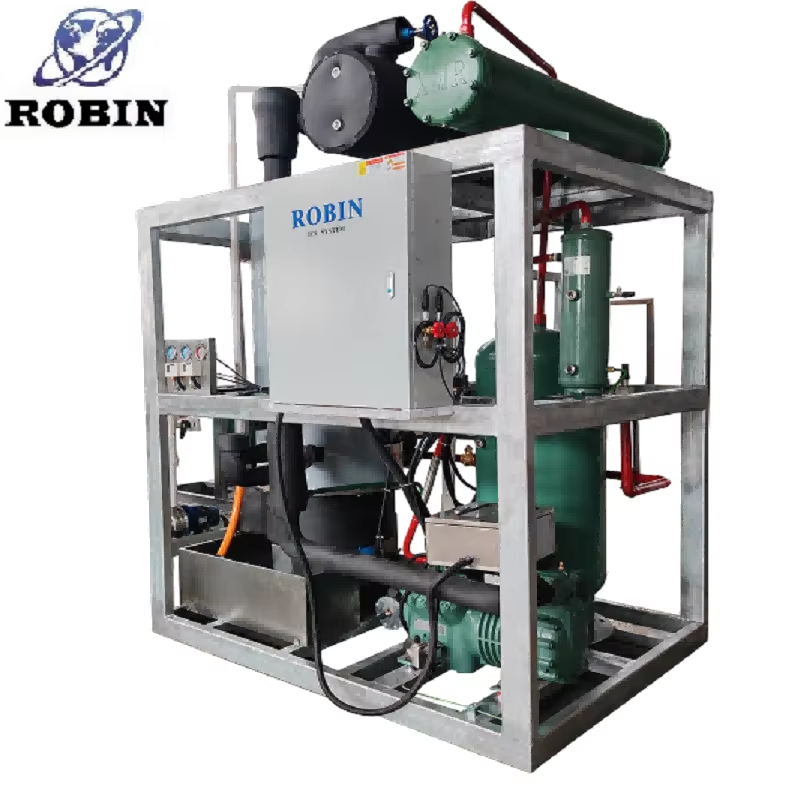
The industrial direct cooling block ice machine represents a sophisticated refrigeration system designed to produce large-scale ice blocks through an efficient direct cooling methodology. This equipment operates by circulating refrigerant directly through evaporator plates that come into contact with water-filled containers, creating solid ice blocks that typically range from 25 to 100 kilograms per block. The direct cooling block ice machine utilizes advanced compressor technology combined with precision-engineered evaporator systems to achieve rapid freezing cycles while maintaining consistent ice quality. These machines find extensive application across fisheries, food processing facilities, concrete cooling operations, chemical industries, and large-scale cold chain logistics operations. The core function of an industrial direct cooling block ice machine centers on transforming large volumes of water into dense, crystal-clear ice blocks that offer superior cooling capacity and extended melting duration compared to other ice formats. The technological framework incorporates automated water filling systems, intelligent defrosting mechanisms, and computerized control panels that monitor temperature fluctuations, refrigerant pressure, and production cycles. Modern industrial direct cooling block ice machines feature stainless steel construction that ensures hygiene standards while providing corrosion resistance in demanding operational environments. The production capacity of these systems varies significantly, with industrial models capable of generating anywhere from 1 ton to 100 tons of block ice per day, depending on configuration and operational parameters. The direct cooling methodology eliminates the need for brine solutions, resulting in cleaner ice production and reduced maintenance requirements. These machines integrate seamlessly into existing cold storage infrastructure, offering businesses a reliable solution for continuous ice production without compromising on quality or efficiency. The versatility of the industrial direct cooling block ice machine makes it an indispensable asset for operations requiring consistent access to large quantities of high-quality ice blocks for preservation, transportation, and industrial cooling applications.

New Product Recommendations

Businesses investing in an industrial direct cooling block ice machine gain immediate access to cost-effective ice production that significantly reduces operational expenses compared to purchasing ice from external suppliers. The direct cooling technology eliminates intermediary cooling agents, which translates to faster freezing times and lower energy consumption per kilogram of ice produced. This efficiency directly impacts your bottom line by reducing electricity costs while increasing daily production output. The machine operates with minimal supervision, freeing your staff to focus on core business activities rather than managing complex ice production processes. You receive ice blocks with exceptional density and purity, characteristics that extend melting time and provide superior cooling performance for your products. The robust construction ensures years of reliable operation with minimal downtime, protecting your investment and guaranteeing consistent ice availability during peak demand periods. Installation requires straightforward setup procedures that most facilities can accommodate without extensive modifications to existing infrastructure. The automated control systems prevent human error and maintain optimal production conditions around the clock, ensuring every ice block meets your quality standards. You benefit from flexible production scheduling that allows adjustment of output volumes based on seasonal demand fluctuations or specific project requirements. The hygienic design features smooth surfaces and food-grade materials that comply with health regulations, making the ice suitable for direct contact with consumable products. Maintenance procedures remain simple and infrequent, with accessible components that reduce service costs and minimize production interruptions. The industrial direct cooling block ice machine adapts to various water quality conditions, though filtered water input optimizes performance and extends equipment lifespan. Your operation gains independence from unreliable ice suppliers, eliminating delivery delays and ensuring uninterrupted access to ice regardless of external market conditions. The compact footprint of modern units maximizes floor space utilization, allowing installation in facilities with limited square footage. Temperature consistency throughout the freezing process produces uniform ice blocks without air pockets or weak spots that could compromise structural integrity during handling and transportation. The system generates ice blocks in standardized dimensions that stack efficiently in storage areas and transport vehicles, optimizing space utilization throughout your cold chain. Energy-efficient compressors and optimized refrigerant circuits reduce environmental impact while meeting sustainability goals that increasingly influence purchasing decisions and corporate responsibility initiatives.

Latest News

How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

06

May

How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

The ice tube machine has become an essential piece of equipment across a wide range of commercial operations, from busy restaurant kitchens to large-scale food processing facilities. Its ability to produce cylindrical ice in consistent shapes and siz...
View More
How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

12

May

How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

In food processing, healthcare, fisheries, and beverage production, the integrity of ice directly affects product safety and regulatory compliance. A tube ice maker machine is engineered from the ground up to meet the demanding hygiene standards that...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial direct cooling block ice machine

Superior Energy Efficiency Through Direct Cooling Technology

Superior Energy Efficiency Through Direct Cooling Technology

The industrial direct cooling block ice machine achieves remarkable energy efficiency by employing a direct refrigerant-to-water heat exchange system that eliminates unnecessary thermal transfer stages found in traditional ice-making methods. This technological approach circulates refrigerant directly through aluminum or stainless steel evaporator plates that form the walls of ice-making containers, creating an immediate thermal connection between the cooling source and the water being frozen. By removing the brine solution intermediary used in older systems, the direct cooling block ice machine reduces energy losses associated with heating and cooling secondary fluids, resulting in energy savings that can reach 30 to 40 percent compared to conventional brine-based systems. The compressor operates more efficiently because it maintains optimal pressure ratios without compensating for the thermal resistance introduced by brine solutions. Modern industrial direct cooling block ice machines incorporate variable frequency drive technology that adjusts compressor speed based on actual cooling demand, preventing energy waste during partial load conditions and startup sequences. The intelligent control systems monitor ambient temperature, water input temperature, and ice formation progress to optimize refrigerant flow and compressor operation throughout each production cycle. This precision management ensures the machine consumes only the energy necessary to achieve target ice production volumes, avoiding the overcooling and energy spikes common in less sophisticated systems. The direct contact between evaporator surfaces and water accelerates heat transfer rates, shortening freezing cycles and allowing the machine to produce more ice per kilowatt-hour of electricity consumed. Facilities operating multiple shifts benefit particularly from this efficiency, as reduced energy consumption compounds into substantial cost savings over months and years of continuous operation. The environmental advantages extend beyond operational costs, as lower energy consumption translates to reduced carbon emissions and a smaller environmental footprint for your ice production activities. The industrial direct cooling block ice machine supports corporate sustainability initiatives while delivering tangible financial returns through decreased utility expenses, making it an investment that aligns economic performance with environmental responsibility.
Exceptional Ice Quality and Structural Integrity

Exceptional Ice Quality and Structural Integrity

The industrial direct cooling block ice machine produces ice blocks with superior density, clarity, and structural characteristics that outperform ice generated through alternative production methods. The direct cooling process creates a controlled freezing environment where water solidifies gradually from the outside surfaces inward, allowing dissolved gases and impurities to migrate toward the center where they can be managed through proper water circulation and overflow systems. This methodical freezing pattern results in ice blocks with minimal air entrapment, producing crystal-clear ice that not only looks more appealing but also melts more slowly due to its compact molecular structure. The density achieved through direct cooling technology typically exceeds 900 kilograms per cubic meter, approaching the theoretical maximum density of pure ice and ensuring each block delivers maximum cooling capacity per unit volume. This density advantage becomes critically important in applications where space constraints limit the quantity of ice that can be stored or transported, as denser ice provides more cooling power in less physical space. The structural integrity of ice blocks produced by an industrial direct cooling block ice machine withstands the rigors of handling, stacking, and transportation without cracking or fragmenting, reducing product loss and maintaining cooling effectiveness throughout the distribution chain. The uniform freezing conditions eliminate weak points and stress fractures that develop in ice produced through rapid or uneven cooling processes, ensuring each block maintains its shape and structural coherence even under mechanical stress. Food processing operations particularly value this quality consistency, as reliable ice block performance ensures product temperatures remain within safe ranges during processing and storage. The purity of ice produced through direct cooling methods meets stringent food safety standards, making it suitable for direct contact with seafood, meat, poultry, and produce without risk of contamination or quality degradation. The absence of brine solutions in the production process eliminates any possibility of salt or chemical residue contaminating the ice, a critical consideration for applications in food service, healthcare, and pharmaceutical industries where purity requirements are non-negotiable. The industrial direct cooling block ice machine delivers consistent quality across every production cycle, ensuring your operations receive predictable performance that supports quality control protocols and customer satisfaction guarantees.
Operational Reliability and Low Maintenance Requirements

Operational Reliability and Low Maintenance Requirements

The industrial direct cooling block ice machine distinguishes itself through exceptional operational reliability that minimizes downtime and reduces the total cost of ownership over the equipment's service life. The simplified design inherent to direct cooling systems eliminates complex brine circulation pumps, heat exchangers, and associated plumbing that represent common failure points in traditional ice-making equipment. Fewer mechanical components translate directly to reduced maintenance requirements and lower probability of unexpected breakdowns that disrupt production schedules. The robust construction employs industrial-grade compressors, corrosion-resistant evaporator materials, and heavy-duty structural frames designed to withstand continuous operation in demanding industrial environments. Manufacturers typically engineer these machines for operational lifespans exceeding 15 to 20 years when properly maintained, providing long-term value that justifies the initial capital investment. The automated control systems continuously monitor critical operating parameters including refrigerant pressures, compressor temperatures, water levels, and ice formation progress, alerting operators to potential issues before they escalate into costly failures. This predictive capability allows maintenance teams to schedule service activities during planned downtime rather than responding to emergency breakdowns that halt production and require expensive expedited repairs. The industrial direct cooling block ice machine requires minimal daily intervention, with most operational tasks limited to ensuring adequate water supply and removing completed ice blocks from the production chambers. Cleaning procedures remain straightforward, typically involving periodic flushing of water systems and inspection of evaporator surfaces to prevent scale buildup that could impair heat transfer efficiency. The absence of brine solutions eliminates the need for chemical testing, solution replacement, and disposal procedures that add complexity and cost to ice production operations. Replacement parts for direct cooling systems are widely available and standardized across manufacturers, preventing supply chain delays and reducing inventory costs for facilities maintaining spare parts stocks. The modular design of modern industrial direct cooling block ice machines allows technicians to access and service individual components without disassembling entire systems, minimizing repair time and labor costs. Training requirements for operating personnel remain modest, as intuitive control interfaces and automated operation sequences reduce the technical knowledge needed for day-to-day management. This operational simplicity makes the industrial direct cooling block ice machine accessible to facilities without specialized refrigeration expertise, democratizing access to reliable ice production capabilities across diverse industries and geographic regions.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000