Direct Cooling Block Ice Machine Supplier - Industrial Ice Production Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

direct cooling block ice machine supplier

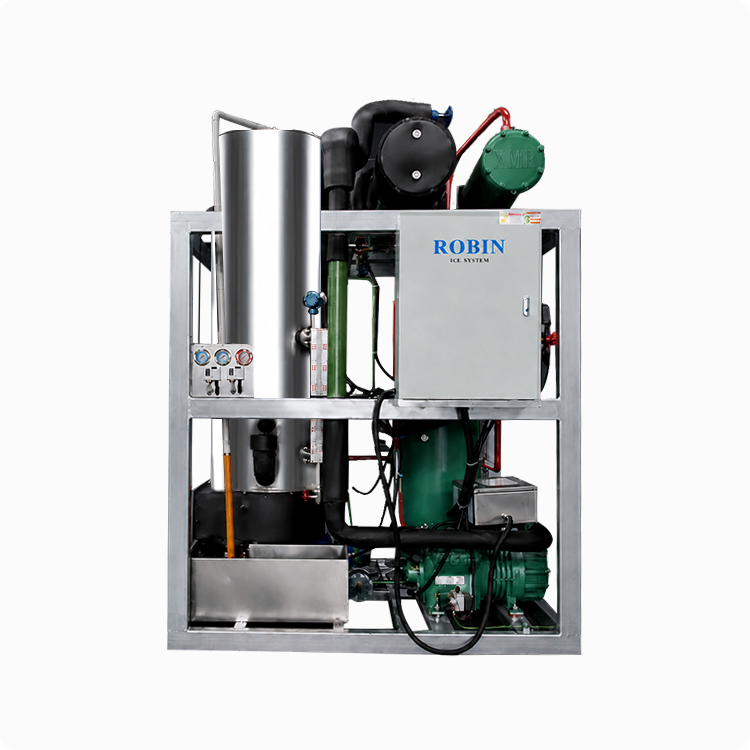
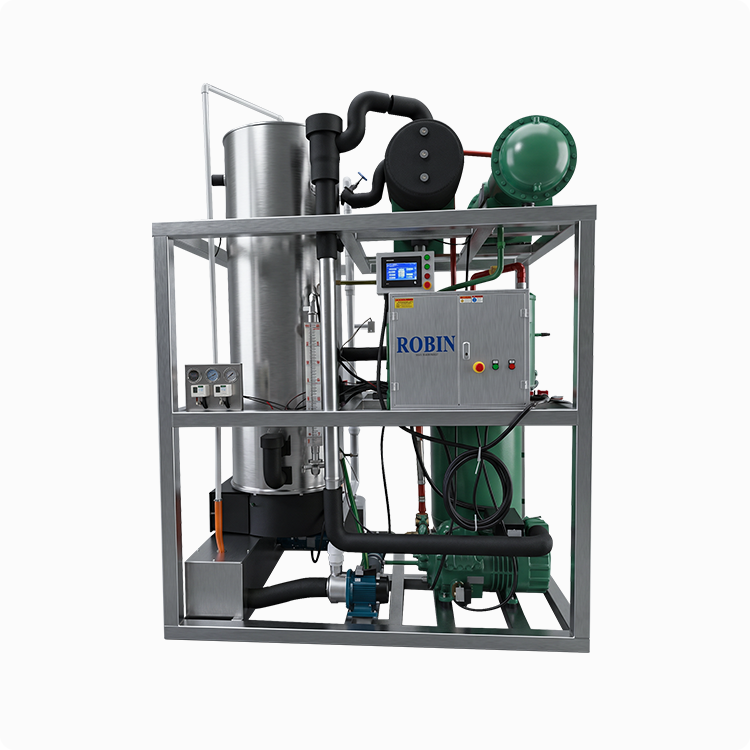
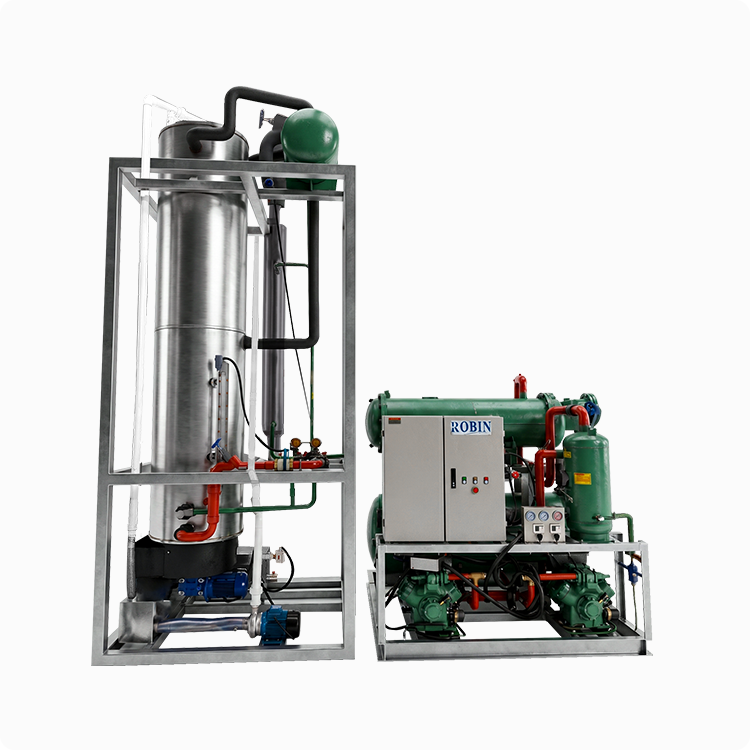
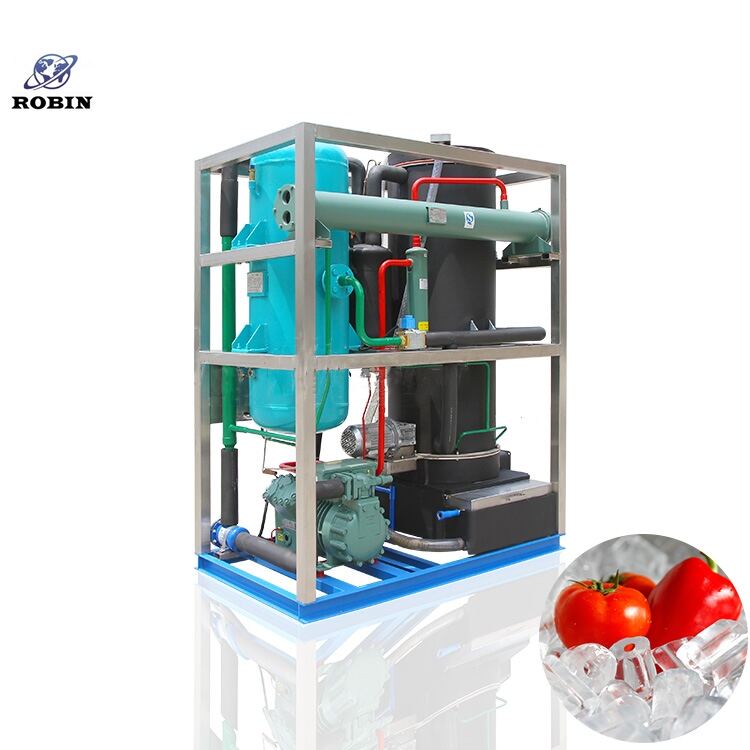
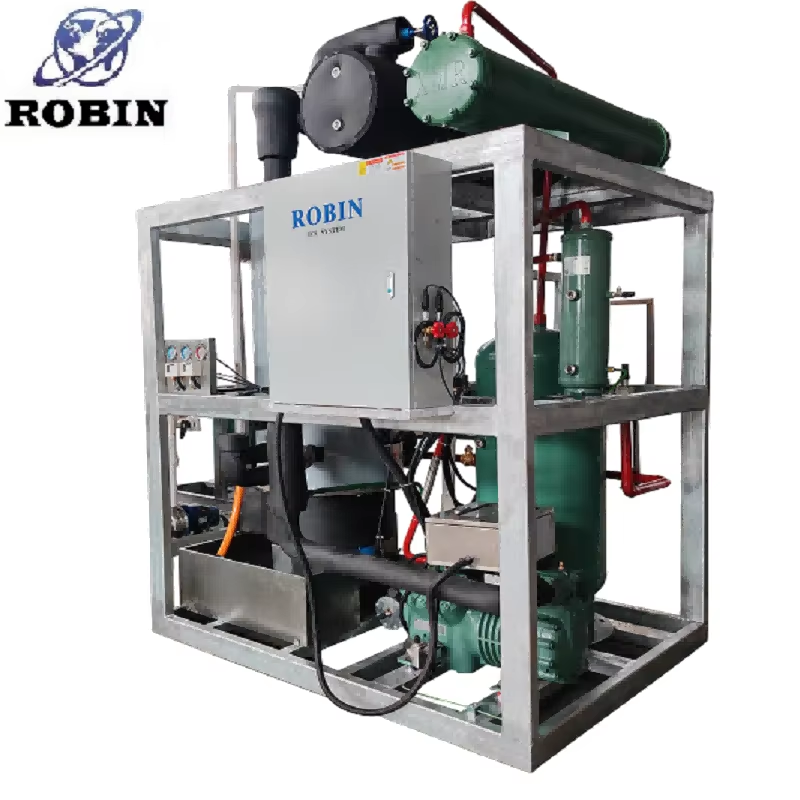
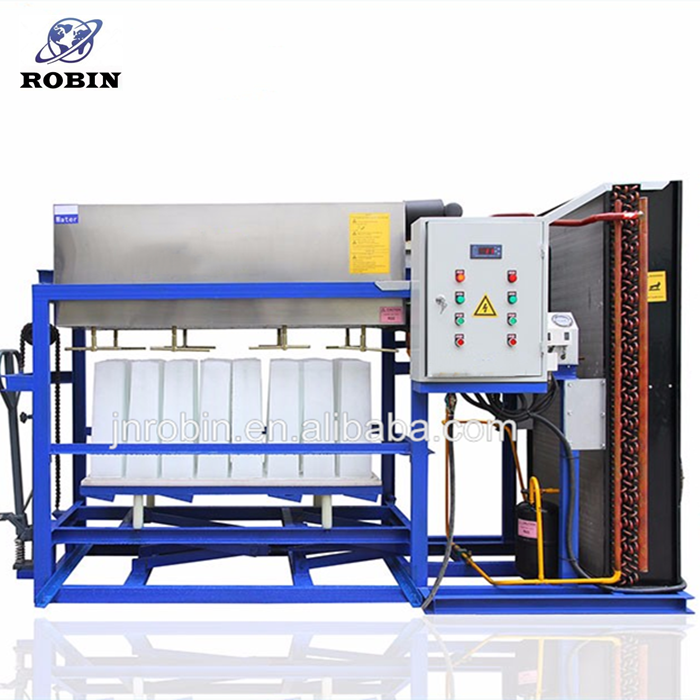
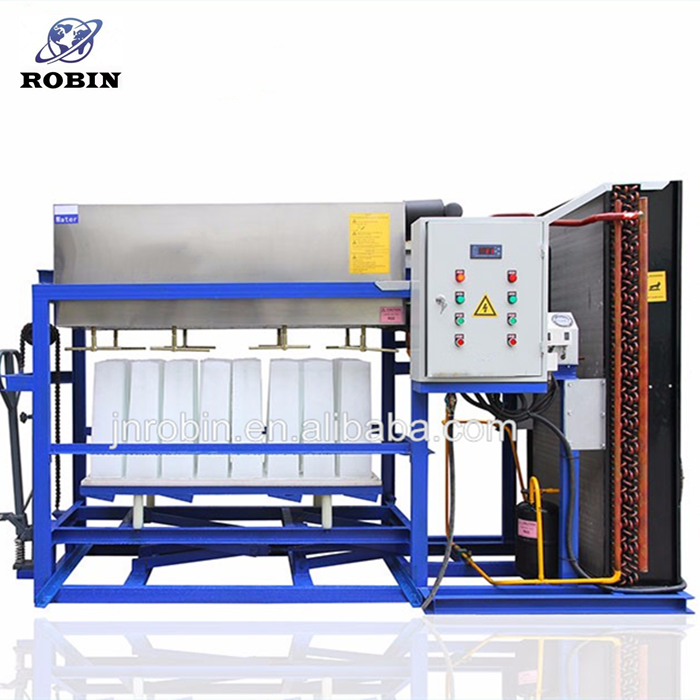
A direct cooling block ice machine supplier provides specialized industrial refrigeration equipment designed to produce large-scale block ice through advanced direct cooling technology. These suppliers offer comprehensive solutions for businesses requiring consistent, high-quality ice production in substantial quantities. The primary function of equipment from a direct cooling block ice machine supplier centers on creating dense, crystal-clear ice blocks that range from 25kg to 100kg per block, suitable for various commercial and industrial applications. The technological foundation relies on direct refrigerant contact with water-filled containers, eliminating intermediate heat transfer steps and maximizing thermal efficiency. This direct cooling method ensures faster freezing cycles compared to traditional brine systems, reducing production time by up to 40 percent while maintaining superior ice quality. Modern suppliers integrate intelligent control systems that monitor temperature fluctuations, refrigerant flow, and harvest cycles automatically, minimizing manual intervention and operational errors. The equipment typically features stainless steel construction for durability and hygiene compliance, meeting international food safety standards. Applications span multiple industries including fisheries preservation, concrete cooling in construction projects, food processing facilities, chemical cooling processes, and large-scale event management. A reputable direct cooling block ice machine supplier also provides installation guidance, maintenance protocols, and technical support to ensure optimal performance throughout the equipment's operational lifespan. The machines accommodate various production capacities, from small-scale operations producing 1 ton daily to industrial facilities generating 50 tons or more within 24 hours. Energy efficiency remains a critical consideration, with leading suppliers incorporating eco-friendly refrigerants and heat recovery systems that reduce operational costs significantly. The modular design approach allows businesses to scale production capacity incrementally, adding units as demand increases without requiring complete system overhauls. Quality assurance from a professional direct cooling block ice machine supplier includes rigorous testing protocols, warranty coverage, and spare parts availability to minimize downtime and maintain continuous production capabilities for demanding commercial environments.

Popular Products

Choosing a reliable direct cooling block ice machine supplier delivers multiple practical benefits that directly impact your operational efficiency and bottom line. First, the direct cooling technology eliminates the need for brine solutions, which means you avoid the corrosive effects and maintenance headaches associated with salt-based systems. Your equipment lasts longer because there is no salt damage to metal components, and you save money on brine replacement and disposal costs. The ice quality produced through direct cooling methods is noticeably superior, with crystal-clear blocks that melt slower and contain fewer impurities compared to brine-frozen alternatives. This matters when you are preserving seafood or using ice for food applications where contamination risks must remain minimal. Energy consumption drops significantly because the refrigerant works directly on the water containers without losing thermal efficiency through intermediate transfer mediums. Many businesses report 25 to 35 percent reductions in electricity costs after switching from brine systems to direct cooling equipment. Production speed increases substantially, allowing you to meet higher demand without expanding your facility footprint. A typical freezing cycle completes in 16 to 24 hours depending on block size and ambient conditions, compared to 36 to 48 hours with older technologies. The automated control systems provided by professional suppliers reduce labor requirements dramatically. Your staff no longer needs to monitor temperatures constantly or manually initiate harvest cycles, freeing them for other productive tasks. Installation flexibility represents another major advantage, as direct cooling systems require less complex infrastructure than brine-based alternatives. You avoid the expense and space requirements of large brine tanks and circulation pumps. Maintenance becomes straightforward with fewer components prone to failure and easier access to critical parts. When issues do arise, a quality direct cooling block ice machine supplier provides rapid technical support and readily available replacement components, minimizing production interruptions. The environmental benefits cannot be overlooked either, as modern systems use refrigerants with lower global warming potential and generate no brine waste requiring special disposal procedures. Scalability allows your business to grow incrementally, adding production modules as demand increases without replacing your entire system. The return on investment typically occurs within 18 to 30 months through combined savings on energy, maintenance, and labor costs. Hygiene standards improve automatically because the closed-system design prevents external contamination and simplifies cleaning procedures. Your ice meets stringent food safety regulations without additional processing steps. Finally, the consistent quality and reliable output from equipment supplied by established manufacturers protect your reputation with customers who depend on your ice supply for their own operations.

Practical Tips

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

01

May

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

In food processing and manufacturing environments, maintaining a reliable and uninterrupted supply of ice is not a luxury — it is an operational necessity. From chilling fresh produce to controlling temperatures during meat processing, the dema...
View More
Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

08

May

Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

When industrial buyers and plant managers evaluate large-scale ice production systems, one question consistently surfaces: is a tube ice maker machine genuinely capable of meeting high-capacity manufacturing demands? The answer is not simply yes or n...
View More
Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

18

May

Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

When it comes to preserving freshness and extending the shelf life of seafood products, the choice of ice type and ice-making equipment is far from trivial. Commercial seafood markets operate under strict hygiene standards, high-volume throughput dem...
View More
How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

20

May

How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

Aquaculture operations depend on precise temperature control at every stage of the supply chain, from harvest tanks to processing floors to distribution centers. A flake ice machine for fish sits at the center of this cold chain, producing thin, flat...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

direct cooling block ice machine supplier

Advanced Direct Refrigeration Technology Maximizes Production Efficiency

Advanced Direct Refrigeration Technology Maximizes Production Efficiency

The core technological advantage offered by a direct cooling block ice machine supplier lies in the revolutionary direct refrigeration approach that fundamentally transforms ice production economics. Unlike conventional brine-based systems where refrigerant cools a salt solution that then freezes water indirectly, direct cooling technology brings refrigerant into immediate thermal contact with the ice-forming containers. This elimination of the intermediate heat transfer step creates a dramatic improvement in thermodynamic efficiency, reducing the temperature differential required for freezing and accelerating the entire production cycle. The engineering behind this system involves precision-designed evaporator coils that wrap around or integrate directly with the ice molds, creating optimal surface contact for maximum heat extraction. This configuration allows the refrigerant to absorb thermal energy from the water at peak efficiency, translating to faster freezing times and lower energy consumption per kilogram of ice produced. A professional direct cooling block ice machine supplier designs these systems with computational fluid dynamics modeling to ensure uniform cooling across all mold positions, preventing the quality variations that plague less sophisticated equipment. The result is consistent block density and clarity regardless of position within the freezing chamber. Temperature control precision reaches levels impossible with brine systems, as modern digital controllers monitor and adjust refrigerant flow in real-time based on actual thermal conditions rather than relying on indirect measurements through brine temperature. This responsiveness prevents the temperature overshoots and undershoots that waste energy and extend production cycles. The direct cooling method also enables rapid defrosting when harvest time arrives, as the same refrigerant lines can introduce warm gas to release blocks quickly without damaging ice quality or equipment components. Maintenance requirements decrease substantially because the system contains fewer moving parts and eliminates the pumps, filters, and monitoring equipment necessary for brine circulation. Corrosion concerns disappear entirely, as there is no salt exposure to attack metal surfaces, extending equipment lifespan from typical 8-10 year expectations to 15-20 years with proper care. Energy audits consistently demonstrate 30 to 40 percent reductions in kilowatt-hours per ton of ice when facilities upgrade from brine to direct cooling systems supplied by reputable manufacturers. This efficiency gain compounds over years of operation, creating substantial cost savings that improve competitive positioning in price-sensitive markets.
Customizable Production Capacity Scales With Business Growth

Customizable Production Capacity Scales With Business Growth

A forward-thinking direct cooling block ice machine supplier understands that businesses evolve and ice production requirements change over time, which is why leading manufacturers design their equipment with modular scalability as a fundamental principle. This approach allows you to start with a production capacity matching your current demand and expand incrementally as your business grows, avoiding the financial burden of over-investing in excessive capacity upfront or the operational limitations of being locked into inadequate production levels. The modular architecture typically consists of independent freezing units that share common refrigeration infrastructure, electrical systems, and control panels, enabling seamless integration of additional capacity without disrupting existing operations. When you need to increase output, a qualified direct cooling block ice machine supplier can add freezing modules to your existing system in a matter of days rather than the weeks or months required for complete system replacements. This flexibility proves invaluable for businesses experiencing seasonal demand fluctuations, as you can optimize your capital deployment by adding temporary capacity during peak periods and scaling back during slower months. The standardized interfaces between modules ensure compatibility across production runs, meaning equipment purchased years apart integrates smoothly without compatibility issues or performance compromises. Control system sophistication from professional suppliers enables centralized management of multiple modules through a single interface, providing real-time visibility into production status, energy consumption, and maintenance requirements across your entire ice production operation. This centralized monitoring capability allows you to optimize production scheduling, balance loads across modules to extend equipment lifespan, and identify efficiency opportunities that reduce operational costs. The financial advantages of scalable systems extend beyond initial capital savings to include reduced financing costs, as you can fund expansion through operational cash flow rather than large upfront loans. Insurance and property tax implications also favor modular approaches, as incremental additions typically avoid the reassessment triggers associated with major facility expansions. A reputable direct cooling block ice machine supplier provides detailed capacity planning assistance, helping you forecast future requirements based on market trends, historical growth patterns, and business development plans. This consultative approach ensures your expansion investments align with actual demand rather than speculative projections, protecting your return on investment. The technical specifications from quality suppliers include clear documentation of maximum scalability limits, electrical and refrigeration infrastructure requirements for various capacity levels, and space planning guidelines that prevent costly mistakes during facility design. Businesses serving multiple markets particularly benefit from scalable systems, as they can adjust production mix between different block sizes and ice types without replacing equipment, simply by reconfiguring mold arrangements within their existing modules supplied by flexible manufacturers.
Comprehensive Support Services Ensure Continuous Operational Reliability

Comprehensive Support Services Ensure Continuous Operational Reliability

The relationship with a professional direct cooling block ice machine supplier extends far beyond the initial equipment purchase, encompassing a complete ecosystem of support services that protect your investment and ensure uninterrupted production capability throughout the equipment's operational life. Leading suppliers recognize that ice production often represents a critical component of their customers' business operations, where downtime directly translates to revenue loss and customer dissatisfaction, making reliable support infrastructure essential rather than optional. Comprehensive pre-installation consultation services begin this support relationship, with experienced engineers assessing your facility conditions, electrical capacity, water quality, ambient temperature ranges, and spatial constraints to design an optimal system configuration. This thorough planning prevents the costly mistakes that occur when equipment specifications mismatch operational realities, ensuring your direct cooling block ice machine performs at rated capacity from day one. Professional installation services from qualified technicians guarantee proper refrigerant charging, electrical connections, water supply integration, and control system calibration, establishing the foundation for reliable long-term performance. The initial commissioning process includes operator training that covers daily operations, routine maintenance procedures, troubleshooting basics, and safety protocols, empowering your staff to maximize equipment effectiveness and identify potential issues before they escalate into failures. Ongoing technical support availability through multiple channels including phone, email, video conferencing, and on-site visits provides rapid response when questions or problems arise, minimizing production disruptions. A quality direct cooling block ice machine supplier maintains comprehensive spare parts inventories with expedited shipping capabilities, ensuring critical components reach your facility quickly when replacements become necessary. Preventive maintenance programs offered by leading suppliers include scheduled inspections, refrigerant system analysis, electrical component testing, and wear part replacement before failures occur, dramatically reducing unexpected downtime. These programs typically reduce total maintenance costs by 20 to 30 percent compared to reactive repair approaches while extending equipment lifespan significantly. Remote monitoring capabilities increasingly offered by advanced suppliers enable proactive support, with equipment telemetry transmitted to technical teams who can identify developing issues and schedule interventions during planned downtime rather than emergency situations. Software updates and control system enhancements provided by committed suppliers ensure your equipment benefits from continuous improvement in efficiency algorithms, user interface refinements, and diagnostic capabilities without requiring hardware replacements. Warranty coverage from reputable direct cooling block ice machine suppliers typically extends beyond basic component replacement to include labor costs, travel expenses, and performance guarantees that protect your operational continuity. The documentation provided by professional suppliers includes detailed technical manuals, electrical schematics, refrigeration diagrams, and troubleshooting flowcharts that enable your maintenance team to perform routine service independently while knowing when specialist assistance is required. Long-term parts availability commitments from established suppliers protect against obsolescence concerns, ensuring you can maintain equipment economically for its full design life rather than facing premature replacement due to unavailable components.


Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000