Food Grade Flake Ice Machine: Commercial Ice Solutions for Food Safety and Efficiency

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade flake ice machine

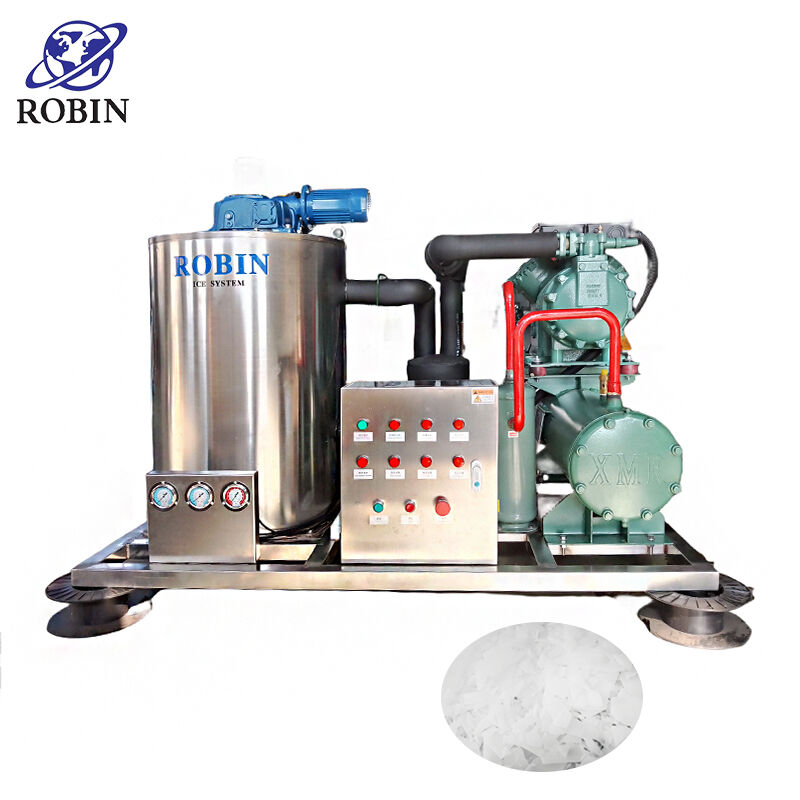
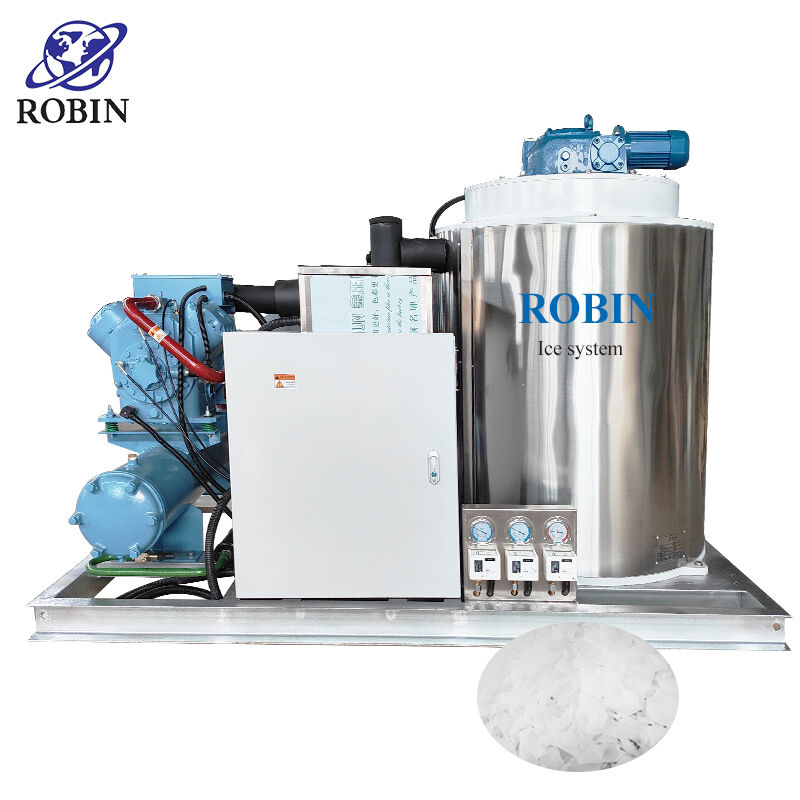
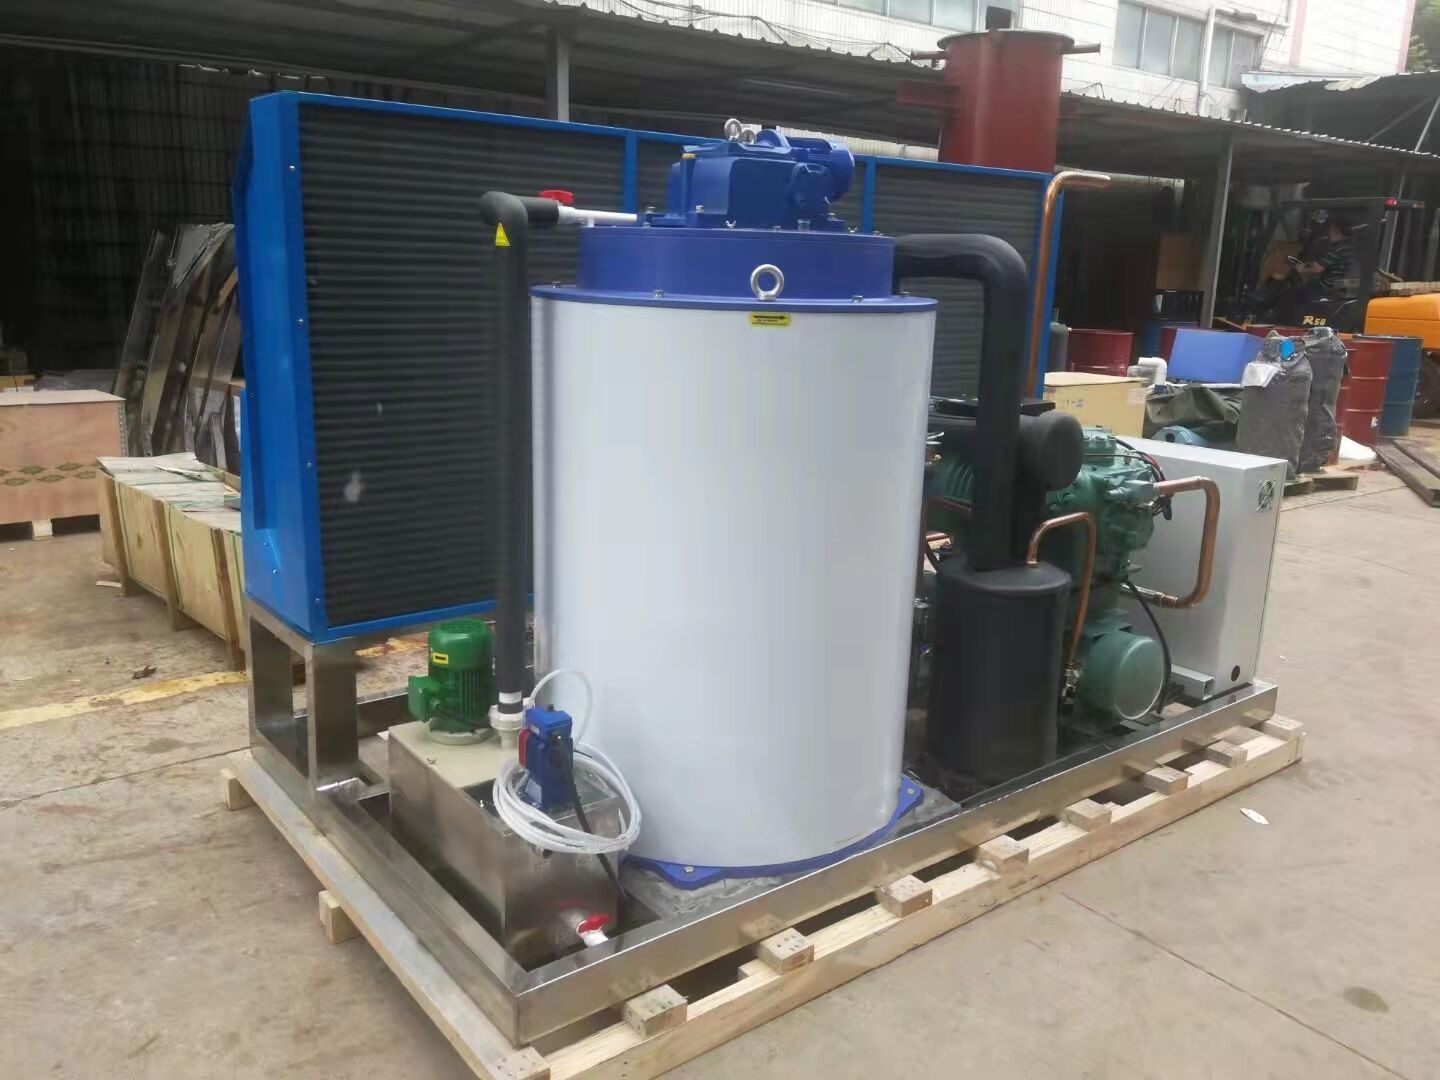
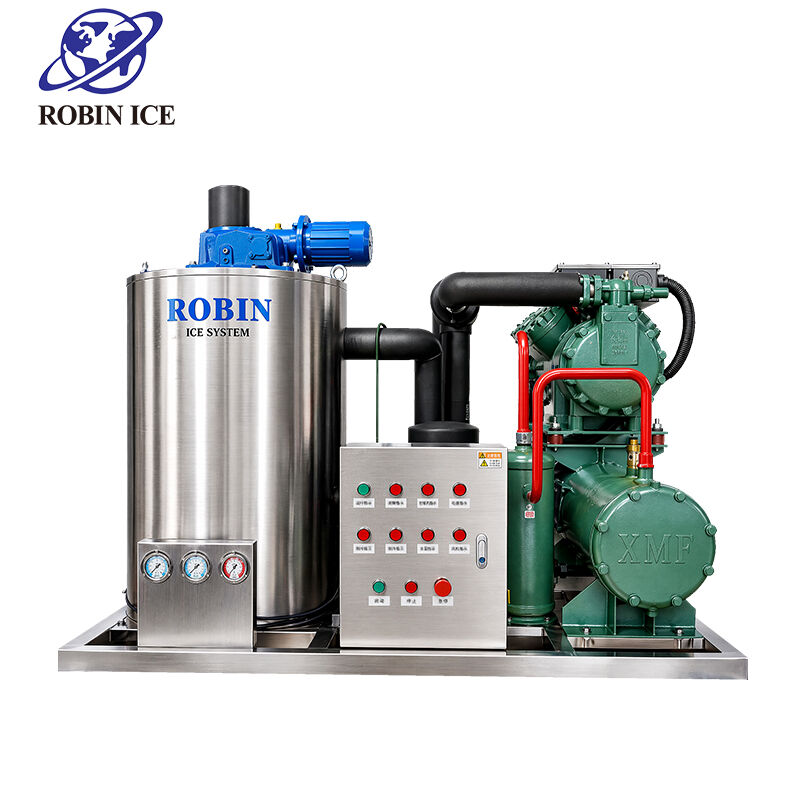
A food grade flake ice machine represents a specialized refrigeration system engineered to produce thin, flat ice crystals that meet stringent food safety standards. This equipment transforms purified water into delicate ice flakes, typically measuring 1-2mm in thickness, through a continuous freezing process on a rotating drum or evaporator surface. The food grade flake ice machine operates by circulating refrigerant through an evaporator cylinder while water flows over its surface, creating a frozen layer that is then scraped off by rotating blades to form irregular flake-shaped ice particles. These machines are constructed using stainless steel and food-safe materials that comply with FDA regulations and international hygiene standards, ensuring that the ice produced remains uncontaminated and suitable for direct contact with consumable products. The primary function of a food grade flake ice machine centers on rapid cooling and preservation of perishable goods, particularly in commercial food processing, seafood markets, bakeries, and healthcare facilities. The technological features include advanced compressor systems that maintain consistent ice production rates, automated water filtration mechanisms that remove impurities, and intelligent control panels that monitor temperature, production cycles, and maintenance requirements. Modern food grade flake ice machine models incorporate energy-efficient components that reduce operational costs while maximizing output capacity, with production ranges varying from 100 kilograms to several tons per day depending on commercial needs. The applications extend across multiple industries where temperature control is critical: supermarkets use these machines to display fresh fish and meat products, hospitals rely on them for therapeutic cooling and laboratory specimen preservation, while food processing plants depend on them for mixing, cooling, and transporting temperature-sensitive ingredients. The versatility of a food grade flake ice machine makes it indispensable for businesses that require consistent, hygienic ice supply throughout their operations, providing a reliable solution that maintains product quality and extends shelf life.

New Products

The food grade flake ice machine delivers exceptional cooling efficiency that surpasses traditional ice cube systems, primarily because flake ice possesses a larger surface area that enables faster heat transfer and more uniform temperature distribution across products. This rapid cooling capability proves invaluable for businesses handling perishable goods, as it quickly lowers product temperatures to safe storage levels, minimizing bacterial growth and preserving freshness. The soft, moldable texture of flake ice allows it to conform to irregular shapes, creating intimate contact with products like seafood, poultry, and produce, which ensures comprehensive cooling without causing physical damage to delicate items. Unlike hard ice cubes that can bruise fruits or puncture packaging, the gentle nature of flake ice protects product integrity while maintaining optimal preservation conditions. Businesses benefit from reduced product loss and waste, translating directly into improved profit margins and customer satisfaction. The food grade flake ice machine operates with remarkable consistency, producing ice at predictable rates that allow managers to plan inventory and staffing requirements accurately, eliminating the uncertainty associated with unreliable ice supply. Energy consumption represents a significant operational expense for commercial refrigeration, and modern food grade flake ice machine models address this concern through advanced compressor technology and optimized refrigeration cycles that minimize electricity usage while maintaining high production volumes. The automated operation reduces labor requirements, as these machines function independently once programmed, freeing staff to focus on core business activities rather than manual ice production tasks. Maintenance demands remain minimal due to robust construction and self-cleaning features that prevent scale buildup and bacterial contamination, resulting in lower long-term ownership costs and extended equipment lifespan. The hygienic design of a food grade flake ice machine incorporates smooth, seamless surfaces that resist bacterial colonization and facilitate thorough cleaning, ensuring compliance with health department regulations and food safety certifications. Water efficiency stands as another practical advantage, as these machines utilize precise water management systems that eliminate waste and reduce utility expenses compared to older ice-making technologies. The compact footprint of many food grade flake ice machine models allows installation in space-constrained environments, maximizing valuable floor space for revenue-generating activities. Businesses appreciate the scalability these machines offer, with models available in various capacities that can grow alongside expanding operations, providing a future-proof investment that adapts to changing demands. The reliability of a food grade flake ice machine minimizes downtime and service interruptions, which is critical for operations where ice availability directly impacts product quality and customer service. The versatility extends beyond simple cooling applications, as flake ice serves multiple purposes including product display, transportation, processing, and even therapeutic uses in medical settings, making it a multifunctional asset that delivers value across diverse operational needs.

Tips And Tricks

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

18

May

Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

When it comes to preserving freshness and extending the shelf life of seafood products, the choice of ice type and ice-making equipment is far from trivial. Commercial seafood markets operate under strict hygiene standards, high-volume throughput dem...
View More
How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

20

May

How Does Flake Ice Machine for Fish Support Aquaculture Cold Storage Needs?

Aquaculture operations depend on precise temperature control at every stage of the supply chain, from harvest tanks to processing floors to distribution centers. A flake ice machine for fish sits at the center of this cold chain, producing thin, flat...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade flake ice machine

Superior Cooling Performance Through Maximum Surface Contact

Superior Cooling Performance Through Maximum Surface Contact

The food grade flake ice machine produces ice with a uniquely thin and irregular structure that maximizes surface area exposure, creating an unparalleled cooling medium for commercial applications. This distinctive characteristic stems from the manufacturing process where water freezes in ultra-thin layers before being scraped into delicate flakes, resulting in ice particles that measure approximately 1-2 millimeters in thickness with irregular edges and shapes. The increased surface area translates into dramatically faster heat exchange rates compared to conventional ice cubes or blocks, allowing businesses to reduce cooling times by up to 50 percent in many applications. When flake ice comes into contact with warm products, the extensive surface area facilitates rapid thermal transfer, drawing heat away from perishable items at an accelerated pace that helps maintain food safety standards and product quality. This performance advantage becomes particularly evident in high-volume operations such as fish markets, where freshly caught seafood must be cooled immediately to prevent spoilage and preserve texture, flavor, and nutritional value. The food grade flake ice machine enables these businesses to meet strict temperature requirements efficiently, ensuring that products remain within safe temperature zones throughout storage and display periods. The moldable nature of flake ice allows it to fill gaps and conform to irregular product shapes, creating comprehensive coverage that eliminates hot spots and ensures uniform cooling across entire batches. This conformability proves essential when cooling delicate items like berries, leafy greens, or bakery products that require gentle handling to prevent physical damage. Traditional ice cubes leave air gaps that reduce cooling efficiency and create uneven temperature distribution, whereas flake ice nestles around products to form an insulating barrier that maintains consistent temperatures. The food grade flake ice machine thus provides businesses with a competitive advantage by enabling superior product presentation, extended shelf life, and reduced spoilage rates that directly impact profitability. The rapid cooling capability also supports food processing operations where ingredients must be chilled quickly during mixing or grinding processes to prevent bacterial growth and maintain product consistency. Bakeries use flake ice to control dough temperatures during high-speed mixing, preventing gluten development issues that would compromise texture and rise. The food grade flake ice machine delivers precise temperature control that allows processors to achieve consistent results batch after batch, reducing waste and improving product quality.
Uncompromising Hygiene Standards and Food Safety Compliance

Uncompromising Hygiene Standards and Food Safety Compliance

The food grade flake ice machine is engineered with meticulous attention to sanitation requirements, incorporating design elements and material selections that prioritize food safety and regulatory compliance. Every component that contacts water or ice is constructed from food-grade stainless steel or approved polymers that resist corrosion, prevent chemical leaching, and withstand repeated cleaning with commercial sanitizers. The smooth, seamless construction eliminates crevices and joints where bacteria, mold, or mineral deposits could accumulate, creating surfaces that are easily cleaned and sanitized according to health department protocols. This hygienic design philosophy extends throughout the entire ice production pathway, from water intake through filtration, freezing, and discharge, ensuring that contamination risks are minimized at every stage. The food grade flake ice machine typically includes integrated water filtration systems that remove sediment, chlorine, and microorganisms before water enters the freezing chamber, producing ice that meets or exceeds drinking water quality standards. Many models feature antimicrobial coatings on critical surfaces that actively inhibit bacterial growth between cleaning cycles, providing an additional layer of protection against contamination. The automated cleaning cycles programmed into modern food grade flake ice machine systems flush the water circuit and evaporator surfaces regularly, preventing scale buildup that could harbor pathogens or affect ice quality. Businesses operating in regulated industries such as food processing, healthcare, and hospitality face stringent inspection requirements and must demonstrate compliance with food safety management systems like HACCP. The food grade flake ice machine simplifies compliance by providing documentation, certifications, and design features that align with regulatory expectations, reducing the administrative burden on operators. The transparent operation of these machines allows quality assurance personnel to monitor ice production conditions, verify cleaning procedures, and maintain detailed records that satisfy auditor requirements. The food grade flake ice machine eliminates cross-contamination risks associated with manual ice handling, as the automated production and dispensing process minimizes human contact with the finished product. This closed-system approach protects ice purity from environmental contaminants, employee hygiene lapses, and equipment contamination that could compromise food safety. The importance of hygienic ice production cannot be overstated, as contaminated ice has been identified as a vector for foodborne illness outbreaks in restaurants, hospitals, and food processing facilities. Investing in a food grade flake ice machine demonstrates a commitment to customer safety and brand protection, as businesses that prioritize hygiene build trust with consumers and avoid costly recalls or reputation damage. The long-term value extends beyond regulatory compliance to encompass operational efficiency, as properly maintained food grade flake ice machine equipment experiences fewer breakdowns, produces consistent quality ice, and requires less frequent deep cleaning interventions.
Economic Efficiency Through Energy Optimization and Operational Reliability

Economic Efficiency Through Energy Optimization and Operational Reliability

The food grade flake ice machine represents a sound financial investment that delivers measurable returns through reduced energy consumption, minimized maintenance costs, and exceptional operational reliability. Modern refrigeration technology incorporated into these machines utilizes variable-speed compressors, high-efficiency heat exchangers, and intelligent control systems that optimize energy usage based on actual ice demand rather than running continuously at maximum capacity. This adaptive operation can reduce electricity consumption by 20-30 percent compared to older fixed-speed models, translating into substantial utility cost savings over the equipment's lifespan. The food grade flake ice machine achieves superior energy efficiency by maximizing the coefficient of performance in the refrigeration cycle, extracting more cooling capacity from each unit of electrical input through precise temperature control and optimized refrigerant flow. Businesses operating multiple shifts or requiring continuous ice production benefit particularly from these efficiency gains, as the cumulative energy savings compound over thousands of operating hours annually. The robust construction and quality components used in food grade flake ice machine manufacturing result in extended service life and reduced maintenance frequency, lowering total cost of ownership compared to cheaper alternatives that require frequent repairs or premature replacement. Stainless steel evaporators resist corrosion and wear, maintaining consistent performance for years without degradation, while commercial-grade compressors are engineered for continuous duty cycles that would overwhelm residential-grade equipment. The food grade flake ice machine typically includes diagnostic systems that monitor operating parameters and alert operators to potential issues before they escalate into costly failures, enabling proactive maintenance that prevents unexpected downtime. This predictive capability proves invaluable for businesses where ice availability is mission-critical, such as seafood processors who cannot afford production interruptions during peak harvest seasons. The modular design of many food grade flake ice machine models facilitates rapid component replacement, minimizing repair time and allowing businesses to maintain spare parts inventory for critical components. The operational reliability extends to consistent ice quality, as precision temperature control and automated water management ensure that every batch meets the same specifications regardless of ambient conditions or production volume. This consistency eliminates quality variations that could affect product cooling performance or customer satisfaction, providing businesses with predictable results they can depend on. The food grade flake ice machine also contributes to water conservation through efficient water usage and recirculation systems that minimize waste, addressing both environmental responsibility and utility cost management. The return on investment calculation for a food grade flake ice machine must consider not only direct cost savings but also indirect benefits such as reduced product loss, improved product quality, enhanced customer satisfaction, and competitive advantages gained through superior cooling capabilities. Businesses that invest in quality equipment position themselves for long-term success by building operational foundations that support growth, maintain compliance, and deliver consistent performance that customers and regulators expect.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000