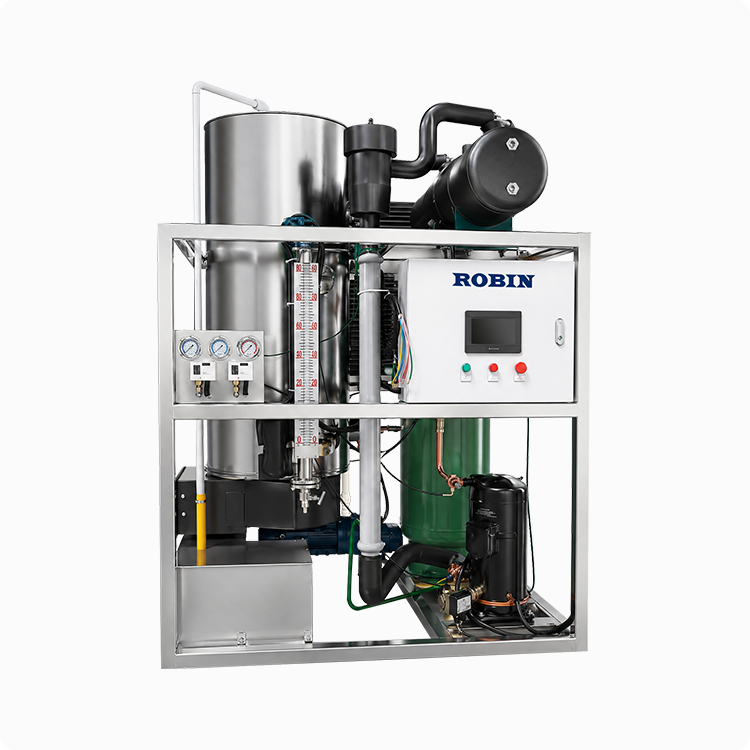
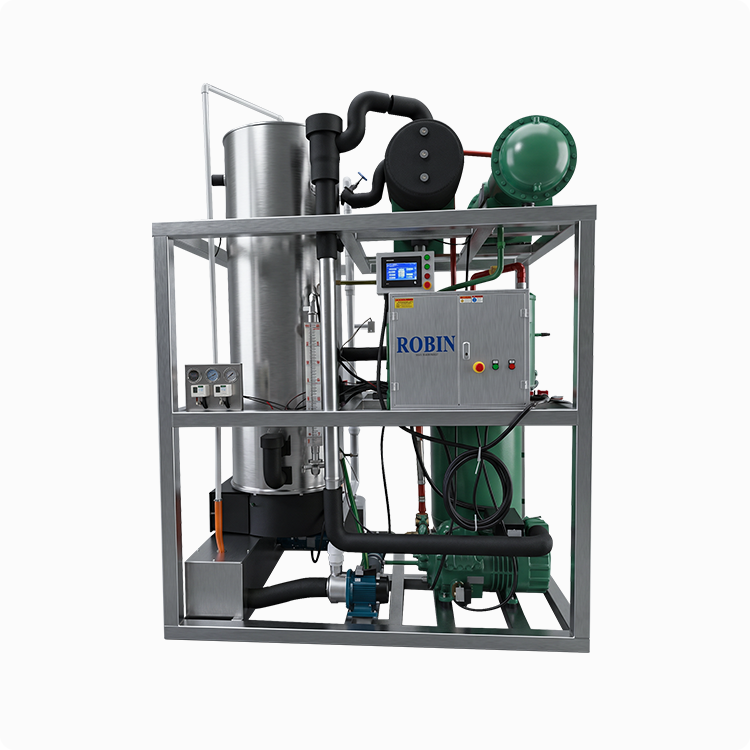
Commercial Flake Ice Machine for Supermarket - Fresh Food Display Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

flake ice machine for supermarket

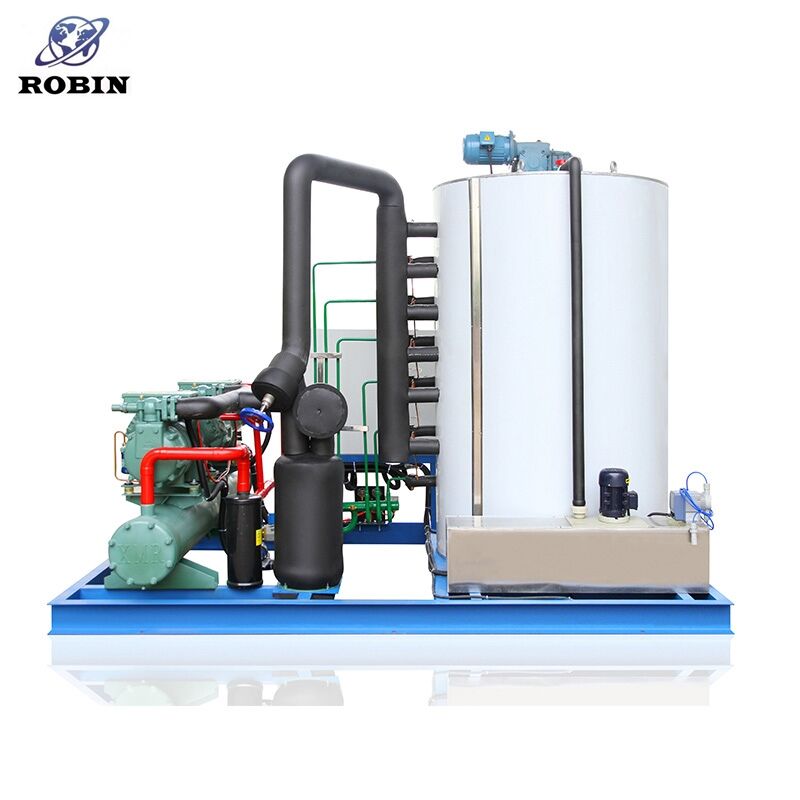
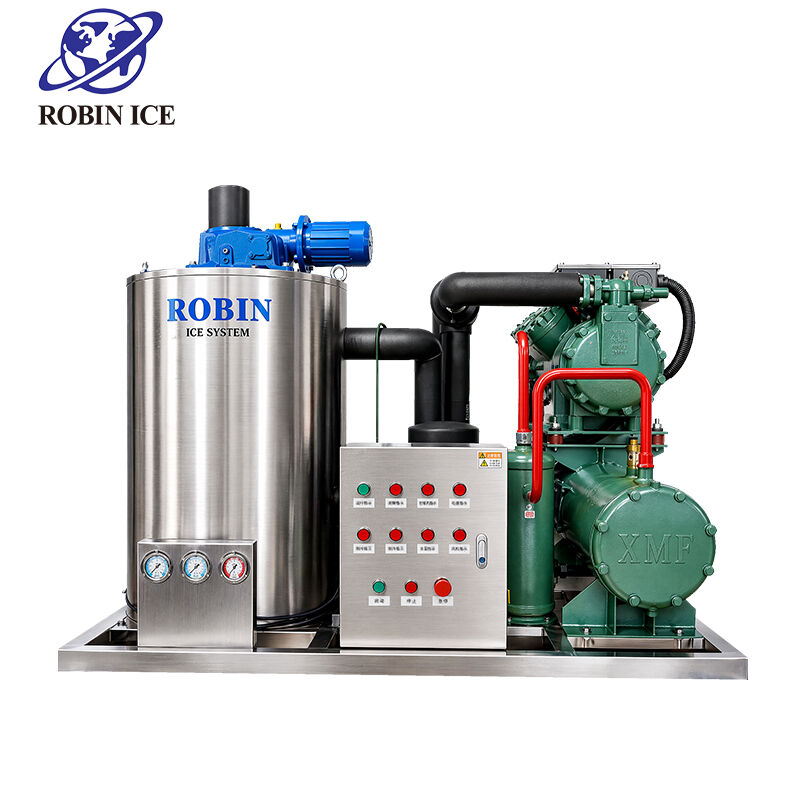
A flake ice machine for supermarket represents an essential refrigeration solution designed specifically to meet the demanding preservation needs of fresh food retail environments. This specialized equipment produces thin, flat ice crystals that provide superior cooling coverage compared to traditional ice forms. The machine operates through an advanced evaporator drum system where water freezes on a rotating cylinder and is continuously scraped off by precision blades, creating delicate ice flakes with optimal surface area. Modern flake ice machines for supermarket applications integrate energy-efficient compressors, automated control systems, and food-grade stainless steel construction to ensure hygiene standards. The technology behind these units allows for consistent ice production ranging from several hundred to thousands of pounds per day, depending on the model capacity. Supermarkets rely on flake ice machines to maintain product freshness across multiple departments including seafood counters, meat displays, produce sections, and deli areas. The ice produced has a temperature typically between 23 to 28 degrees Fahrenheit, making it ideal for direct contact with perishable goods without causing freezer burn. These machines feature user-friendly digital interfaces that allow staff to monitor production rates, adjust settings, and receive maintenance alerts. The compact footprint of contemporary flake ice machine for supermarket models enables installation in space-constrained back-of-house areas while maintaining high output capacity. Built-in water filtration systems ensure ice purity, while antimicrobial components prevent bacterial growth within the machine. The rapid cooling properties of flake ice help supermarkets reduce product spoilage, extend shelf life, and maintain the visual appeal of fresh merchandise. Investment in a quality flake ice machine for supermarket operations delivers long-term cost savings through reduced waste and improved customer satisfaction with product quality.

New Product Recommendations

Supermarkets gain significant operational benefits when implementing a flake ice machine for supermarket displays and storage applications. The primary advantage lies in superior temperature control that keeps seafood, meat, poultry, and produce at optimal freshness levels throughout the day. Unlike cube or nugget ice, flake ice conforms perfectly to irregular product shapes, creating maximum surface contact that accelerates cooling and maintains consistent temperatures. This conformability means every piece of fish, every cut of meat, and every vegetable receives uniform refrigeration without air gaps that allow warm spots to develop. The soft texture of flake ice prevents damage to delicate items like berries, leafy greens, and premium seafood fillets that harder ice forms might bruise or puncture. Customers notice the difference immediately when products rest on beds of pristine flake ice, as the presentation signals freshness and quality that influences purchasing decisions. A flake ice machine for supermarket use operates with remarkable energy efficiency, utilizing modern refrigeration technology that minimizes electricity consumption while maximizing output. The automated production cycle means staff never worry about running out of ice during peak shopping hours, and the continuous supply eliminates the need for manual ice handling or emergency purchases from external suppliers. Maintenance requirements remain minimal thanks to self-cleaning features and durable components engineered for commercial environments. The financial return becomes evident through reduced shrinkage rates, as proper icing extends product life by days, directly impacting profit margins on high-value perishables. Food safety compliance becomes easier to achieve and document when a reliable flake ice machine for supermarket operations provides consistent cooling that meets health department standards. The ice itself contains no additives or chemicals, making it safe for direct food contact and suitable for use in prepared food areas. Installation flexibility allows supermarkets to position machines near high-demand areas, reducing the labor and time required to transport ice throughout the store. Modern units operate quietly, ensuring the shopping environment remains pleasant without disruptive compressor noise. The professional appearance of a well-maintained flake ice display elevates the entire store image, positioning the supermarket as a destination for quality fresh foods. Staff productivity increases because automated ice production frees employees from time-consuming manual ice preparation tasks, allowing them to focus on customer service and merchandising. The scalability of flake ice machine for supermarket systems means businesses can start with one unit and expand capacity as sales grow, protecting the initial investment while accommodating future needs. Water efficiency features in contemporary models reduce utility costs and support sustainability initiatives that resonate with environmentally conscious consumers. The reliability of commercial-grade flake ice machines minimizes downtime, ensuring continuous operation during critical periods like holidays and weekends when fresh food sales peak.

Latest News

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

01

May

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

In food processing and manufacturing environments, maintaining a reliable and uninterrupted supply of ice is not a luxury — it is an operational necessity. From chilling fresh produce to controlling temperatures during meat processing, the dema...
View More
Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

06

May

How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

The ice tube machine has become an essential piece of equipment across a wide range of commercial operations, from busy restaurant kitchens to large-scale food processing facilities. Its ability to produce cylindrical ice in consistent shapes and siz...
View More
How Is Flake Ice Machine for Fish Used in Seafood Processing Facilities?

26

May

How Is Flake Ice Machine for Fish Used in Seafood Processing Facilities?

In seafood processing facilities, temperature control is not a preference — it is a biological necessity. From the moment a fish is harvested to the point it reaches a consumer's plate, maintaining a consistently low temperature determines whet...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

flake ice machine for supermarket

Advanced Evaporator Technology Delivers Consistent Ice Quality

Advanced Evaporator Technology Delivers Consistent Ice Quality

The heart of every flake ice machine for supermarket applications is its sophisticated evaporator drum technology that sets it apart from conventional ice-making equipment. This cylindrical evaporator operates on a continuous freeze-and-harvest cycle that produces ice flakes with remarkable consistency in size, texture, and temperature. Water flows onto the interior surface of a refrigerated drum where it instantly begins freezing into a thin layer. As the drum rotates, precision-engineered scraper blades positioned at optimal angles shave the frozen layer into delicate flakes that fall into a storage bin below. The engineering behind this process ensures each flake maintains ideal thickness, typically between 1 to 2 millimeters, which provides the perfect balance between cooling efficiency and ice longevity. This thickness allows the flakes to pack tightly around products while remaining pliable enough to conform to any shape. The evaporator drum in a quality flake ice machine for supermarket use is constructed from food-grade stainless steel with specialized coatings that prevent ice adhesion and facilitate smooth release. The refrigeration system maintains precise temperature control throughout the drum surface, eliminating hot spots that could create inconsistent ice quality. Advanced models incorporate variable-speed compressors that adjust cooling capacity based on ambient temperature and production demand, optimizing energy consumption without compromising output. The scraper blade assembly represents critical engineering, with blades manufactured from hardened materials that resist wear while maintaining sharp edges for clean ice removal. Proper blade geometry ensures complete ice harvest with minimal residue, maximizing production efficiency and preventing buildup that could impair machine performance. The continuous production method means a flake ice machine for supermarket operations never experiences the downtime associated with batch-style ice makers, providing uninterrupted supply during business hours. Automated defrost cycles prevent frost accumulation on evaporator surfaces, maintaining peak efficiency and extending component lifespan. The closed-loop water circulation system in modern units recycles unused water, reducing waste and lowering operating costs. Sensors monitor ice thickness and production rates, automatically adjusting parameters to maintain consistent output regardless of external conditions. This technological sophistication translates directly into operational reliability that supermarket managers depend on for daily fresh food merchandising.
Hygienic Design Meets Food Safety Standards

Hygienic Design Meets Food Safety Standards

Food safety represents the paramount concern for any supermarket, and a flake ice machine for supermarket environments is engineered with comprehensive hygienic features that protect product integrity and customer health. Every component that contacts water or ice is constructed from antimicrobial stainless steel that resists bacterial colonization and withstands rigorous cleaning protocols. The smooth, seamless interior surfaces eliminate crevices where microorganisms might harbor, while rounded corners and accessible panels facilitate thorough sanitation. Modern flake ice machines incorporate built-in water filtration systems that remove sediment, chlorine, and potential contaminants before water enters the freezing cycle. These multi-stage filters ensure the ice produced meets or exceeds drinking water quality standards, making it safe for direct contact with ready-to-eat foods. The filtration system in a quality flake ice machine for supermarket use includes replaceable cartridges with indicator lights that alert staff when maintenance is required, preventing compromised ice quality. Antimicrobial additives in plastic components and gaskets provide additional protection against microbial growth in areas that cannot be stainless steel. The ice storage bin features insulated walls that maintain proper temperature while preventing external condensation that could introduce contamination. Sloped bin floors and strategically positioned drains ensure meltwater evacuates completely, preventing standing water that could become a breeding ground for bacteria. The air intake system includes washable filters that prevent dust and airborne particles from entering the machine, protecting both the mechanical components and ice purity. Many flake ice machines for supermarket applications now include UV sanitization systems that continuously disinfect water and ice contact surfaces, providing an extra layer of protection without chemical additives. The exterior housing is designed for easy cleaning with smooth surfaces and minimal seams, allowing staff to maintain sanitary conditions around the machine. Removable panels provide access to internal components for deep cleaning during scheduled maintenance, ensuring every part of the system remains hygienic. The machine control system can log production data and cleaning cycles, creating documentation that supports health inspection compliance and HACCP protocols. Automatic alerts notify operators of any conditions that might compromise ice safety, such as elevated water temperature or extended production interruptions. The commitment to hygiene extends to the ice dispensing mechanism, which minimizes human contact and prevents contamination during ice transfer to display cases. This comprehensive approach to sanitary design makes a flake ice machine for supermarket use an investment in both product quality and regulatory compliance.
Operational Efficiency Reduces Costs and Labor

Operational Efficiency Reduces Costs and Labor

The economic advantages of installing a flake ice machine for supermarket operations extend far beyond the initial equipment investment, delivering substantial ongoing savings through operational efficiency and labor reduction. These machines operate with exceptional energy efficiency, utilizing advanced compressor technology and optimized refrigeration cycles that minimize electricity consumption per pound of ice produced. Variable-speed compressors adjust cooling capacity to match actual demand, avoiding the energy waste associated with constant full-power operation. Improved insulation in modern units reduces heat transfer, allowing the refrigeration system to maintain ice temperature with less energy input. The continuous production method eliminates the energy spikes associated with batch ice makers that must repeatedly cool down and freeze new batches. A properly sized flake ice machine for supermarket needs can reduce ice-related energy costs by thirty to forty percent compared to older equipment or alternative ice sources. The automated operation eliminates labor costs associated with manual ice production, bagging, and distribution throughout the store. Staff members no longer spend valuable time filling ice bins, monitoring supply levels, or making emergency runs to purchase ice from external suppliers. The machine handles these tasks autonomously, freeing employees to focus on customer service, merchandising, and other revenue-generating activities. The reliability of commercial flake ice machines minimizes maintenance costs through durable construction and self-diagnostic systems that identify potential issues before they cause breakdowns. Preventive maintenance becomes straightforward with accessible components and clear service indicators that guide technicians to specific areas requiring attention. The reduced product spoilage enabled by consistent, high-quality ice directly impacts the bottom line by extending the saleable life of expensive perishables like seafood and premium meats. Supermarkets report shrinkage reductions of fifteen to twenty-five percent in properly iced departments, translating to thousands of dollars in saved inventory annually. The professional presentation created by abundant flake ice increases sales velocity as customers perceive greater freshness and quality, choosing to purchase items they might otherwise skip. A flake ice machine for supermarket use pays for itself through these combined savings, typically achieving return on investment within eighteen to thirty-six months depending on store volume. Water efficiency features reduce utility bills while supporting corporate sustainability goals that appeal to environmentally conscious consumers. The compact footprint of modern machines maximizes valuable floor space, allowing supermarkets to dedicate more area to revenue-generating displays rather than ice production equipment. The quiet operation of contemporary units eliminates noise complaints and creates a more pleasant working environment for staff in back-of-house areas. Long equipment lifespan, often exceeding ten years with proper maintenance, spreads the capital investment across many years of reliable service, improving the overall cost-benefit ratio.


Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000