High Quality Flake Ice Machine - Commercial Ice Production Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high quality flake ice machine

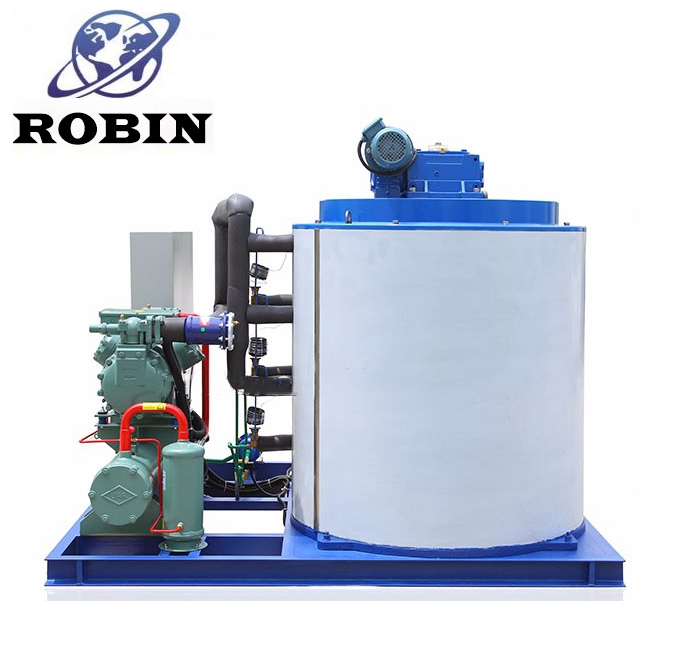
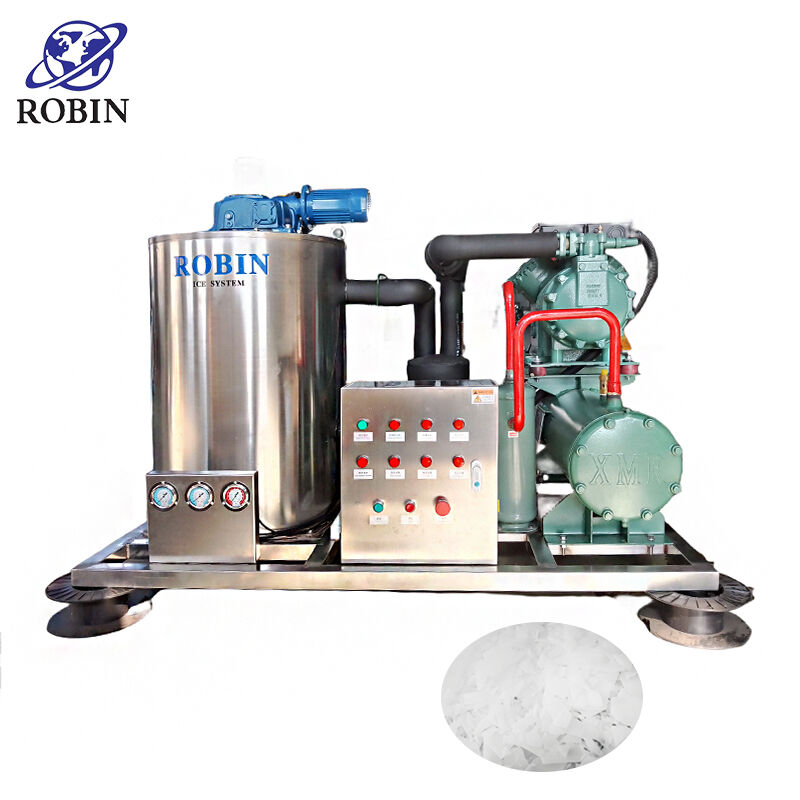
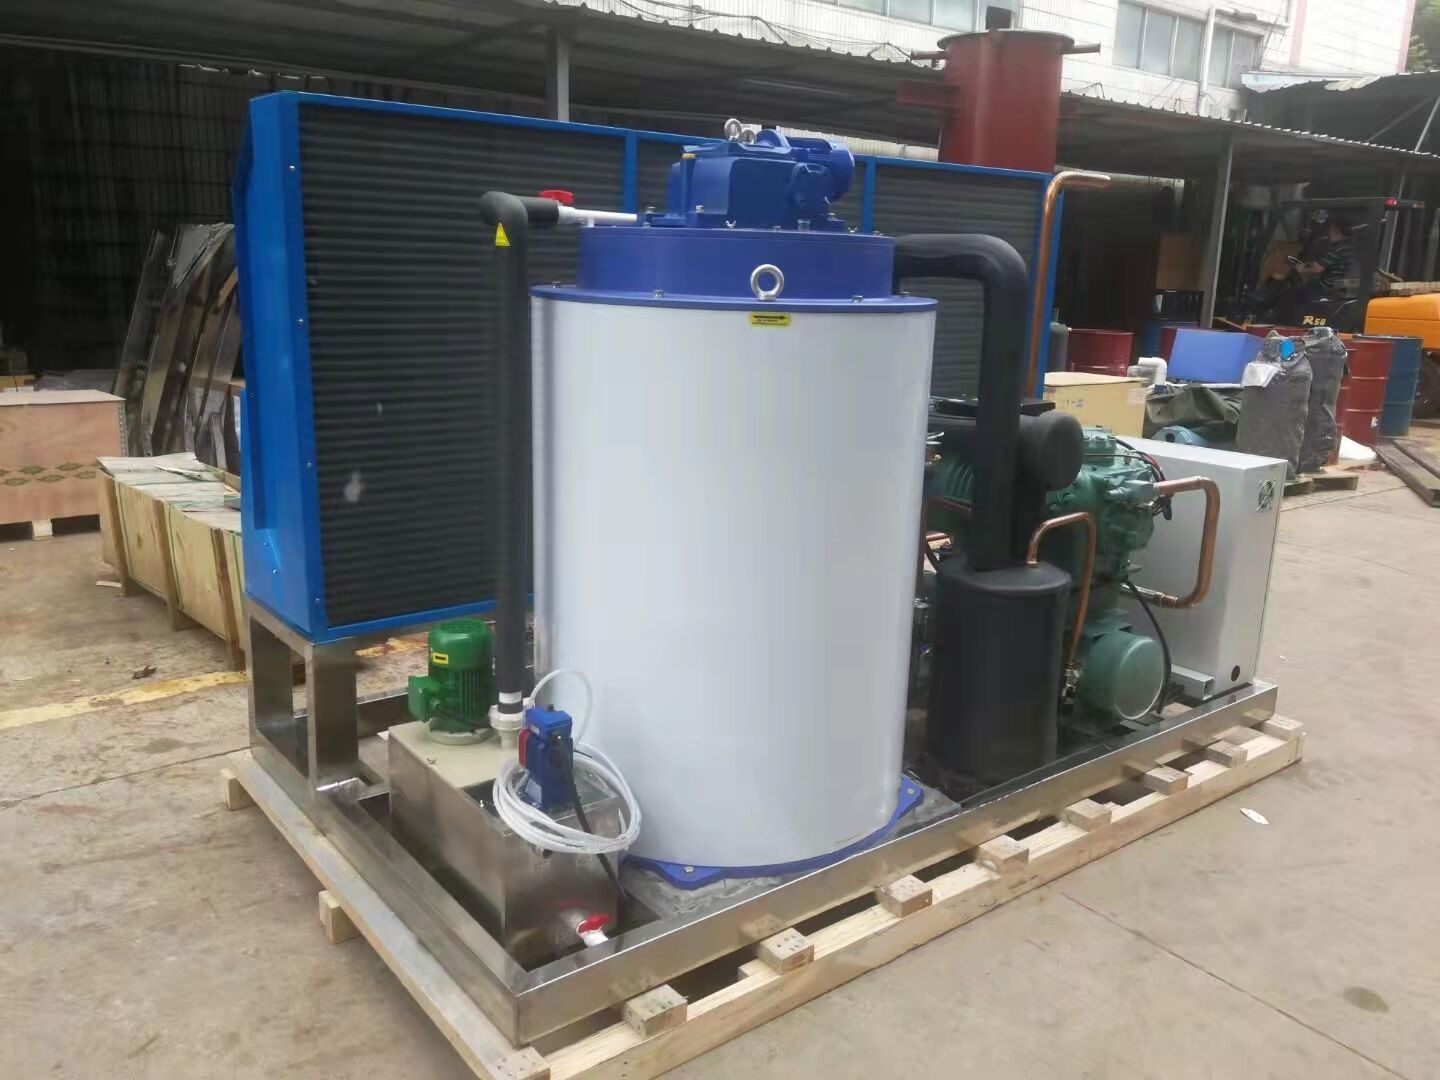
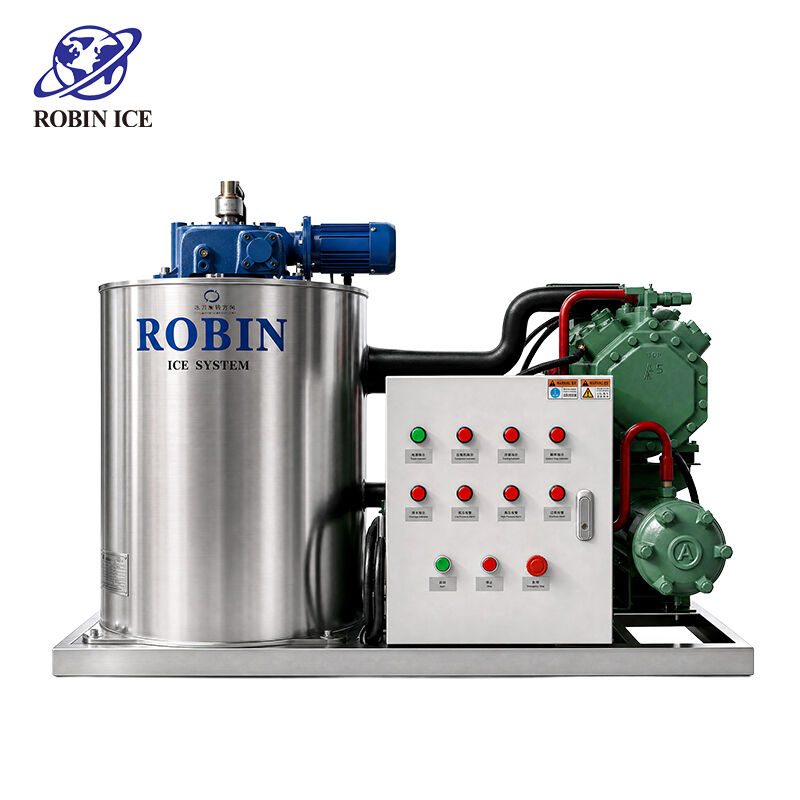
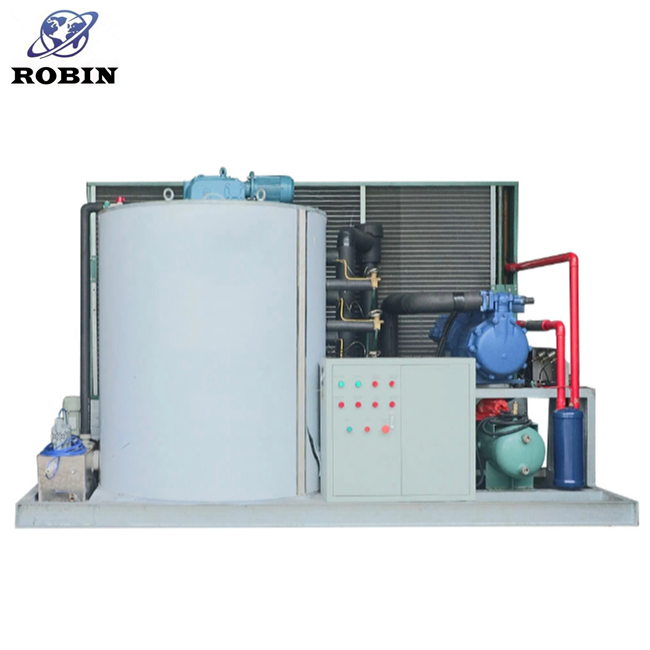
A high quality flake ice machine represents a sophisticated refrigeration solution designed to produce thin, flat ice crystals that offer superior cooling performance across diverse commercial and industrial applications. These advanced systems utilize precision-engineered evaporators and intelligent control mechanisms to generate consistent flake ice with optimal thickness and texture. The fundamental operation involves water flowing over a refrigerated cylindrical drum where it freezes into a thin layer before being scraped off by rotating blades, creating small, irregular flakes that maximize surface area contact. Modern high quality flake ice machine units incorporate energy-efficient compressors, corrosion-resistant materials, and automated monitoring systems that ensure reliable performance in demanding environments. The ice produced typically measures between 1 to 2 millimeters in thickness, providing exceptional cooling efficiency due to increased surface area compared to traditional ice forms. These machines serve critical roles in seafood preservation, concrete cooling, medical applications, food processing, and commercial fishing operations. The technology behind a high quality flake ice machine has evolved significantly, now featuring microprocessor controls that optimize production cycles, reduce energy consumption, and extend equipment longevity. Installation flexibility allows these systems to operate in various settings, from compact restaurant kitchens to large-scale industrial facilities. The stainless steel construction common in premium models ensures hygiene standards are maintained while resisting environmental degradation. Production capacities range from small units generating 100 kilograms daily to industrial systems producing several tons per day, accommodating businesses of all scales. The rapid cooling properties of flake ice make it indispensable for temperature-sensitive applications where maintaining product quality is paramount. A high quality flake ice machine delivers consistent output regardless of ambient conditions, thanks to advanced refrigeration technology and robust component selection that withstands continuous operation in challenging environments.

New Products

Investing in a high quality flake ice machine delivers measurable benefits that directly impact operational efficiency and product quality. The primary advantage lies in superior cooling performance, as flake ice provides approximately 20 percent more surface area than cube or block ice, enabling faster temperature reduction for perishable goods. This rapid cooling capability translates to extended product freshness, reduced spoilage rates, and improved customer satisfaction across food service and retail sectors. Energy efficiency represents another compelling benefit, with modern systems consuming significantly less electricity than older refrigeration methods while maintaining higher output levels. The automated operation of a high quality flake ice machine minimizes labor requirements, freeing staff to focus on core business activities rather than manual ice production or procurement. Businesses eliminate the recurring costs and logistical challenges associated with purchasing bagged ice, achieving return on investment typically within 18 to 24 months depending on usage volume. The dry, subcooled nature of flake ice prevents clumping and allows easy handling, storage, and distribution throughout facilities. Hygiene standards improve dramatically when organizations control their ice production internally, as a high quality flake ice machine operates in a closed system that reduces contamination risks compared to externally sourced ice. Maintenance requirements remain minimal due to durable construction and self-cleaning features integrated into premium models, reducing downtime and repair expenses. The versatility of flake ice accommodates diverse applications, from displaying fresh seafood and produce to therapeutic uses in medical settings and concrete temperature management in construction projects. Space efficiency characterizes modern designs, with compact footprints that fit into existing layouts without requiring extensive facility modifications. Operational reliability ensures consistent ice availability during peak demand periods, eliminating the anxiety of running short during critical business hours. The gentle texture of flake ice prevents damage to delicate products like fish fillets or fresh vegetables during storage and display. Temperature control precision improves across all applications, as the small ice particles conform to product contours and eliminate air gaps that reduce cooling effectiveness. A high quality flake ice machine also supports sustainability initiatives by reducing transportation emissions associated with ice delivery and minimizing packaging waste from bagged ice purchases. The long service life of quality equipment, often exceeding 10 years with proper maintenance, provides stable operational costs and predictable budgeting. Businesses gain competitive advantages through improved product presentation, extended shelf life, and the ability to meet stringent food safety regulations that increasingly govern temperature control in commercial settings.

Latest News

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

08

May

Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

When industrial buyers and plant managers evaluate large-scale ice production systems, one question consistently surfaces: is a tube ice maker machine genuinely capable of meeting high-capacity manufacturing demands? The answer is not simply yes or n...
View More
Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

18

May

Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

When it comes to preserving freshness and extending the shelf life of seafood products, the choice of ice type and ice-making equipment is far from trivial. Commercial seafood markets operate under strict hygiene standards, high-volume throughput dem...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high quality flake ice machine

Advanced Refrigeration Technology for Consistent Performance

Advanced Refrigeration Technology for Consistent Performance

The engineering excellence behind a high quality flake ice machine centers on sophisticated refrigeration systems that deliver unwavering performance across varying operational demands and environmental conditions. At the core lies a precision-designed evaporator drum manufactured from specialized alloys that optimize heat transfer while resisting corrosion from continuous water exposure. This cylindrical component rotates at carefully calibrated speeds, allowing water to freeze uniformly across its surface before mechanical scrapers remove the ice in thin, consistent flakes. The refrigeration circuit employs high-efficiency compressors that utilize environmentally responsible refrigerants, balancing powerful cooling capacity with reduced energy consumption and minimal environmental impact. Intelligent control systems monitor multiple parameters including water temperature, ice thickness, production rate, and system pressures, making real-time adjustments that maintain optimal performance without operator intervention. These automated controls prevent common issues such as ice bridging, inconsistent flake size, or production interruptions that plague inferior equipment. The water distribution system in a high quality flake ice machine features precision nozzles or spray bars that ensure even coverage across the evaporator surface, eliminating dry spots that would compromise ice quality or reduce output. Insulation materials surrounding critical components minimize thermal loss, enhancing energy efficiency while protecting internal mechanisms from ambient temperature fluctuations. The defrost cycle, when required, operates seamlessly through hot gas bypass or electric heating elements that quickly clear any ice buildup without disrupting production schedules. Vibration dampening systems reduce operational noise, making these machines suitable for customer-facing environments where excessive sound would detract from the experience. The integration of diagnostic capabilities allows maintenance personnel to identify potential issues before they escalate into costly failures, with many modern units offering remote monitoring through network connectivity. This technological sophistication translates into production consistency that businesses can depend upon, with output rates remaining stable regardless of seasonal temperature variations or fluctuating demand patterns. The durability of components selected for a high quality flake ice machine reflects engineering decisions that prioritize longevity over initial cost savings, utilizing bearings, seals, and motors rated for continuous duty cycles that extend equipment lifespan significantly beyond economy alternatives.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

The remarkable adaptability of a high quality flake ice machine makes it an invaluable asset across numerous sectors, each benefiting from the unique properties of flake ice in distinct ways. In commercial fishing and seafood processing, flake ice serves as the gold standard for preserving catch quality from boat to market, as the small ice particles nestle between fish, creating a protective barrier that maintains optimal temperature while preventing tissue damage that larger ice forms might cause. Supermarkets and fish markets rely on flake ice for stunning product displays, where the ice bed showcases fresh seafood while maintaining the cold chain that preserves flavor, texture, and safety. The food processing industry utilizes a high quality flake ice machine for applications ranging from mixing into ground meat products to cooling bakery dough, where temperature control during production directly affects final product quality. Healthcare facilities employ flake ice for therapeutic purposes, including post-surgical recovery treatments and sports medicine applications where the moldable nature of flake ice conforms to body contours for effective cold therapy. Concrete cooling represents a critical construction application, particularly in large-scale projects or hot climates, where adding flake ice to concrete mixes controls the exothermic curing reaction, preventing structural weaknesses and cracking that would compromise building integrity. Chemical processing plants integrate flake ice into various manufacturing processes requiring precise temperature management during reactions or product formulation. The hospitality sector, including hotels, restaurants, and catering operations, depends on a high quality flake ice machine for salad bars, beverage service, and food presentation that meets both aesthetic and safety standards. Agricultural applications include produce cooling immediately after harvest, where rapid temperature reduction extends shelf life and maintains nutritional value during transportation to distribution centers. Laboratory environments utilize flake ice for sample preservation, equipment cooling, and experimental procedures requiring consistent, contamination-free ice. The versatility extends to industrial applications such as cooling machinery, controlling fermentation temperatures in breweries, and maintaining product quality in pharmaceutical manufacturing. Each industry benefits from the specific characteristics of flake ice, including its high surface area for efficient heat transfer, dry texture that prevents excessive moisture, and gentle handling properties that protect delicate materials. A high quality flake ice machine adapts to these varied demands through adjustable production settings, sanitary design features, and robust construction that withstands the unique challenges of different operational environments.
Economic Benefits and Return on Investment

Economic Benefits and Return on Investment

The financial advantages of installing a high quality flake ice machine extend far beyond the initial purchase price, creating a compelling economic case that resonates with cost-conscious business operators across all sectors. Eliminating recurring ice purchases represents the most immediate savings, as businesses currently buying bagged ice typically spend substantial amounts annually on a commodity they can produce internally at a fraction of the cost. The per-kilogram production cost of ice from a quality machine often runs 70 to 80 percent lower than purchased ice, with the differential becoming more pronounced as production volume increases. Energy efficiency improvements in modern equipment mean that operational costs remain manageable even with continuous production, as advanced compressors and optimized refrigeration cycles minimize electricity consumption while maximizing output. Labor savings accumulate through automated operation that requires minimal supervision, contrasting sharply with the time employees spend managing ice deliveries, storage, and inventory. The reliability of a high quality flake ice machine prevents costly disruptions that occur when ice supplies run short during peak business periods, protecting revenue streams that depend on consistent product availability. Product loss reduction contributes significantly to the economic equation, as proper ice availability and quality preservation techniques enabled by flake ice minimize spoilage of perishable inventory. The extended equipment lifespan characteristic of quality construction means that the initial investment amortizes over many years of dependable service, with total cost of ownership remaining favorable compared to cheaper alternatives requiring frequent replacement. Maintenance expenses stay predictable and reasonable due to durable components and accessible design that simplifies routine service tasks, avoiding the surprise repair bills that plague poorly manufactured equipment. Tax advantages may apply in many jurisdictions, where equipment purchases qualify for depreciation schedules or energy efficiency incentives that reduce net investment costs. The competitive advantages gained through superior product quality, consistent availability, and operational flexibility translate into revenue growth that accelerates payback periods beyond simple cost savings calculations. Businesses report improved customer satisfaction when product quality improves through better temperature management, leading to repeat purchases and positive reputation effects that drive long-term profitability. The scalability of a high quality flake ice machine allows organizations to match production capacity with actual needs, avoiding both the waste of excess capacity and the limitations of undersized equipment. Financing options available for commercial equipment purchases enable businesses to preserve working capital while still accessing the benefits of modern ice production technology. The environmental benefits of reduced transportation and packaging waste align with corporate sustainability goals while potentially qualifying for green business certifications that appeal to environmentally conscious consumers. Risk mitigation represents another economic dimension, as controlling ice production internally eliminates supply chain vulnerabilities that could disrupt operations during supplier issues or seasonal shortages.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000