custom commercial cube ice maker
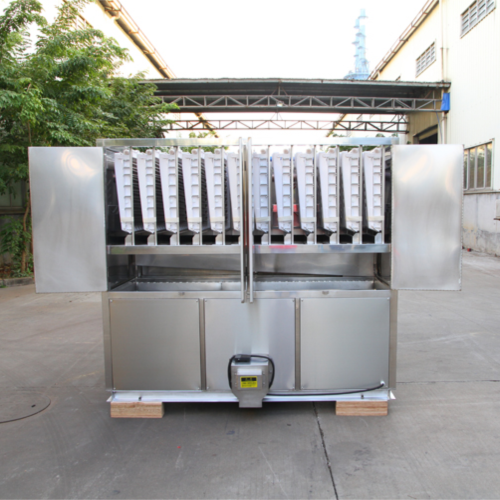
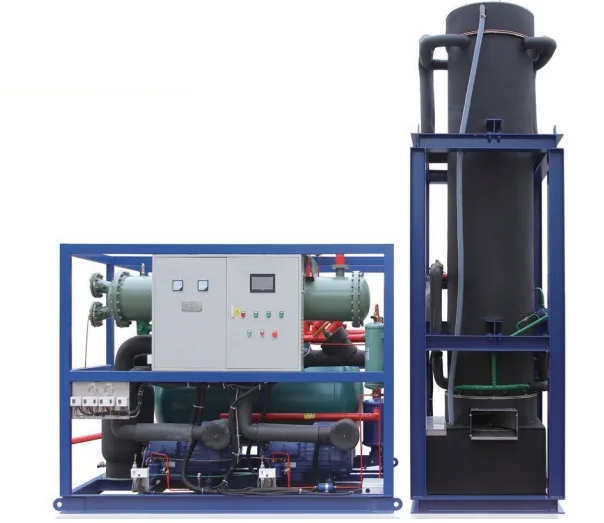
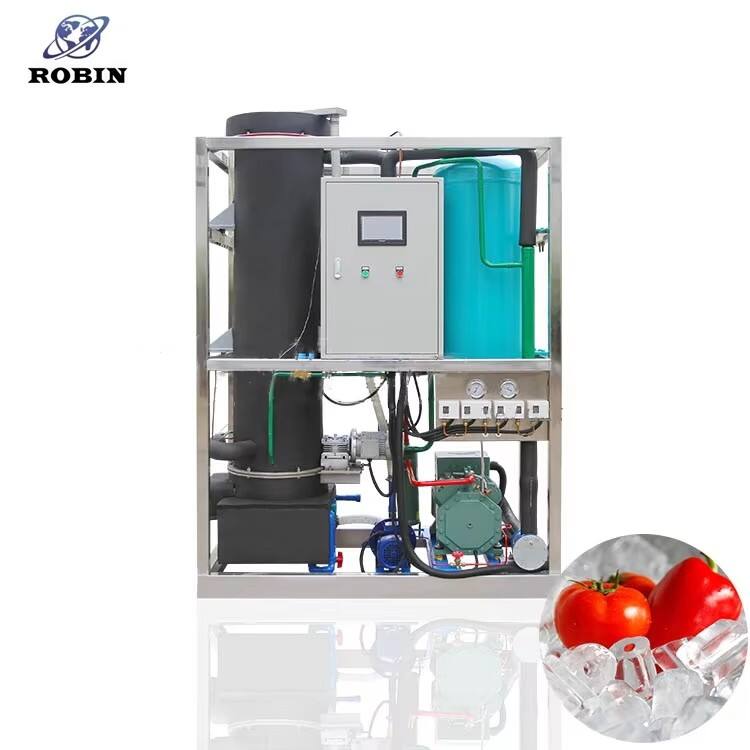
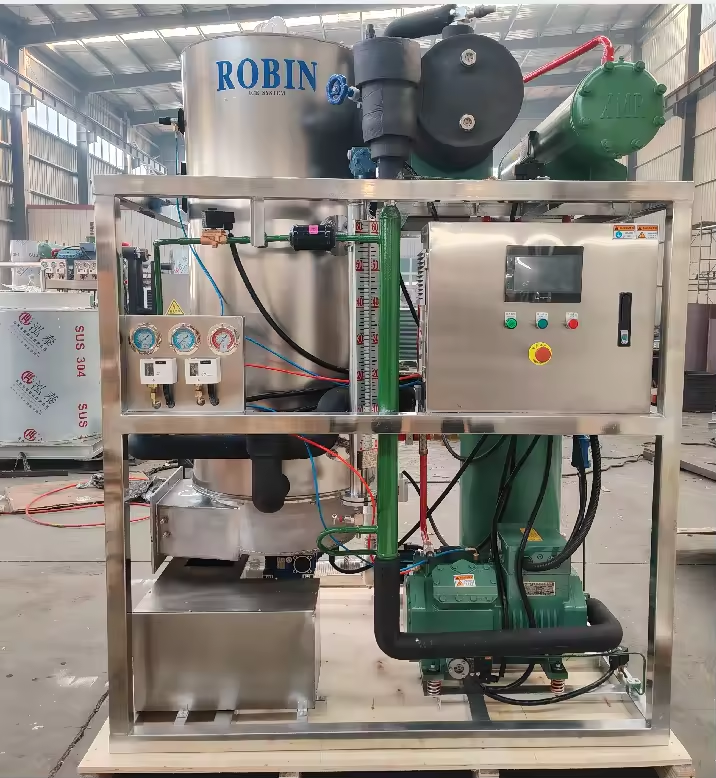
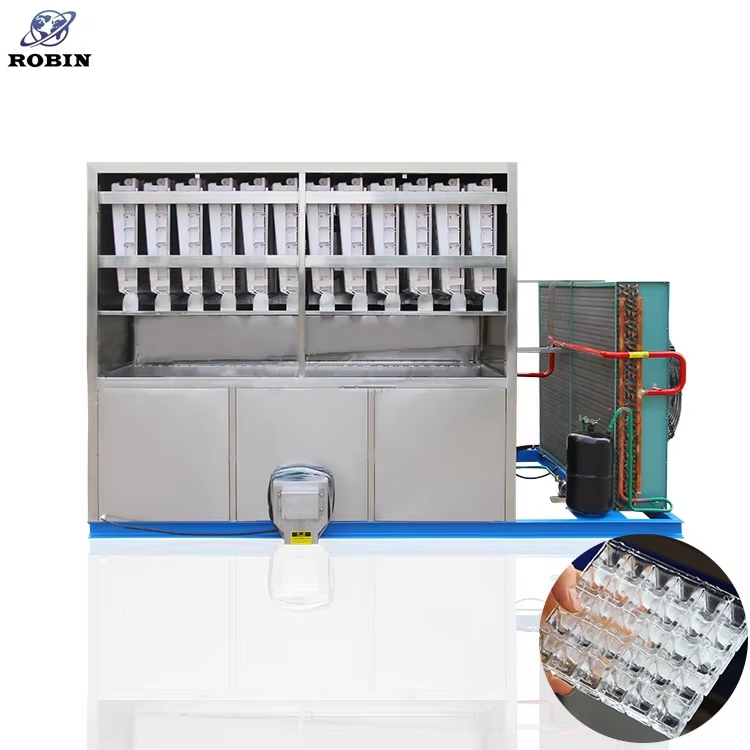
A custom commercial cube ice maker represents a specialized refrigeration solution designed to produce consistent, high-quality ice cubes for businesses across various industries. This equipment serves as an essential component for restaurants, hotels, bars, healthcare facilities, and food service operations that require reliable ice production throughout their operating hours. The custom commercial cube ice maker distinguishes itself through its ability to generate perfectly formed ice cubes that maintain their shape longer than traditional ice, providing superior cooling performance and aesthetic appeal in beverages. These machines incorporate advanced freezing technology that ensures each cube meets exact specifications for size, clarity, and density. The customization aspect allows businesses to select specific cube dimensions, production capacities, and operational features that align with their unique requirements. Modern custom commercial cube ice makers utilize efficient compressor systems, precise water filtration mechanisms, and intelligent control panels that monitor production cycles and maintain optimal performance. The equipment typically features stainless steel construction for durability and hygiene compliance, making it suitable for demanding commercial environments. Production capacity varies significantly across different models, ranging from compact units producing 50 pounds daily to industrial-scale systems generating over 1000 pounds of ice per day. The custom commercial cube ice maker integrates seamlessly into existing kitchen layouts or bar setups, with options for undercounter installation, modular stacking configurations, or standalone placement. Energy efficiency has become a critical consideration in modern designs, with manufacturers implementing eco-friendly refrigerants and optimized cooling cycles that reduce electricity consumption while maintaining consistent output. The ice production process involves precise water distribution over evaporator plates, controlled freezing periods, and automated harvesting mechanisms that release finished cubes into insulated storage bins. These systems often include built-in diagnostics that alert operators to maintenance needs, water quality issues, or performance irregularities before they impact production.

 EN