Industrial Cube Ice Machine Supplier - Commercial Ice Equipment Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial cube ice machine supplier

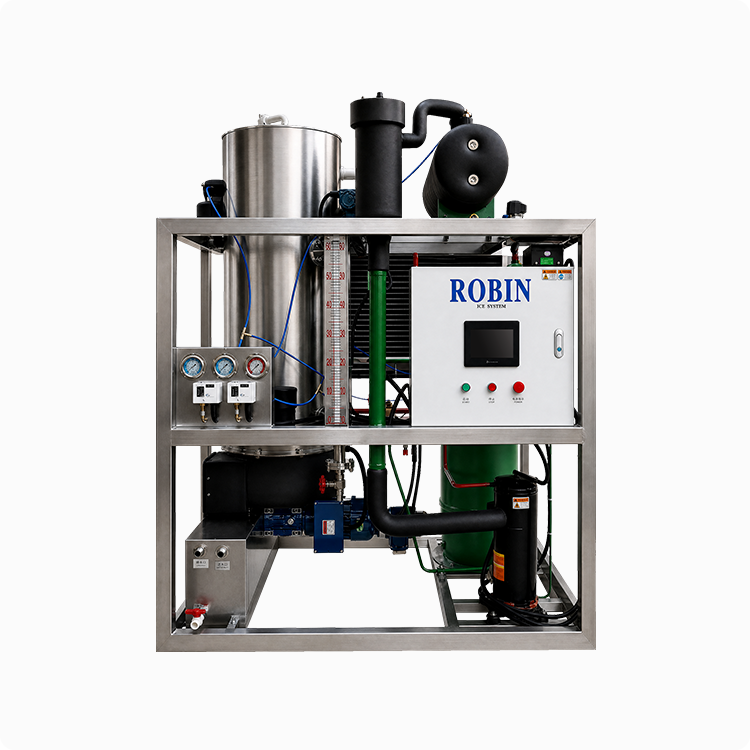
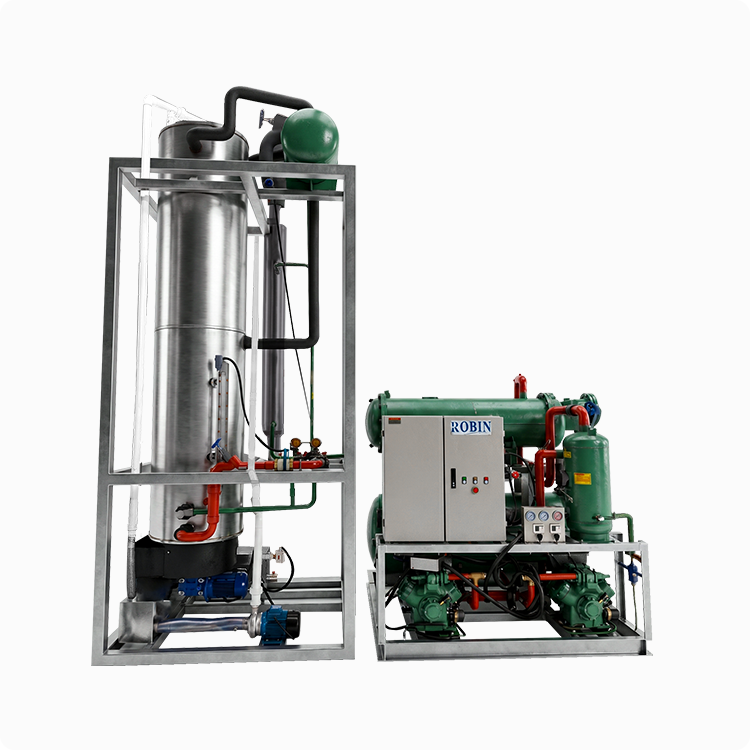
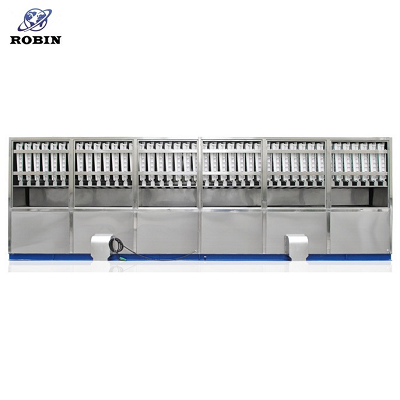
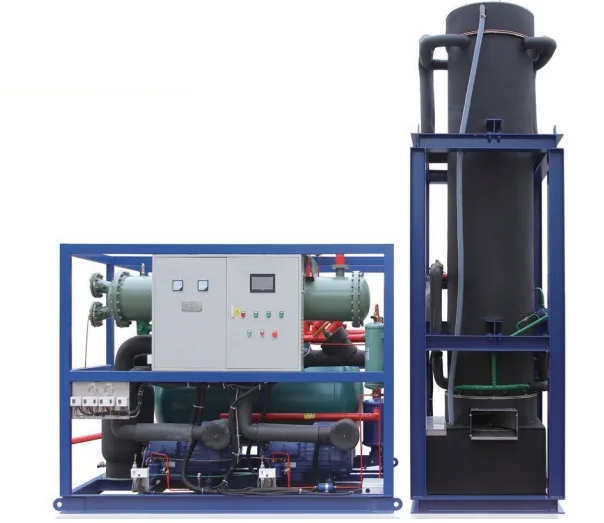
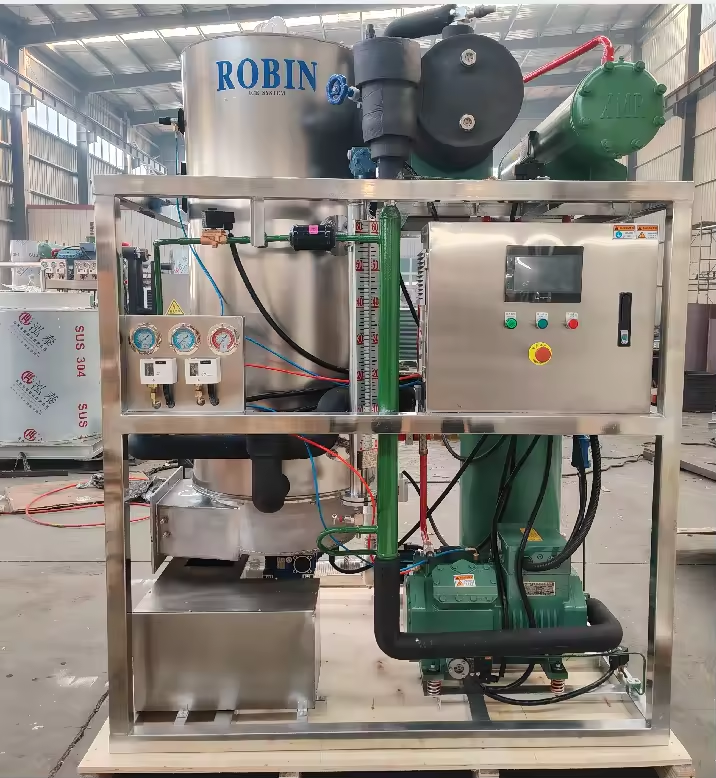
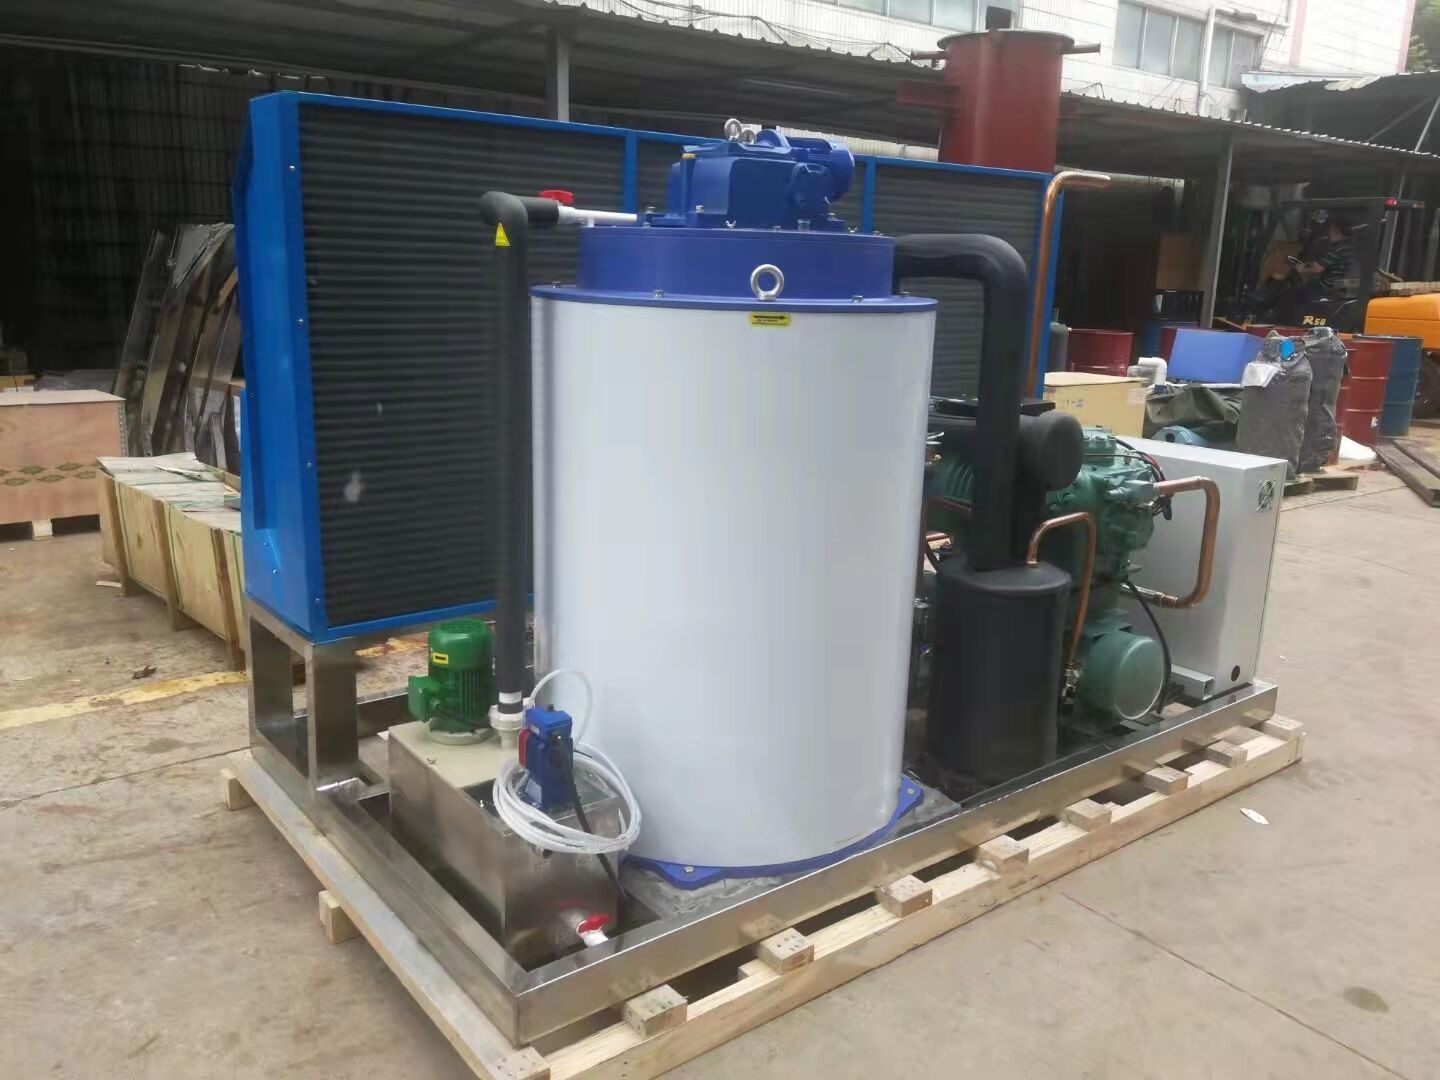
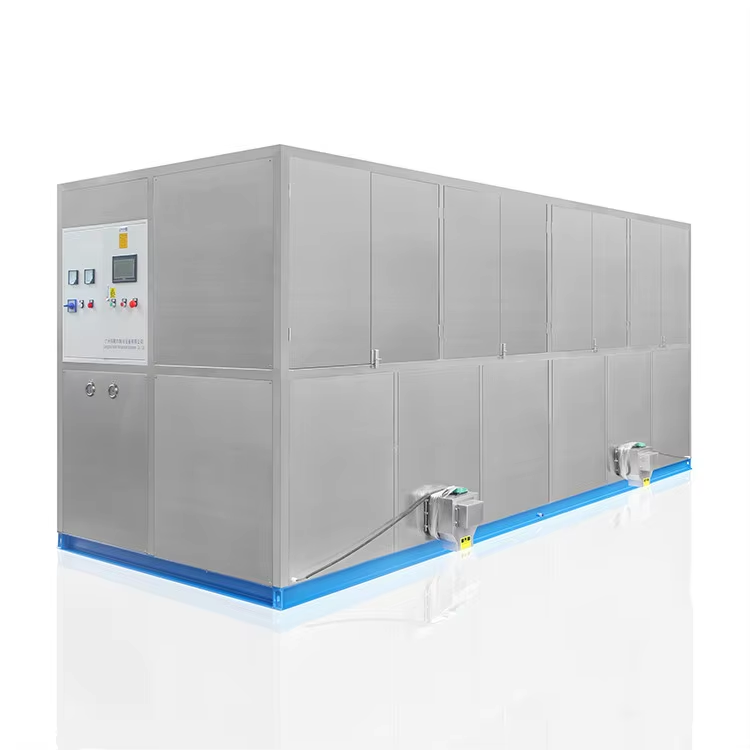
An industrial cube ice machine supplier provides essential equipment for businesses requiring consistent, high-volume ice production. These suppliers specialize in manufacturing and distributing commercial-grade ice makers that produce uniform cube-shaped ice, which has become the standard in hospitality, food service, healthcare, and retail industries. The primary function of these machines centers on converting water into perfectly formed ice cubes through advanced refrigeration technology, ensuring reliable output that meets demanding operational requirements. Industrial cube ice machine suppliers offer equipment ranging from compact units producing several hundred pounds daily to large-scale systems capable of generating thousands of pounds of ice every 24 hours. The technological features integrated into modern industrial cube ice machines include energy-efficient compressors, automated cleaning cycles, intelligent diagnostic systems, and precise temperature controls that maintain optimal ice production conditions. These machines utilize either air-cooled or water-cooled condensing systems, with many suppliers offering both options to accommodate different facility requirements and environmental considerations. The cube ice produced by these industrial systems typically measures between 7/8 inch to 1-1/8 inch, providing the ideal size for beverage service, food preservation, and therapeutic applications. Applications for industrial cube ice machines span numerous sectors including restaurants, hotels, hospitals, convenience stores, bars, catering operations, fisheries, and food processing facilities. Each application benefits from the consistent quality and reliable production capacity that professional-grade equipment delivers. Industrial cube ice machine suppliers also provide comprehensive support services including installation guidance, maintenance programs, replacement parts availability, and technical assistance to ensure continuous operation. The selection process when working with an industrial cube ice machine supplier involves evaluating production capacity needs, available space, water quality, ambient temperature conditions, and specific ice quality requirements. Leading suppliers offer customization options and can recommend appropriate models based on detailed operational assessments, ensuring businesses invest in equipment that precisely matches their ice production demands while optimizing energy consumption and operational efficiency.


New Product Releases

Working with a reputable industrial cube ice machine supplier delivers numerous practical benefits that directly impact your business operations and bottom line. First and foremost, these suppliers provide access to equipment engineered for durability and consistent performance under demanding commercial conditions. Unlike residential ice makers, industrial cube ice machines feature heavy-duty components designed to operate continuously without degradation in ice quality or production speed. This reliability translates to fewer service interruptions and reduced downtime costs. The energy efficiency of modern industrial cube ice machines represents another significant advantage, as leading suppliers incorporate advanced refrigeration technology that minimizes electricity consumption while maximizing ice output. This efficiency directly reduces operational expenses, with many businesses recovering their equipment investment through energy savings alone within several years. Industrial cube ice machine suppliers also offer equipment with superior sanitation features, including antimicrobial components, automatic cleaning cycles, and designs that prevent contamination. These features prove essential for businesses in food service and healthcare where ice quality directly affects customer safety and regulatory compliance. The cube shape itself provides distinct advantages over other ice forms, as cubes melt slower than flaked or crushed ice, maintaining beverage temperature without excessive dilution. This characteristic enhances customer satisfaction in hospitality settings while reducing ice waste. Another practical benefit involves the scalability options available through industrial cube ice machine suppliers. As your business grows, suppliers can provide larger capacity units or multiple machines that integrate seamlessly with existing equipment, protecting your initial investment while accommodating expansion. The technical support and warranty coverage offered by established suppliers provide peace of mind and protect against unexpected repair costs. Many suppliers maintain extensive parts inventories and employ trained technicians who understand the specific requirements of commercial ice production equipment. This support network ensures rapid response when service needs arise, minimizing operational disruptions. Industrial cube ice machine suppliers also stay current with evolving regulations regarding refrigerants, water usage, and energy standards, ensuring the equipment they provide meets all applicable codes and environmental requirements. This compliance assistance saves businesses from costly retrofits or premature equipment replacement. The purchasing flexibility offered by industrial cube ice machine suppliers represents another advantage, with options including outright purchase, leasing arrangements, and financing programs that accommodate different budget structures and cash flow preferences. This flexibility makes professional-grade ice production accessible to businesses of all sizes. Finally, the consultation services provided by knowledgeable suppliers help businesses avoid common mistakes such as undersizing equipment, selecting inappropriate models for specific water conditions, or installing machines in locations with inadequate ventilation, all of which can compromise performance and increase operating costs.

Latest News

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

12

May

How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

In food processing, healthcare, fisheries, and beverage production, the integrity of ice directly affects product safety and regulatory compliance. A tube ice maker machine is engineered from the ground up to meet the demanding hygiene standards that...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial cube ice machine supplier

Advanced Refrigeration Technology for Maximum Efficiency

Advanced Refrigeration Technology for Maximum Efficiency

Industrial cube ice machine suppliers distinguish themselves through their commitment to incorporating cutting-edge refrigeration technology that maximizes production efficiency while minimizing environmental impact and operational costs. Modern industrial cube ice machines utilize sophisticated compressor systems that optimize refrigerant flow based on ambient conditions and production demands, automatically adjusting performance parameters to maintain consistent ice output regardless of external temperature fluctuations. This adaptive technology ensures that businesses receive reliable ice production even during peak summer months when demand typically increases and ambient temperatures challenge equipment performance. The refrigeration systems employed by leading industrial cube ice machine suppliers feature enhanced heat exchange surfaces that improve thermal transfer efficiency, reducing the energy required to freeze water into ice cubes. These improvements translate directly into lower electricity bills, with some advanced models consuming up to 30 percent less energy than older generation equipment while producing equivalent or greater ice quantities. Environmental considerations have driven industrial cube ice machine suppliers to adopt eco-friendly refrigerants that comply with international environmental protocols while maintaining excellent thermodynamic properties. These modern refrigerants eliminate the ozone depletion concerns associated with older compounds while providing superior cooling performance. The technological sophistication extends to intelligent control systems that monitor multiple operational parameters including water temperature, refrigerant pressure, ice thickness, and harvest cycle timing. These systems automatically optimize each production cycle, ensuring cubes form to precise specifications before harvest, which maximizes yield and minimizes wasted energy on incomplete freeze cycles. Industrial cube ice machine suppliers also incorporate variable-speed fan motors in air-cooled models, which adjust airflow based on actual cooling requirements rather than running constantly at full speed. This variable-speed technology reduces noise levels, extends component life, and further decreases energy consumption. The insulation materials used in modern industrial cube ice machines represent another technological advancement, with high-density foam insulation that minimizes thermal loss and maintains optimal freezing chamber temperatures with less compressor runtime. This insulation technology proves particularly valuable in warm environments where ambient heat would otherwise force equipment to work harder. Leading industrial cube ice machine suppliers also offer models with hot gas defrost systems that use waste heat from the refrigeration cycle to efficiently clear ice from evaporator plates during harvest cycles, eliminating the need for electric heating elements and reducing harvest time. This technology increases daily production capacity while decreasing energy consumption per pound of ice produced.
Comprehensive Sanitation Features for Food Safety Compliance

Comprehensive Sanitation Features for Food Safety Compliance

Industrial cube ice machine suppliers recognize that ice quality and sanitation represent critical concerns for businesses in food service, healthcare, and hospitality sectors, which has driven the development of comprehensive sanitation features that exceed basic regulatory requirements. Modern industrial cube ice machines incorporate antimicrobial materials in key components including water distribution systems, storage bins, and contact surfaces where bacteria, mold, and slime could potentially develop. These antimicrobial treatments actively inhibit microbial growth between cleaning cycles, maintaining ice purity even during extended operation periods. The design philosophy embraced by leading industrial cube ice machine suppliers emphasizes accessibility for cleaning and inspection, with removable panels, easily accessible water filters, and component layouts that allow thorough sanitation without requiring specialized tools or extensive disassembly. This accessibility ensures that routine maintenance tasks can be completed quickly by staff members, promoting consistent adherence to cleaning schedules. Advanced filtration systems offered by industrial cube ice machine suppliers remove sediment, chlorine, minerals, and other contaminants from incoming water before it enters the freezing cycle. These filtration systems not only improve ice clarity and taste but also protect internal components from scale buildup that can harbor bacteria and reduce equipment efficiency. Many suppliers offer multi-stage filtration options that can be customized based on local water quality conditions, ensuring optimal results regardless of source water characteristics. Automatic cleaning cycles represent another significant sanitation advantage available through industrial cube ice machine suppliers. These systems periodically flush water distribution components, sanitize contact surfaces, and remove mineral deposits without requiring manual intervention. The automation ensures cleaning occurs on schedule even during busy periods when staff might otherwise postpone maintenance tasks. Industrial cube ice machine suppliers also provide equipment with sealed water systems that prevent airborne contaminants from entering the ice production pathway. These sealed systems include covered water reservoirs, enclosed distribution manifolds, and protected evaporator surfaces that minimize contamination risks. The cube ice production method itself offers sanitation advantages, as the freezing process occurs in individual cube cells that prevent cross-contamination between ice pieces. This cell-based freezing contrasts with flake or nugget ice production where ice particles contact each other during formation, potentially spreading any contamination. Leading industrial cube ice machine suppliers incorporate diagnostic systems that alert operators to conditions that could compromise ice quality, including elevated water temperature, inadequate sanitizer levels, or extended periods between cleaning cycles. These alerts enable proactive intervention before sanitation issues affect ice quality or customer safety. The storage bin designs offered by industrial cube ice machine suppliers feature sloped floors that promote complete drainage, preventing standing water where bacteria could multiply. These bins also include sealed doors with gaskets that prevent external contamination while maintaining proper temperature and humidity levels.
Flexible Capacity Options and Scalable Solutions

Flexible Capacity Options and Scalable Solutions

Industrial cube ice machine suppliers understand that businesses have vastly different ice production requirements based on their size, industry, and operational patterns, which has led to the development of extensive product lines offering flexible capacity options and scalable solutions that accommodate diverse needs. The capacity range available through industrial cube ice machine suppliers spans from compact undercounter units producing 200 pounds daily, suitable for small cafes or medical offices, to massive modular systems generating over 10,000 pounds per day for large hotels, hospitals, or food processing facilities. This breadth ensures businesses can select equipment precisely matched to their actual consumption patterns without paying for excess capacity or suffering from inadequate production. Industrial cube ice machine suppliers provide detailed capacity planning assistance, analyzing factors including peak demand periods, storage limitations, ambient temperature conditions, and growth projections to recommend appropriate equipment configurations. This consultation process prevents common sizing errors that result in either insufficient ice during busy periods or wasted energy producing ice that melts unused in storage. The modular approach offered by leading industrial cube ice machine suppliers allows businesses to install multiple smaller units rather than single large machines, providing operational redundancy that ensures continued ice availability even if one unit requires service. This redundancy proves particularly valuable for businesses where ice shortages would severely impact operations or customer satisfaction. Scalability represents a crucial advantage when working with established industrial cube ice machine suppliers, as businesses can start with appropriately sized equipment and add capacity as operations expand. The compatibility between different models within a supplier's product line ensures that additional units integrate seamlessly with existing equipment, sharing storage bins, water supplies, and drainage systems without requiring extensive modifications. Industrial cube ice machine suppliers also offer equipment with adjustable production settings that allow operators to increase or decrease output based on seasonal demand variations. This adjustability prevents energy waste during slower periods while ensuring adequate production during peak seasons. The storage bin options available through industrial cube ice machine suppliers range from integrated bins built into the machine housing to large-capacity remote bins that can hold several days' worth of production. This flexibility allows businesses to configure systems that match their specific space constraints and usage patterns. Remote ice storage proves particularly valuable for operations with limited space in service areas but available storage in back-of-house locations. Industrial cube ice machine suppliers provide the necessary components including insulated bins, ice transport systems, and dispensing equipment to create efficient remote storage configurations. The installation flexibility offered by industrial cube ice machine suppliers accommodates various facility layouts and utility configurations. Equipment is available in air-cooled, water-cooled, and remote-cooled configurations, each suited to different environmental conditions and infrastructure capabilities. This variety ensures businesses can install industrial cube ice machines in locations ranging from compact kitchens to large mechanical rooms without compromising performance or efficiency.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000