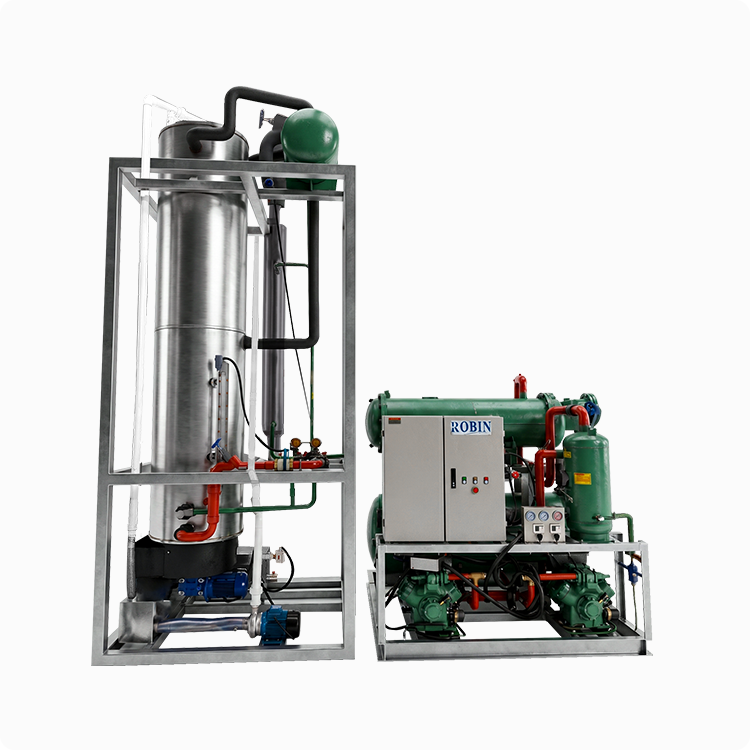
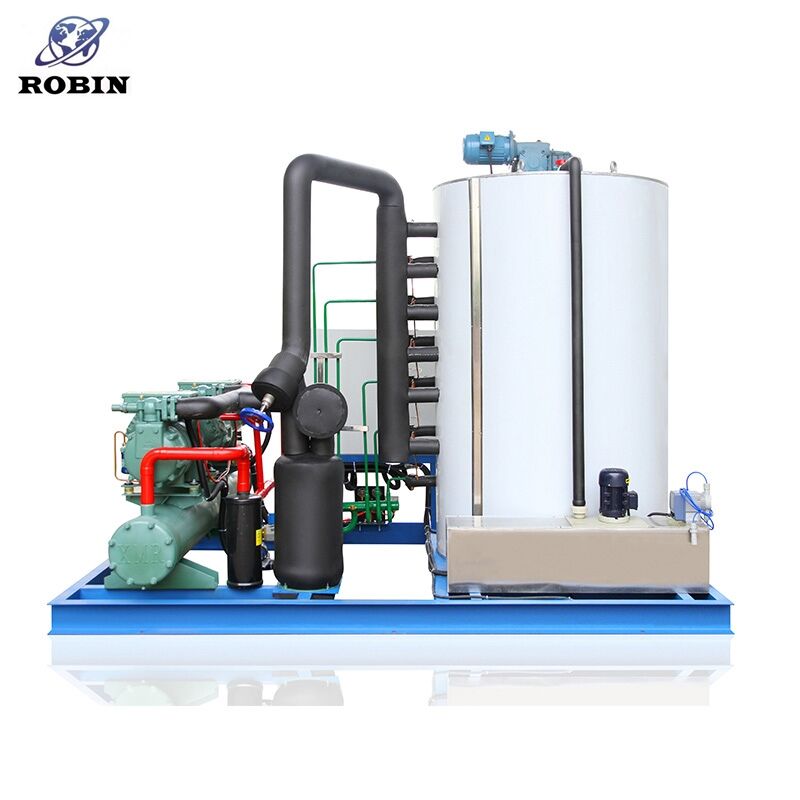
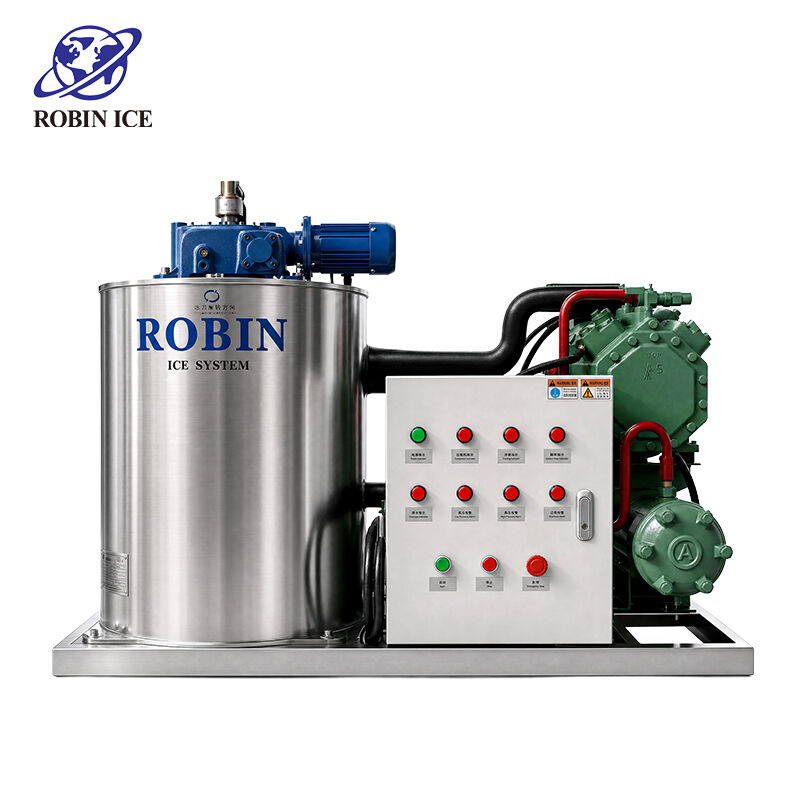
Industrial Ice Cube Machines - High-Capacity Commercial Ice Production Systems

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

ice cube industrial machine

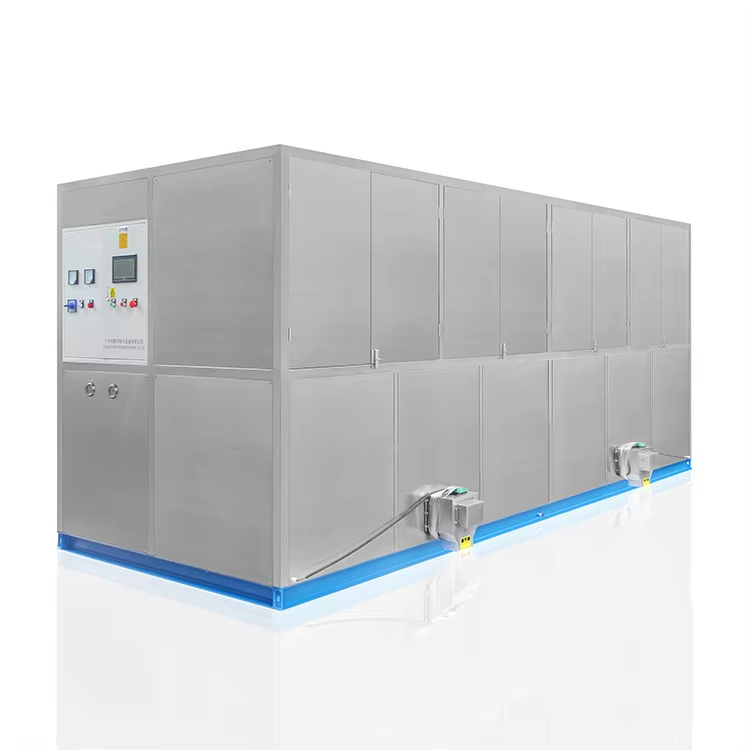
An ice cube industrial machine represents a critical investment for businesses requiring consistent, high-volume ice production. These sophisticated systems are engineered to produce large quantities of uniform ice cubes efficiently, serving diverse commercial sectors from hospitality to healthcare. The primary function of an ice cube industrial machine centers on transforming purified water into perfectly shaped ice cubes through advanced refrigeration technology. Modern units incorporate automated water filtration systems that remove impurities, ensuring crystal-clear ice production that meets stringent health standards. The technological framework includes precision temperature controls, automated harvest cycles, and intelligent monitoring systems that optimize energy consumption while maintaining peak performance. Industrial-grade compressors work alongside high-efficiency evaporators to accelerate freezing processes, enabling rapid production cycles that can generate hundreds of pounds of ice daily. These machines feature stainless steel construction that resists corrosion and simplifies sanitation procedures, making them ideal for food service environments. Advanced models integrate smart diagnostics that alert operators to maintenance needs before breakdowns occur, minimizing costly downtime. The application spectrum spans restaurants, hotels, hospitals, convenience stores, bars, catering operations, and food processing facilities. Each ice cube industrial machine can be configured to produce various cube sizes, from standard cubes for beverages to smaller nugget ice for blended drinks. The automated operation reduces labor requirements, as machines continuously produce ice without constant supervision. Storage bins maintain ice at optimal temperatures, preventing melting and ensuring immediate availability during peak demand periods. Energy-efficient designs incorporate insulation technologies that reduce power consumption while maintaining consistent output. The versatility of these systems allows businesses to scale production according to seasonal fluctuations and operational demands, providing flexibility that manual ice production cannot match.

New Products

Investing in an ice cube industrial machine delivers substantial operational benefits that directly impact your bottom line. First, these systems dramatically reduce labor costs by eliminating the need for staff to manually fill trays, monitor freezing, or transport ice from external suppliers. Your team can focus on core business activities while the machine operates autonomously, producing ice around the clock without breaks or supervision. The consistency of output ensures you never face shortages during rush periods, protecting revenue streams and customer satisfaction. Production capacity scales to meet your specific needs, with models ranging from compact units generating 50 pounds daily to industrial powerhouses producing over 1,000 pounds. This scalability means you pay only for the capacity you require, avoiding waste while ensuring adequate supply. Energy efficiency translates to lower utility bills, as modern ice cube industrial machines use advanced insulation and optimized refrigeration cycles that consume less power than older models. The long-term cost savings become evident when comparing ongoing supplier fees against the one-time equipment investment and minimal operating expenses. Quality control improves significantly because you control the entire production process, from water filtration to storage conditions. This control eliminates concerns about contamination during transportation or storage at supplier facilities. The ice produced maintains uniform size and clarity, enhancing beverage presentation and customer perception of quality. Maintenance requirements remain minimal, with most machines requiring only periodic cleaning and filter replacements that staff can perform without specialized training. Reliability proves exceptional, as industrial-grade components withstand continuous operation in demanding environments. The immediate availability of ice eliminates dependency on delivery schedules, preventing disruptions caused by supplier delays or transportation issues. Space efficiency allows installation in various locations, from back-of-house areas to dedicated ice production rooms. The machines operate quietly, avoiding noise disturbances in customer-facing areas. Hygiene standards reach new heights because automated systems minimize human contact with ice, reducing contamination risks. The return on investment typically occurs within 18 to 24 months for high-volume operations, after which the machine generates pure savings. Flexibility extends to ice type selection, allowing you to switch between cube sizes based on seasonal menu changes or special events. The professional appearance of an ice cube industrial machine also enhances your facility's credibility, demonstrating commitment to quality and operational excellence that customers and health inspectors appreciate.

Practical Tips

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

06

May

How Is Ice Tube Machine Used in Commercial Beverage and Food Industries?

The ice tube machine has become an essential piece of equipment across a wide range of commercial operations, from busy restaurant kitchens to large-scale food processing facilities. Its ability to produce cylindrical ice in consistent shapes and siz...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

18

May

Is Flake Ice Machine for Fish Suitable for Commercial Seafood Markets?

When it comes to preserving freshness and extending the shelf life of seafood products, the choice of ice type and ice-making equipment is far from trivial. Commercial seafood markets operate under strict hygiene standards, high-volume throughput dem...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

ice cube industrial machine

Unmatched Production Efficiency and Consistency

Unmatched Production Efficiency and Consistency

The production efficiency of an ice cube industrial machine sets it apart from all alternative ice sourcing methods. These systems employ cutting-edge refrigeration technology that accelerates the freezing process while maintaining exceptional energy efficiency. The core advantage lies in continuous operation capability, where machines produce ice in systematic cycles without requiring downtime between batches. Advanced evaporator designs maximize surface contact between water and refrigerated components, reducing freeze times significantly compared to traditional methods. This efficiency means a single ice cube industrial machine can replace multiple smaller units or eliminate dependency on external suppliers entirely. The consistency of output proves equally valuable, as each production cycle generates ice cubes with identical dimensions, clarity, and density. This uniformity matters tremendously in commercial settings where beverage presentation affects customer perception and satisfaction. Automated water distribution systems ensure precise filling of ice molds, preventing variations that occur with manual processes. The machines maintain optimal freezing temperatures throughout each cycle, eliminating the partially frozen or irregularly shaped cubes that plague inconsistent systems. Smart sensors monitor production stages and adjust parameters automatically, compensating for ambient temperature fluctuations or water supply variations. This intelligent operation ensures that the first cube produced in the morning matches the last cube made at night, providing reliability that businesses can depend upon. The efficiency extends beyond production speed to include resource utilization, as modern ice cube industrial machines waste minimal water through optimized harvest cycles and recirculation systems. Energy consumption remains remarkably low considering output volume, thanks to high-efficiency compressors and superior insulation that prevents thermal loss. The combination of speed, consistency, and resource efficiency creates a production environment where businesses can confidently plan operations knowing their ice supply will never become a limiting factor. This reliability transforms ice from a potential operational bottleneck into a seamlessly managed resource that supports rather than constrains business growth.
Superior Hygiene and Food Safety Compliance

Superior Hygiene and Food Safety Compliance

Hygiene represents a paramount concern for any business serving food or beverages, and an ice cube industrial machine delivers uncompromising sanitation standards. The closed-system design prevents airborne contaminants from reaching ice during production, a critical advantage over open containers or manual ice handling. Stainless steel construction throughout the machine provides non-porous surfaces that resist bacterial growth and simplify cleaning procedures. Antimicrobial coatings on key components add an extra layer of protection, actively inhibiting microorganism proliferation in areas that contact water or ice. The automated production process minimizes human contact, eliminating the contamination risks associated with scooping, transferring, or handling ice manually. Built-in water filtration systems remove sediment, chlorine, minerals, and other impurities before water enters the freezing chamber, ensuring that only purified water becomes ice. This filtration proves especially valuable in areas with questionable water quality, as the machine compensates for municipal supply inconsistencies. Regular sanitization becomes straightforward thanks to accessible components and smooth surfaces that allow thorough cleaning without disassembly. Many ice cube industrial machines feature automatic cleaning cycles that flush the system with sanitizing solutions, reducing labor requirements while ensuring consistent hygiene standards. The enclosed storage bins maintain ice in sanitary conditions, protected from environmental contaminants until dispensing. Temperature monitoring prevents ice from melting and refreezing, a cycle that can concentrate impurities and create food safety hazards. Compliance with health department regulations becomes effortless, as these machines meet or exceed standards established by food safety authorities. Documentation capabilities in advanced models provide production logs and temperature records that satisfy inspection requirements and demonstrate due diligence. The peace of mind that comes from knowing your ice meets the highest sanitation standards protects your business reputation and customer health. This hygiene advantage proves particularly crucial for healthcare facilities, where compromised ice could pose serious risks to vulnerable patients. The investment in an ice cube industrial machine represents a commitment to food safety that customers recognize and appreciate, differentiating your establishment from competitors who may cut corners on this essential aspect of service quality.
Long-Term Cost Savings and Operational Independence

Long-Term Cost Savings and Operational Independence

The financial benefits of owning an ice cube industrial machine extend far beyond the initial purchase, creating substantial long-term savings that transform operational economics. Eliminating recurring supplier costs represents the most obvious advantage, as businesses no longer pay markup prices for bagged ice or scheduled deliveries. These ongoing expenses accumulate rapidly, especially for high-volume operations where daily ice purchases can reach hundreds of dollars. The ice cube industrial machine converts this recurring cost into a one-time capital investment that pays dividends for years. Energy costs remain surprisingly modest, as efficient refrigeration systems and optimized production cycles minimize power consumption relative to output volume. Modern units incorporate variable-speed compressors that adjust operation intensity based on demand, reducing energy waste during slower periods. The independence from external suppliers eliminates vulnerability to price increases, supply shortages, or delivery disruptions that can cripple operations during peak seasons. This autonomy proves invaluable during emergencies, holidays, or unexpected demand surges when supplier availability becomes unreliable. Maintenance expenses stay predictable and manageable, with most machines requiring only routine cleaning, filter replacements, and occasional component servicing. The durability of industrial-grade construction means these machines operate reliably for decades with proper care, spreading the initial investment across an extended service life. Reduced labor costs compound the savings, as staff no longer spend time managing ice inventory, coordinating deliveries, or manually producing ice. The time savings allow employees to focus on revenue-generating activities rather than logistical tasks. Storage space previously dedicated to bagged ice becomes available for other purposes, improving facility utilization and potentially eliminating the need for additional storage areas. The ability to produce ice on demand eliminates waste from melted or unused ice, as you generate only what you need when you need it. This precision prevents the financial loss associated with over-ordering from suppliers or disposing of excess inventory. Tax benefits may apply to the equipment purchase, as capital investments often qualify for depreciation deductions or business expense write-offs. The professional image conveyed by owning production equipment rather than relying on retail ice bags enhances business credibility with customers and partners. Insurance costs may decrease as well, since eliminating delivery truck traffic reduces liability exposure. The cumulative effect of these savings creates a compelling financial case that justifies the initial investment many times over, making an ice cube industrial machine one of the most cost-effective equipment purchases a business can make.


Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000