Advanced Technology for Superior Ice Quality and Consistency
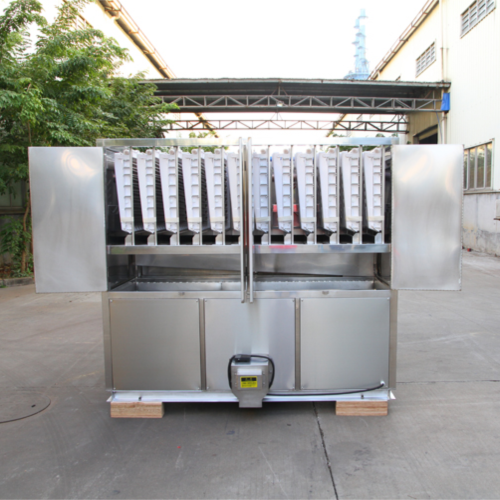
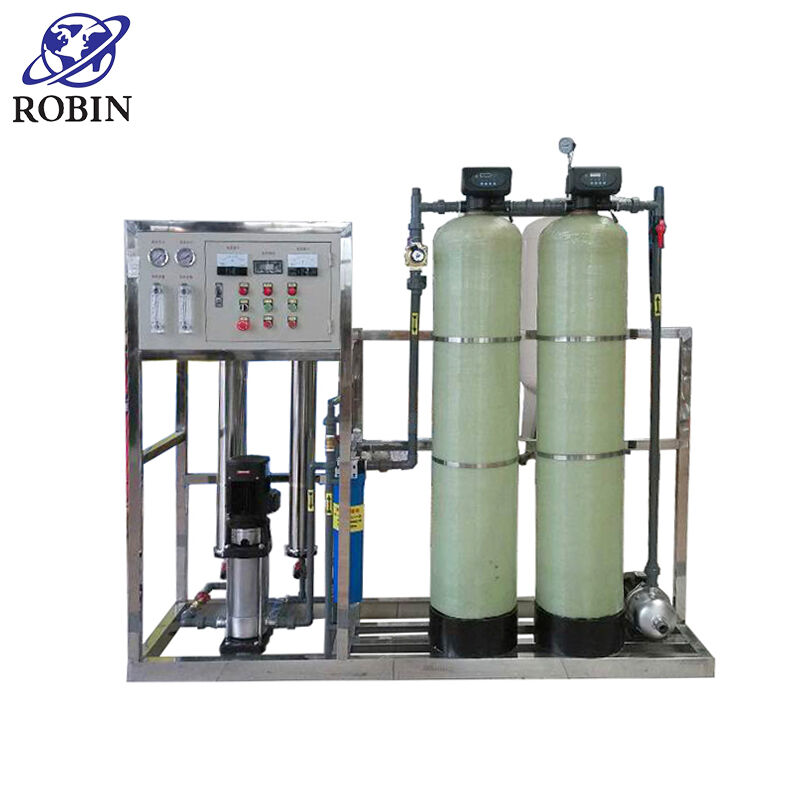
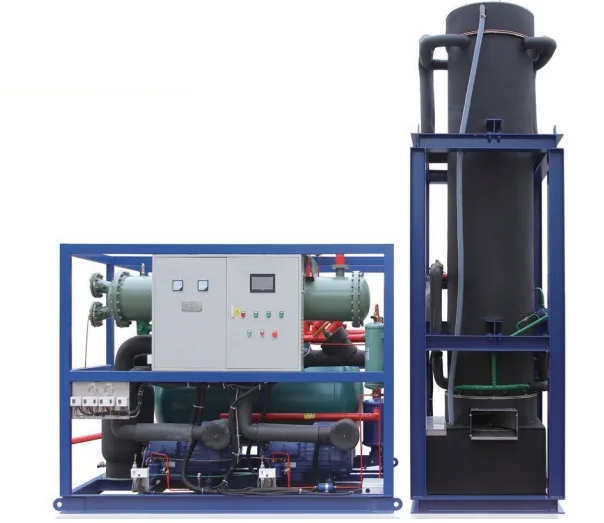
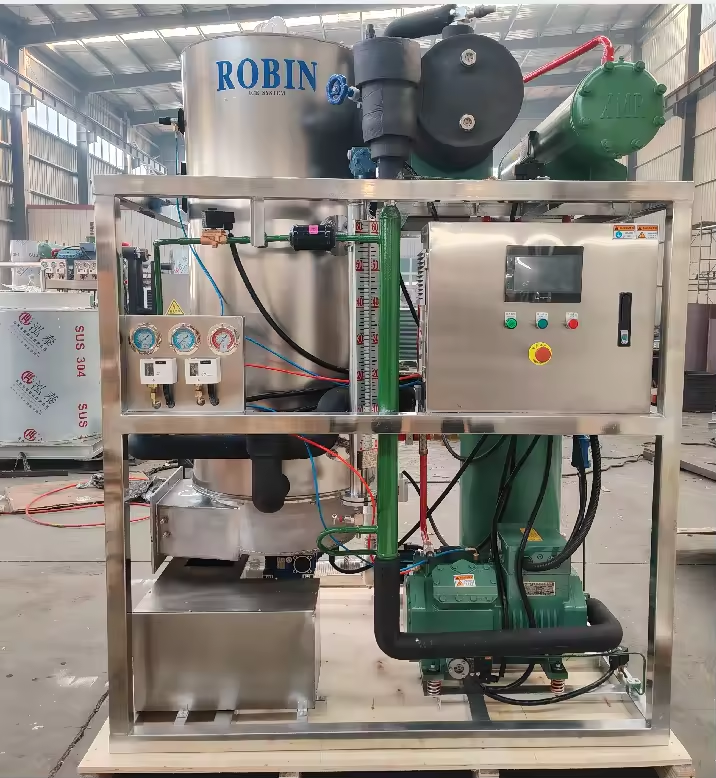
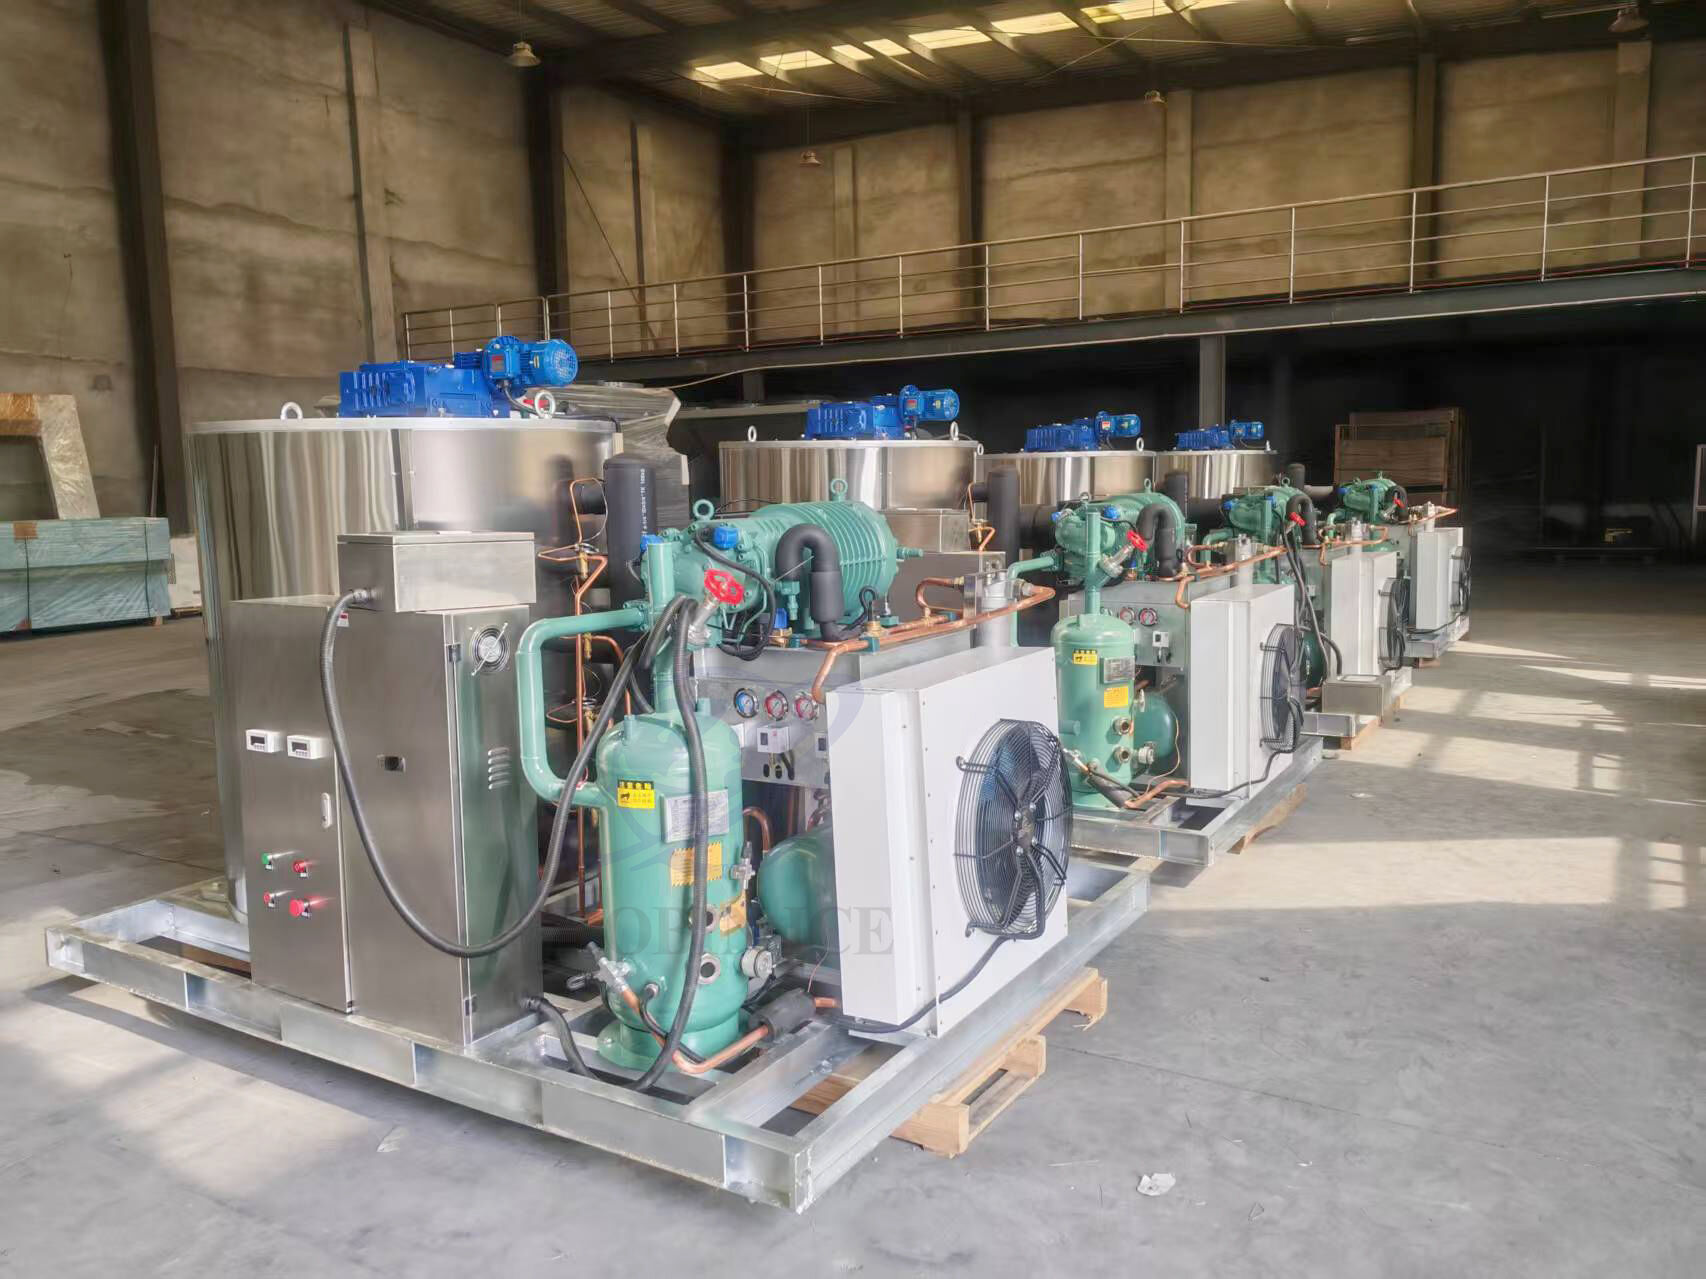
The technological sophistication embedded in modern wholesale industrial ice machines directly impacts the quality and consistency of ice production, factors that significantly influence customer experience and operational efficiency. Advanced refrigeration systems utilize precision-engineered compressors and evaporators that maintain exact temperature control throughout the freezing process, resulting in ice that is harder, clearer, and slower-melting than ice produced by basic equipment. This superior ice quality matters tremendously in beverage service, where cloudy or soft ice dilutes drinks quickly and diminishes presentation appeal. Clear, dense ice from a wholesale industrial ice machine keeps beverages colder longer, enhances visual appeal, and demonstrates attention to quality that customers notice and appreciate. The consistency achieved by wholesale industrial ice machines eliminates the variability that plagues inferior equipment. Every ice cube, flake, or nugget meets the same size and density specifications, batch after batch, day after day. This uniformity is crucial for businesses that depend on precise portioning, such as healthcare facilities measuring therapeutic ice applications or food processors calculating cooling requirements for perishable products. Consistent ice production also simplifies inventory management and usage forecasting, allowing you to predict supply needs accurately and avoid both shortages and excess that leads to waste. Water filtration technology integrated into wholesale industrial ice machines represents another critical quality advantage. Multi-stage filtration systems remove chlorine, minerals, sediments, and other impurities that affect ice taste, clarity, and machine performance. Clean water input produces better-tasting ice that does not impart off-flavors to beverages or foods. Additionally, filtered water reduces mineral buildup inside the machine, extending component life and reducing maintenance frequency. Some advanced wholesale industrial ice machines include antimicrobial filtration that actively inhibits bacterial growth, providing an extra layer of food safety protection. Smart technology features in contemporary wholesale industrial ice machines provide unprecedented control and monitoring capabilities. Digital displays show real-time production status, ice bin levels, and system diagnostics at a glance. Programmable settings allow you to adjust production schedules to match demand patterns, reducing energy consumption during slow periods while ensuring adequate supply during peak times. Remote connectivity enables managers to monitor multiple machines across different locations from a single interface, receiving instant alerts about maintenance needs or operational issues before they impact service. This technological integration transforms ice production from a passive background function into an actively managed component of your operational strategy, delivering measurable improvements in efficiency, quality, and cost control.

 EN