Leading Tube Ice Machine Manufacturers: Advanced Technology, Hygienic Design & Scalable Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

tube ice machine manufacturers

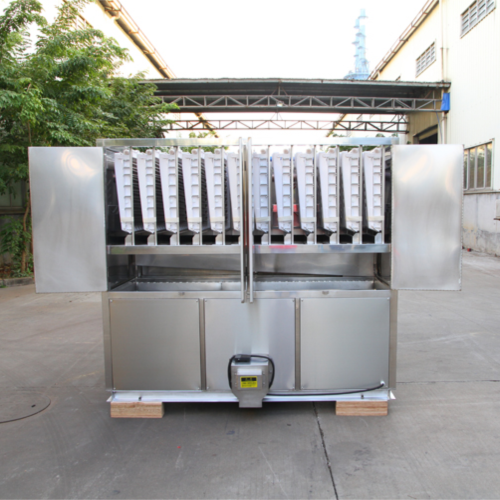
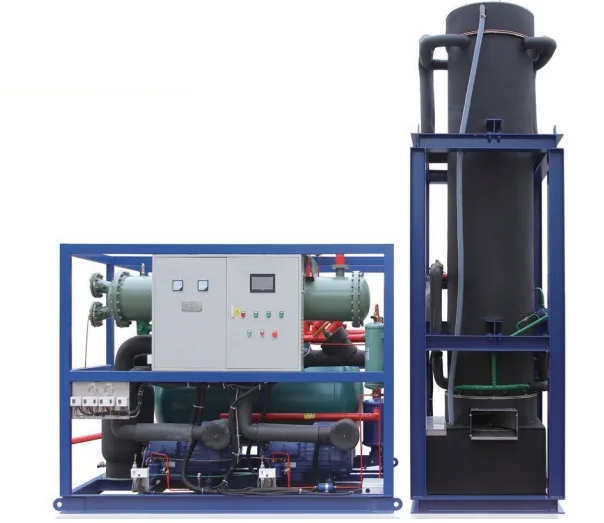
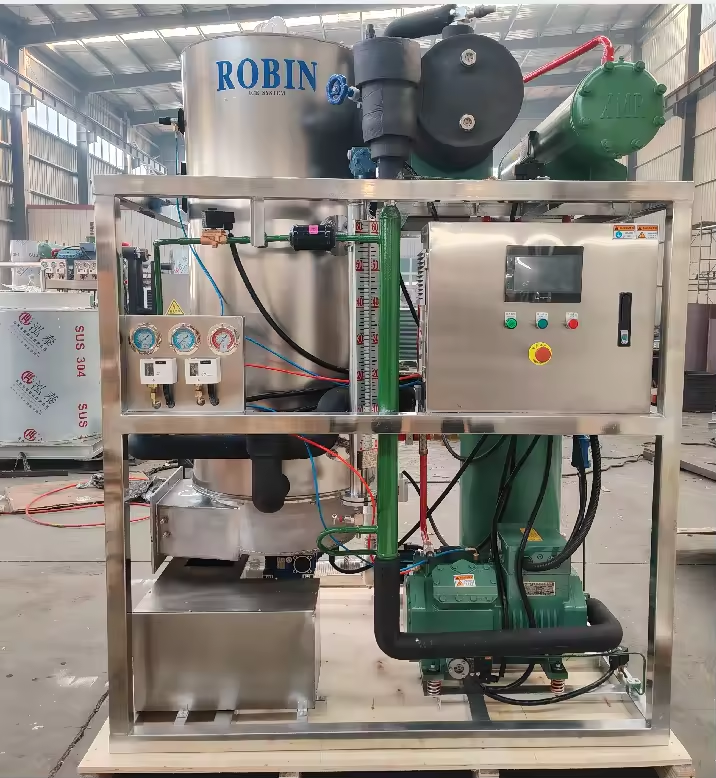
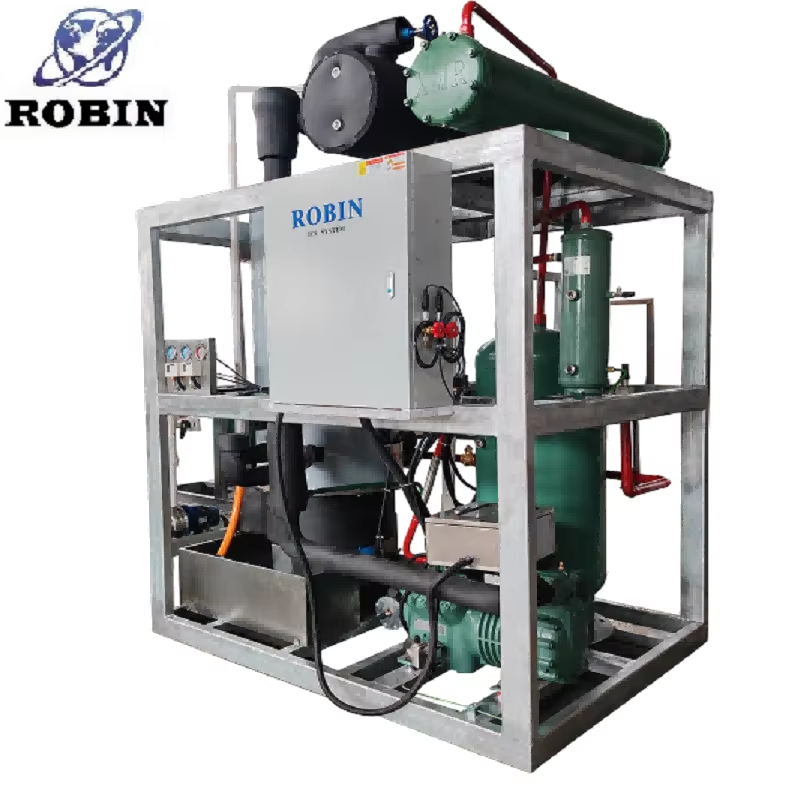
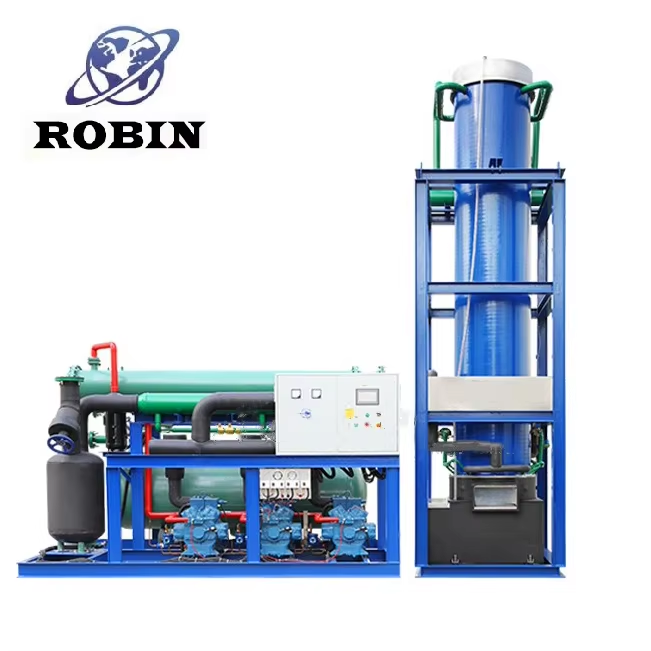
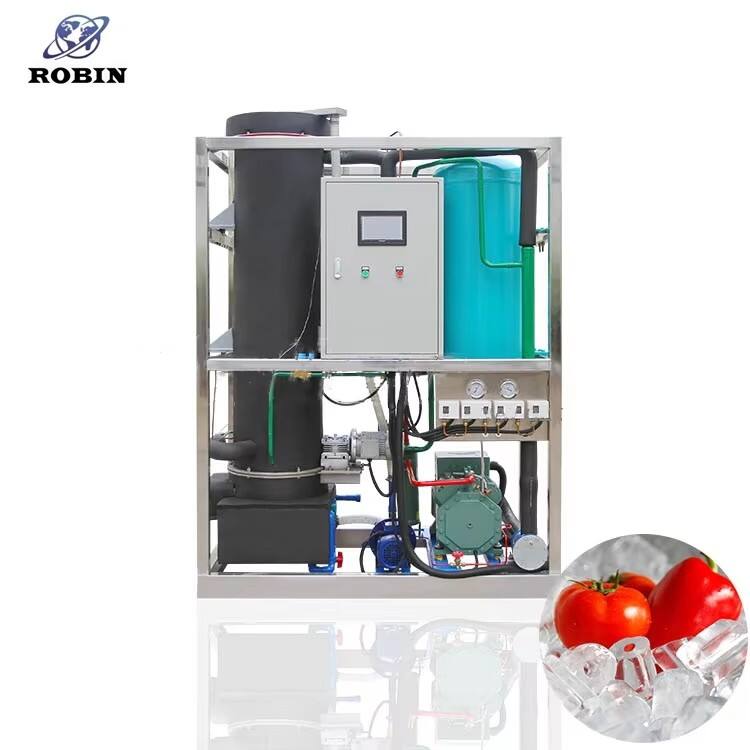
Tube ice machine manufacturers represent a specialized sector within the industrial refrigeration industry, dedicated to producing equipment that creates cylindrical ice with hollow centers. These manufacturers design and build machines capable of generating tube ice in various sizes, typically ranging from 20mm to 50mm in diameter and 25mm to 60mm in length. The primary function of these machines involves freezing water inside vertical evaporator tubes, where refrigerant circulates around the exterior, causing ice to form on the inner walls. Once the ice reaches the desired thickness, a hot gas defrost cycle releases the tubes, allowing them to fall into storage bins below. Tube ice machine manufacturers incorporate advanced refrigeration technology, utilizing high-efficiency compressors, precision-engineered evaporators, and automated control systems that monitor ice production cycles. The technological features embedded in these machines include microprocessor-based controllers that regulate ice thickness, production capacity adjustments, and energy consumption optimization. Many tube ice machine manufacturers now integrate smart monitoring systems that provide real-time data on machine performance, maintenance alerts, and remote diagnostics capabilities. The applications for tube ice produced by these manufacturers span numerous industries, including food processing facilities that require ice for cooling seafood, poultry, and produce during transportation and storage. Beverage industries rely on tube ice for drink cooling and display purposes, while concrete cooling operations use it to control temperature during large-scale construction projects in hot climates. Chemical processing plants employ tube ice for temperature regulation in various reactions, and the healthcare sector utilizes it for therapeutic applications and laboratory processes. Tube ice machine manufacturers serve both commercial and industrial markets, offering equipment with production capacities ranging from small-scale units producing 1 ton per day to large industrial systems capable of generating over 30 tons daily. The versatility of tube ice makes it particularly valuable because its hollow center allows for rapid cooling and easy handling, while its hard texture ensures slower melting rates compared to other ice forms.

New Product Releases

Choosing the right tube ice machine manufacturers brings substantial benefits that directly impact your operational efficiency and bottom line. First, reputable manufacturers deliver machines built with superior engineering that ensures consistent ice quality day after day. You get uniform tube ice with predictable dimensions, which matters when your processes depend on standardized cooling performance. The reliability factor cannot be overstated because downtime in ice production translates to lost revenue and disrupted operations. Established tube ice machine manufacturers use proven components and rigorous testing protocols, resulting in equipment that runs continuously with minimal interruptions. Energy efficiency stands as another major advantage, as leading manufacturers invest in research to reduce power consumption without sacrificing output. Modern tube ice machines incorporate variable-speed compressors, optimized refrigerant circuits, and intelligent defrost cycles that cut electricity costs by 20 to 30 percent compared to older models. This efficiency translates to lower operating expenses over the machine's lifespan, often recovering the initial investment within a few years. The ease of maintenance represents a practical benefit that busy operators appreciate. Quality manufacturers design their machines with accessible components, clear service points, and straightforward maintenance procedures that your staff can handle without specialized training. This accessibility reduces service costs and minimizes the time machines spend offline for routine maintenance. Hygiene and food safety compliance come standard with reputable tube ice machine manufacturers who understand regulatory requirements across different markets. Their machines feature stainless steel construction in food-contact areas, smooth surfaces that prevent bacterial growth, and designs that facilitate thorough cleaning. Scalability offers another advantage, as established manufacturers provide a range of models that grow with your business. You can start with a smaller unit and expand capacity by adding machines or upgrading to larger models, knowing that parts availability and service support remain consistent. Technical support and after-sales service distinguish quality manufacturers from budget alternatives. You gain access to experienced technicians who understand your specific model, readily available spare parts that arrive quickly when needed, and comprehensive warranties that protect your investment. Training programs offered by leading tube ice machine manufacturers ensure your operators understand proper machine operation, troubleshooting basics, and maintenance schedules. Customization capabilities allow manufacturers to adapt standard designs to your specific requirements, whether that involves different ice sizes, special voltage configurations, or integration with existing refrigeration systems. The durability of machines from established manufacturers means you avoid frequent replacements and enjoy stable production for 10 to 15 years or more with proper maintenance. Finally, working with recognized tube ice machine manufacturers provides peace of mind through their track record, customer references, and proven performance in demanding industrial environments.

Practical Tips

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

12

May

How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

In food processing, healthcare, fisheries, and beverage production, the integrity of ice directly affects product safety and regulatory compliance. A tube ice maker machine is engineered from the ground up to meet the demanding hygiene standards that...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

tube ice machine manufacturers

Advanced Refrigeration Technology and Energy Optimization

Advanced Refrigeration Technology and Energy Optimization

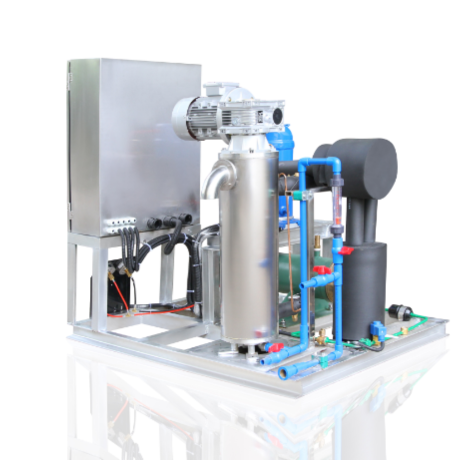
Tube ice machine manufacturers have revolutionized ice production through sophisticated refrigeration technology that maximizes efficiency while minimizing environmental impact. At the core of these advancements lies the integration of variable-speed compressor technology, which adjusts cooling capacity based on actual demand rather than running at full power continuously. This intelligent approach reduces energy consumption during periods of lower ice demand and prevents the wasteful cycling that plagues fixed-speed systems. The evaporator design represents another area where tube ice machine manufacturers have achieved significant breakthroughs. Modern evaporators feature enhanced heat transfer surfaces with optimized tube spacing and refrigerant distribution systems that ensure uniform ice formation across all tubes. This uniformity eliminates the problem of some tubes producing thicker ice while others remain thin, which previously caused inefficient defrost cycles and wasted energy. Leading manufacturers now employ advanced refrigerants with lower global warming potential, responding to environmental regulations while maintaining excellent thermodynamic properties. The control systems developed by innovative tube ice machine manufacturers incorporate predictive algorithms that learn your usage patterns and adjust production schedules accordingly. These systems can ramp up production before peak demand periods and reduce output during slower times, ensuring you always have sufficient ice without overproduction. The defrost cycle optimization deserves special attention because it directly impacts both ice quality and energy consumption. Traditional systems used fixed-duration defrost cycles regardless of actual ice thickness, wasting energy when ice was thin and failing to release ice when it was thick. Modern tube ice machine manufacturers implement sensor-based defrost systems that detect actual ice thickness and terminate the defrost cycle precisely when tubes release, saving energy and improving ice consistency. Heat recovery systems represent another innovation where manufacturers capture waste heat from the refrigeration process and redirect it for useful purposes such as preheating incoming water or space heating in cold climates. This approach improves overall system efficiency by 15 to 25 percent in suitable applications. The insulation technology used by quality manufacturers has also evolved, with vacuum-insulated panels and advanced foam materials that dramatically reduce heat gain in ice storage bins and machine compartments. This superior insulation keeps ice frozen longer and reduces the cooling load on the refrigeration system. Monitoring and diagnostic capabilities built into modern machines allow operators to track energy consumption in real-time, identify inefficiencies, and schedule maintenance before minor issues become major problems. Remote connectivity enables manufacturers to provide proactive support, analyzing machine performance data and recommending adjustments that optimize efficiency for your specific operating conditions.
Hygienic Design and Food Safety Compliance

Hygienic Design and Food Safety Compliance

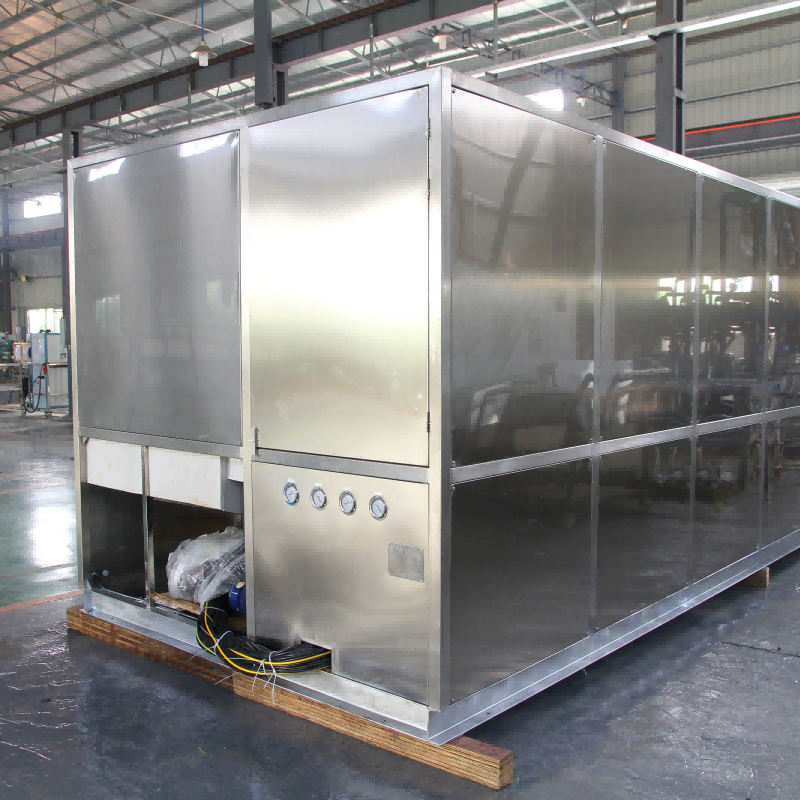
The commitment of tube ice machine manufacturers to hygienic design and food safety compliance addresses one of the most critical concerns for businesses in food service, healthcare, and other sensitive applications. Understanding that ice is a food product that comes into direct contact with consumables, leading manufacturers have developed comprehensive approaches to ensure their machines meet or exceed international food safety standards. The material selection process begins with food-grade stainless steel for all surfaces that contact water or ice, specifically 304 or 316 stainless steel grades that resist corrosion and prevent metallic contamination. Tube ice machine manufacturers carefully design water circuits to eliminate dead legs where stagnant water could harbor bacteria, implementing continuous flow patterns that keep water moving and fresh. The evaporator tubes themselves receive special attention, with smooth interior surfaces that prevent biofilm formation and facilitate effective cleaning. Many manufacturers now offer antimicrobial coatings on critical surfaces, using silver-ion technology or other approved treatments that inhibit bacterial growth without introducing harmful chemicals into the ice. The water filtration systems integrated by quality tube ice machine manufacturers remove sediment, chlorine, and microorganisms before water enters the freezing process, ensuring that only pure water becomes ice. Multi-stage filtration with sediment filters, activated carbon, and ultraviolet sterilization provides comprehensive water treatment that meets stringent food safety requirements. Drainage systems in modern machines prevent water accumulation and cross-contamination, with properly sloped surfaces and sealed connections that eliminate potential contamination pathways. The air intake and ventilation design prevents airborne contaminants from entering the ice production area, with filtered air supplies and positive pressure systems in critical zones. Tube ice machine manufacturers design their equipment for easy cleaning and sanitization, with removable panels, accessible interior surfaces, and smooth transitions that eliminate hard-to-clean crevices. Automated cleaning cycles available in advanced models circulate sanitizing solutions through the water system on programmed schedules, reducing manual labor and ensuring consistent sanitation. Documentation and traceability features built into modern control systems record production parameters, cleaning cycles, and maintenance activities, providing the audit trail required by food safety regulations and quality management systems. Certification from recognized bodies such as NSF International, CE marking for European markets, and compliance with FDA regulations demonstrates that tube ice machine manufacturers take food safety seriously. Training materials and operational guidelines provided by manufacturers help your staff understand proper hygiene practices, from hand washing protocols to ice handling procedures that maintain product integrity from production to end use. The investment in hygienic design by reputable tube ice machine manufacturers protects your brand reputation, reduces liability risks, and ensures that your ice meets the expectations of health-conscious consumers and regulatory inspectors.
Scalable Production Capacity and Operational Flexibility

Scalable Production Capacity and Operational Flexibility

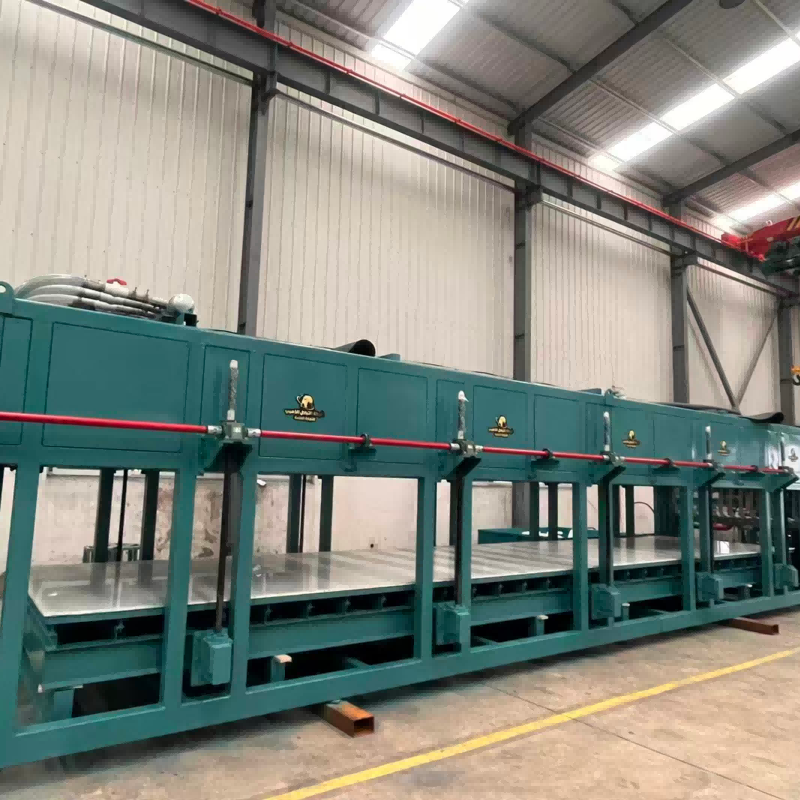
Tube ice machine manufacturers recognize that businesses have diverse and evolving ice production needs, which is why they offer scalable solutions and operational flexibility that adapt to changing requirements. The modular approach adopted by forward-thinking manufacturers allows you to start with a production capacity that matches your current demand and expand seamlessly as your business grows. This scalability eliminates the dilemma of either over-investing in excessive capacity upfront or outgrowing your equipment too quickly and facing costly replacements. Tube ice machine manufacturers design their equipment with standardized interfaces and compatible components, enabling you to add additional machines that integrate smoothly with existing installations. The production capacity range available from established manufacturers spans from compact units suitable for restaurants and small food processors producing 1 to 3 tons daily, up to industrial-scale systems for large fishing operations, concrete plants, and chemical facilities requiring 20 to 30 tons or more per day. This variety ensures that tube ice machine manufacturers can match equipment to your specific volume requirements without forcing you into ill-fitting solutions. The flexibility extends to ice size customization, with manufacturers offering different evaporator configurations that produce tubes ranging from small 20mm diameter pieces ideal for beverage cooling to large 50mm tubes preferred for concrete cooling and bulk food preservation. Operational flexibility manifests in the ability to adjust production schedules based on demand patterns, with programmable controllers that automatically increase output during peak periods and reduce production during off-hours to save energy. Some tube ice machine manufacturers offer dual-capacity systems that can switch between different production modes, providing maximum output when needed and economy mode during slower periods. The installation flexibility provided by quality manufacturers accommodates various facility constraints, with options for indoor or outdoor installation, different voltage and phase configurations, and cooling methods including air-cooled, water-cooled, or evaporative-cooled condensers suited to your climate and water availability. Tube ice machine manufacturers also address the challenge of seasonal demand fluctuations common in many industries, designing machines that maintain efficiency across a wide range of ambient temperatures and production loads. The storage integration options offered by manufacturers include insulated bins of various sizes, automated ice delivery systems, and packaging equipment that prepares ice for distribution. Remote monitoring and control capabilities available from advanced tube ice machine manufacturers provide operational flexibility by allowing you to manage multiple machines across different locations from a central interface, adjusting settings, monitoring performance, and responding to alerts without physical presence at each site. Maintenance flexibility comes through modular component design that enables quick replacement of parts without dismantling entire systems, minimizing downtime and allowing maintenance during convenient windows rather than forcing extended shutdowns. The financial flexibility offered by established tube ice machine manufacturers includes various purchasing options, leasing programs, and performance guarantees that align equipment acquisition with your budget and cash flow requirements.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000