Large Cube Ice Maker Manufacturer: Commercial Ice Equipment Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

large cube ice maker manufacturer

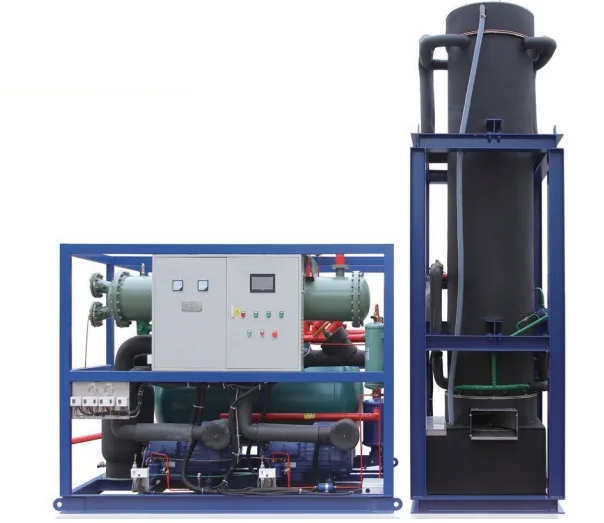
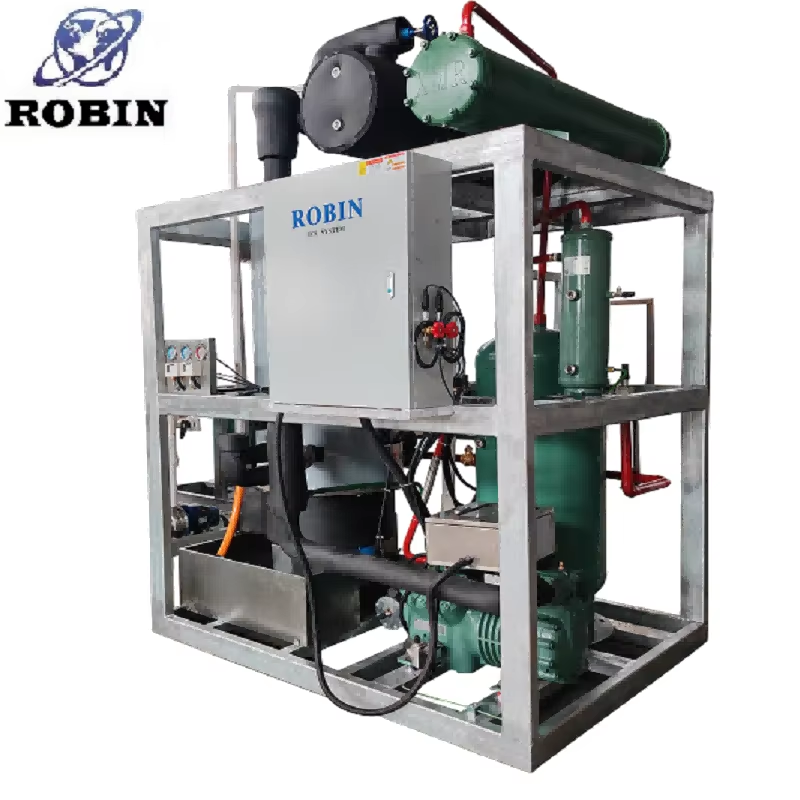
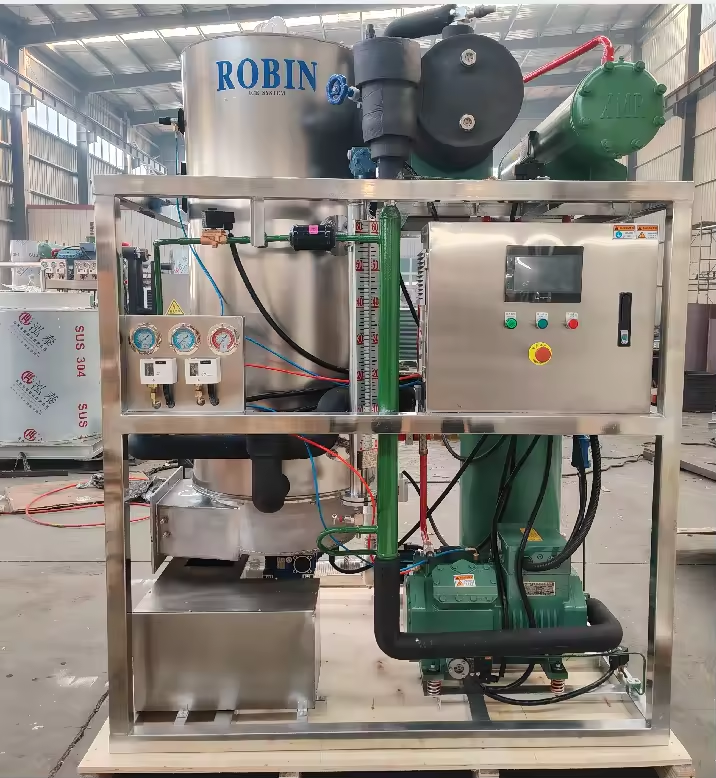
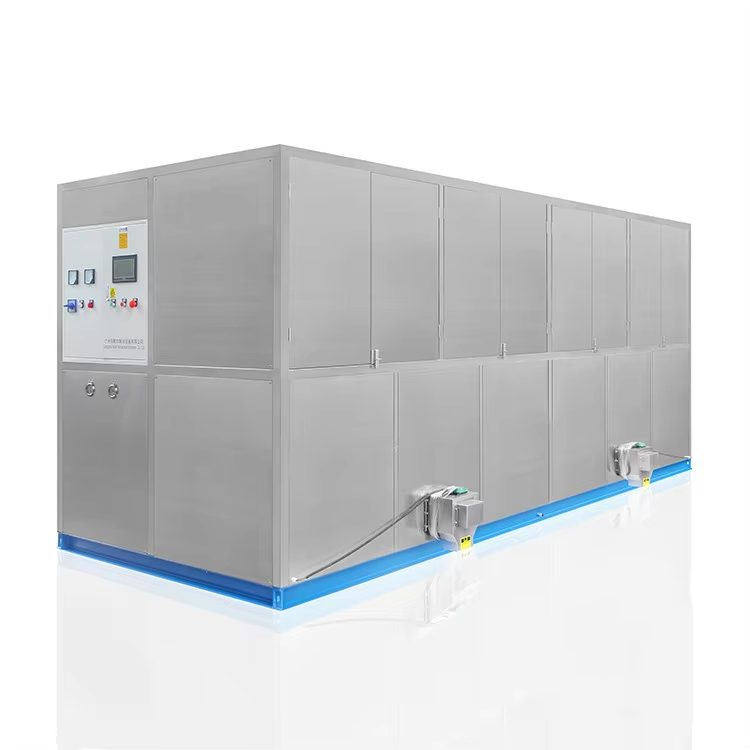
A large cube ice maker manufacturer specializes in producing industrial-grade ice machines designed to create substantial, perfectly formed ice cubes for commercial and hospitality applications. These manufacturers engineer sophisticated refrigeration systems that deliver consistent ice production at scale, meeting the demanding requirements of restaurants, bars, hotels, catering services, and entertainment venues. The primary function of equipment from a large cube ice maker manufacturer centers on transforming purified water into dense, slow-melting ice cubes through precision freezing technology. Modern large cube ice maker manufacturer facilities incorporate advanced control systems that monitor water quality, freezing cycles, and production output to ensure optimal performance. The technological features embedded in products from a large cube ice maker manufacturer include programmable logic controllers, energy-efficient compressors, antimicrobial surfaces, and intelligent diagnostic systems that predict maintenance needs before failures occur. These machines typically produce ice cubes ranging from 1.5 to 2.5 inches, ideal for premium beverage service where dilution control matters. Applications span diverse sectors including fine dining establishments requiring crystal-clear ice for cocktails, healthcare facilities needing sanitary ice for patient care, seafood markets using ice for product preservation, and event venues serving thousands of guests. A reputable large cube ice maker manufacturer invests heavily in research and development to improve freezing efficiency, reduce water waste, and minimize energy consumption. The manufacturing process involves precision metalworking, food-grade material selection, and rigorous quality testing to meet international safety standards. Distribution networks established by a large cube ice maker manufacturer ensure timely delivery, installation support, and ongoing technical assistance. The competitive landscape drives innovation, with leading manufacturers differentiating through build quality, production capacity, and after-sales service. Businesses partnering with an established large cube ice maker manufacturer gain access to reliable equipment that operates continuously under demanding conditions while maintaining ice quality standards essential for customer satisfaction and operational efficiency.

Popular Products

Choosing equipment from a large cube ice maker manufacturer delivers tangible benefits that directly impact your bottom line and operational efficiency. First, production capacity stands as a primary advantage, with industrial units generating between 500 and 3000 pounds of ice daily, eliminating the constant worry about running short during peak service hours. This reliable output means your staff focuses on serving customers rather than managing ice shortages or making emergency supply runs. Energy efficiency represents another significant benefit, as modern units from a quality large cube ice maker manufacturer consume 30 to 40 percent less electricity than older models through improved insulation, variable-speed compressors, and optimized refrigeration cycles. These savings accumulate substantially over the equipment's 10 to 15 year lifespan, often recovering the initial investment through reduced utility bills alone. Durability proves essential in commercial environments, and products from an established large cube ice maker manufacturer feature stainless steel construction, corrosion-resistant components, and reinforced internal mechanisms that withstand constant use without frequent breakdowns. This reliability translates to fewer service calls, reduced downtime, and lower maintenance costs compared to consumer-grade alternatives. Ice quality itself provides a competitive edge, as large cubes melt slower than smaller formats, preserving beverage flavor profiles and reducing dilution complaints from discerning customers. The crystal-clear appearance of properly produced large cubes enhances drink presentation, contributing to perceived value and justifying premium pricing. Sanitation features built into equipment from a responsible large cube ice maker manufacturer include antimicrobial bin liners, self-cleaning cycles, and accessible components that simplify daily cleaning protocols, helping you maintain health code compliance effortlessly. Installation flexibility accommodates various space configurations, with modular designs allowing placement in kitchens, bars, or dedicated ice rooms depending on your facility layout. User-friendly controls minimize training requirements, enabling new staff to operate the equipment confidently after brief instruction. Diagnostic displays alert operators to potential issues before they escalate into costly repairs, supporting proactive maintenance scheduling. Warranty coverage from a reputable large cube ice maker manufacturer typically spans three to five years on major components, providing financial protection and demonstrating manufacturer confidence in product longevity. Technical support networks ensure rapid response when questions arise, with many manufacturers offering 24/7 helplines and extensive online resources. Scalability allows businesses to start with one unit and expand capacity as demand grows, with compatible models that integrate seamlessly into existing setups. Environmental responsibility increasingly matters to consumers and regulators, and leading manufacturers prioritize refrigerants with low global warming potential, water-saving technologies, and recyclable materials in construction. These advantages combine to create a compelling value proposition that extends far beyond the initial purchase price, supporting business growth and customer satisfaction for years.

Tips And Tricks

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

04

May

Can Ice Tube Machine Improve Cooling Efficiency in Industrial Operations?

Industrial cooling is one of the most operationally critical and cost-sensitive challenges across manufacturing, food processing, chemical production, and logistics. When facilities struggle with inconsistent temperature control, product spoilage, or...
View More
Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

08

May

Is Tube Ice Maker Machine Suitable for High-Capacity Ice Manufacturing?

When industrial buyers and plant managers evaluate large-scale ice production systems, one question consistently surfaces: is a tube ice maker machine genuinely capable of meeting high-capacity manufacturing demands? The answer is not simply yes or n...
View More
How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

12

May

How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

In food processing, healthcare, fisheries, and beverage production, the integrity of ice directly affects product safety and regulatory compliance. A tube ice maker machine is engineered from the ground up to meet the demanding hygiene standards that...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

large cube ice maker manufacturer

Advanced Refrigeration Technology for Consistent Performance

Advanced Refrigeration Technology for Consistent Performance

The refrigeration systems engineered by a leading large cube ice maker manufacturer represent the culmination of decades of thermodynamic research and practical application refinement. At the core of these systems lies a precisely calibrated refrigeration cycle that removes heat from water at controlled rates, ensuring uniform ice formation across every production batch. Unlike residential ice makers that produce inconsistent results, commercial equipment from a specialized large cube ice maker manufacturer employs industrial-grade compressors rated for continuous operation, capable of maintaining optimal temperatures even in hot kitchen environments where ambient temperatures regularly exceed 90 degrees Fahrenheit. The evaporator design proves critical to ice quality, with manufacturers utilizing copper or stainless steel coils configured to promote even freezing patterns that eliminate air bubbles and impurities, resulting in the crystal-clear cubes that premium establishments demand. Temperature sensors positioned throughout the freezing chamber provide real-time data to microprocessor controllers, which adjust compressor speed, refrigerant flow, and harvest timing to compensate for variables like incoming water temperature and ambient conditions. This intelligent control system, a hallmark of sophisticated equipment from a quality large cube ice maker manufacturer, optimizes energy consumption by running components only as hard as necessary to maintain production targets, rather than operating at full capacity constantly. The harvest cycle demonstrates particular engineering elegance, as the system briefly reverses refrigerant flow to warm the evaporator surface just enough to release finished cubes without melting them, a process timed to the second for maximum efficiency. Insulation technology has advanced significantly, with modern units from a forward-thinking large cube ice maker manufacturer incorporating vacuum-insulated panels and thermal breaks that minimize heat transfer, keeping ice frozen longer in storage bins while reducing the workload on refrigeration components. Refrigerant selection reflects environmental consciousness, with manufacturers transitioning to R-290 and other natural refrigerants that deliver excellent thermodynamic performance without the ozone depletion and high global warming potential of legacy compounds. The condenser system, whether air-cooled or water-cooled, receives equal engineering attention, with designs that maximize heat rejection efficiency while minimizing maintenance requirements through accessible coil configurations and self-cleaning features. Reliability engineering ensures these complex systems operate for years between service intervals, with manufacturers conducting accelerated life testing that simulates years of operation in compressed timeframes, identifying and eliminating potential failure points before products reach customers. This technological sophistication, invisible to end users but fundamental to performance, distinguishes equipment from a serious large cube ice maker manufacturer from cheaper alternatives that compromise on components and engineering rigor.
Hygienic Design Standards for Food Safety Compliance

Hygienic Design Standards for Food Safety Compliance

Food safety regulations grow stricter annually, and equipment from a responsible large cube ice maker manufacturer incorporates hygienic design principles that help operators maintain compliance effortlessly while protecting public health. The concept of hygienic design extends beyond simple cleanability to encompass material selection, surface finish quality, drainage characteristics, and accessibility for inspection and maintenance. Stainless steel dominates construction in quality units, specifically food-grade 304 or 316 alloys that resist corrosion, withstand repeated sanitizer exposure, and provide non-porous surfaces where bacteria cannot colonize. A reputable large cube ice maker manufacturer specifies these materials not just for customer-facing surfaces but throughout the water pathway, ensuring every component contacting water or ice meets food contact standards. Surface finishes receive careful attention, with manufacturers polishing stainless steel to specific roughness values that prevent biofilm formation while remaining practical to clean during daily operations. Corners and joints, notorious harboring points for contamination, are either eliminated through seamless construction techniques or designed with generous radii that cleaning tools can reach effectively. The water distribution system in equipment from a quality large cube ice maker manufacturer features removable components that operators can disassemble, inspect, and sanitize without tools, supporting thorough cleaning protocols that health inspectors appreciate. Antimicrobial treatments applied to ice contact surfaces provide an additional safety layer, with silver-ion technology or other EPA-registered treatments that inhibit microbial growth between cleaning cycles. Drainage systems incorporate air gaps and backflow prevention to ensure wastewater never contaminates the potable water supply, a critical safety feature that inferior manufacturers sometimes overlook. Storage bin design reflects hygienic priorities, with sloped floors that direct meltwater to drains rather than allowing it to pool, and removable doors that facilitate complete interior access for cleaning and inspection. Air filtration systems protect ice from airborne contaminants, with replaceable filters capturing dust, grease particles, and other pollutants before they enter the freezing chamber. A forward-thinking large cube ice maker manufacturer provides detailed cleaning instructions and schedules based on actual usage patterns and environmental conditions, moving beyond generic recommendations to actionable guidance. Self-diagnostic systems monitor water quality parameters and alert operators when filtration systems require service or when bacterial counts suggest cleaning intervals should be shortened. Compliance documentation matters to health departments, and manufacturers supply specification sheets, material certifications, and test reports that demonstrate conformance with NSF, UL, and other relevant standards. Training resources help staff understand not just how to clean equipment but why specific procedures matter, fostering a culture of food safety that extends beyond mere regulatory compliance. The investment in hygienic design by a serious large cube ice maker manufacturer protects businesses from the devastating consequences of foodborne illness outbreaks, including legal liability, reputation damage, and potential closure, making it an essential consideration rather than an optional feature.
Operational Efficiency and Total Cost of Ownership Benefits

Operational Efficiency and Total Cost of Ownership Benefits

The true value of equipment from an established large cube ice maker manufacturer emerges when examining total cost of ownership rather than focusing solely on purchase price. Operational efficiency begins with energy consumption, where modern units achieve remarkable performance through variable-speed compressors that adjust output to match demand rather than cycling on and off repeatedly, a pattern that wastes energy and stresses components. Heat recovery systems, available on advanced models from innovative manufacturers, capture waste heat from the refrigeration process and redirect it to preheat incoming water or supplement space heating, effectively extracting useful work from energy that would otherwise dissipate into the environment. Water efficiency matters increasingly as utility costs rise and environmental regulations tighten, with leading equipment from a responsible large cube ice maker manufacturer incorporating recirculation systems that reuse water from the final rinse cycle for initial flushing in subsequent batches, reducing consumption by 20 to 30 percent compared to single-pass designs. Production scheduling capabilities allow operators to concentrate ice making during off-peak utility hours when electricity rates drop, with sufficient storage capacity to meet daytime demand from overnight production, a strategy that can reduce energy costs by 40 percent in markets with time-of-use pricing. Maintenance costs factor significantly into ownership economics, and equipment from a quality large cube ice maker manufacturer features modular component design that allows technicians to replace failed parts quickly without extensive disassembly, minimizing labor charges and downtime. Predictive maintenance systems monitor vibration signatures, temperature differentials, and cycle times to identify developing problems before they cause failures, enabling scheduled repairs during slow periods rather than emergency service calls during peak business hours. Parts availability distinguishes established manufacturers from newcomers, with comprehensive inventories, rapid shipping networks, and backward compatibility that ensures components remain available throughout the equipment's service life. Training programs offered by a committed large cube ice maker manufacturer equip in-house maintenance staff with troubleshooting skills and routine service capabilities, reducing dependence on external technicians for minor issues. Energy monitoring features provide granular data on consumption patterns, helping operators identify inefficiencies and optimize settings for their specific usage profiles. The longevity of commercial equipment from a reputable manufacturer typically exceeds 15 years with proper maintenance, compared to 5 to 7 years for consumer-grade alternatives, spreading the capital investment across more years of productive service. Resale value remains higher for recognized brands, providing exit value if business needs change or equipment upgrades become desirable. Financing options through manufacturer partnerships or leasing programs make acquisition more accessible, with payment structures that align with cash flow patterns rather than requiring large upfront capital outlays. Utility rebate programs frequently apply to energy-efficient models from qualifying manufacturers, with some businesses recovering 10 to 20 percent of purchase costs through these incentives. The cumulative effect of these efficiency factors, when calculated over a typical ownership period, often reveals that premium equipment from an established large cube ice maker manufacturer costs less to own and operate than cheaper alternatives, despite higher initial pricing, making it the financially prudent choice for serious operators.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000