Intelligent Water Management and Purification Systems
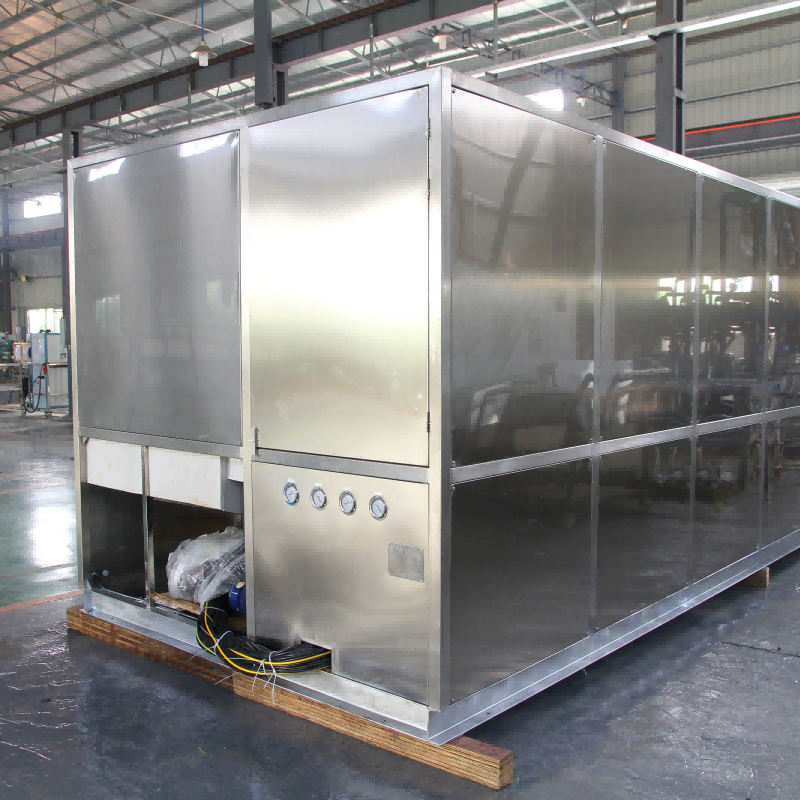
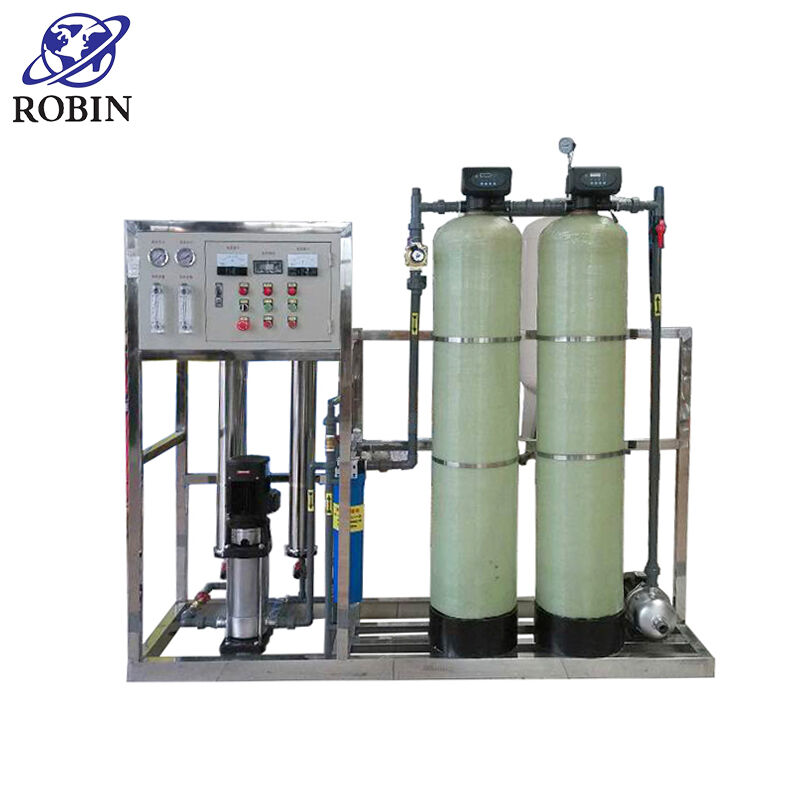
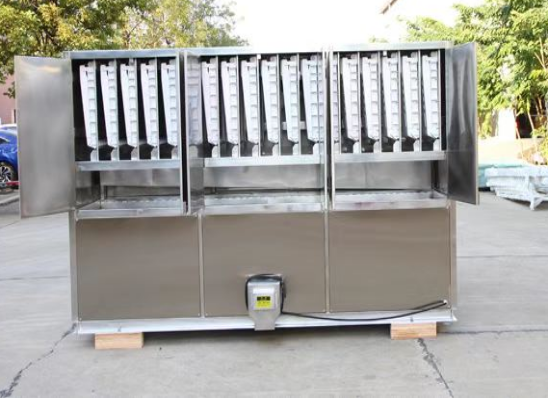
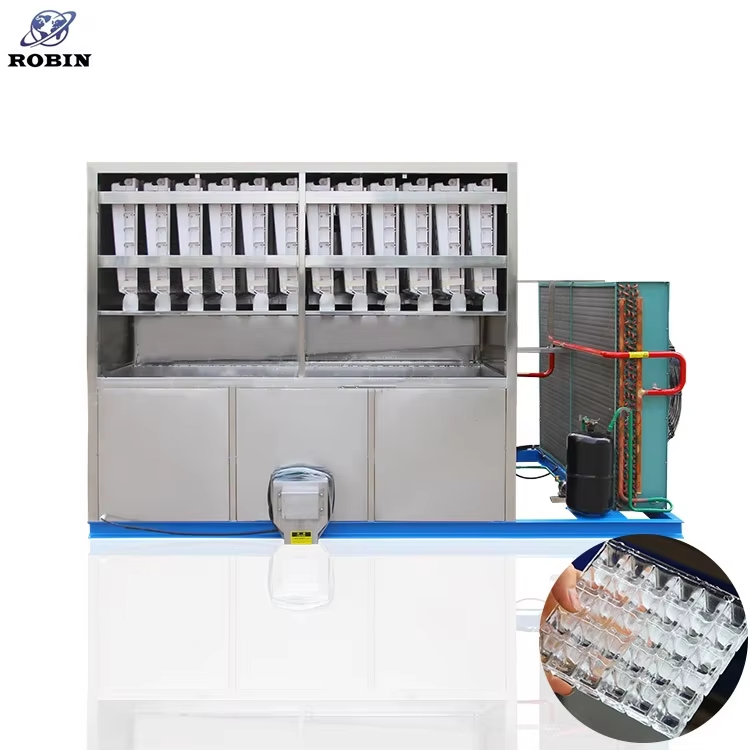
The water management capabilities of an ice cube making machine industrial distinguish professional equipment from consumer-grade alternatives, delivering ice quality that meets the exacting standards of commercial applications. These sophisticated systems begin with multi-stage filtration that removes sediment, chlorine, minerals, and organic compounds that would otherwise compromise ice clarity, taste, and safety. The filtration process typically employs sediment pre-filters that capture particles down to five microns, protecting downstream components from abrasive damage while improving water clarity. Activated carbon filters then remove chlorine and organic compounds that cause unpleasant tastes and odors, ensuring your ice enhances rather than detracts from beverage quality. Many industrial ice cube making machines incorporate scale inhibition technology that prevents mineral deposits from accumulating on evaporator surfaces, a critical feature in areas with hard water that would otherwise require frequent descaling maintenance. The water distribution system represents another area of technological sophistication, with precision-engineered spray nozzles or flooding mechanisms that ensure uniform water coverage across all ice-forming cells. This uniform distribution proves essential for producing consistent cube sizes and preventing weak spots that cause premature melting or structural failure. Advanced industrial models feature water recirculation systems that capture and reuse water that does not freeze during each production cycle, significantly reducing water consumption compared to once-through designs. The intelligent controls monitor water quality parameters including conductivity and temperature, automatically adjusting fill volumes and cycle timing to compensate for seasonal variations or supply changes. Automatic flushing cycles periodically purge the water system, preventing bacterial growth and mineral concentration that could compromise ice safety or machine performance. The ice cube making machine industrial incorporates overflow protection with multiple redundant sensors that prevent water damage from component failures or supply pressure surges. Sanitary design principles guide every aspect of water contact surfaces, with smooth stainless steel construction that resists bacterial colonization and facilitates thorough cleaning. The water inlet connections feature backflow prevention devices that protect municipal water supplies from contamination, ensuring compliance with plumbing codes and health regulations. Temperature monitoring throughout the water system ensures incoming water falls within optimal ranges for efficient freezing, with alerts when supply temperatures exceed design parameters. This comprehensive water management approach guarantees that every ice cube produced meets the highest standards for purity, consistency, and safety.

 EN