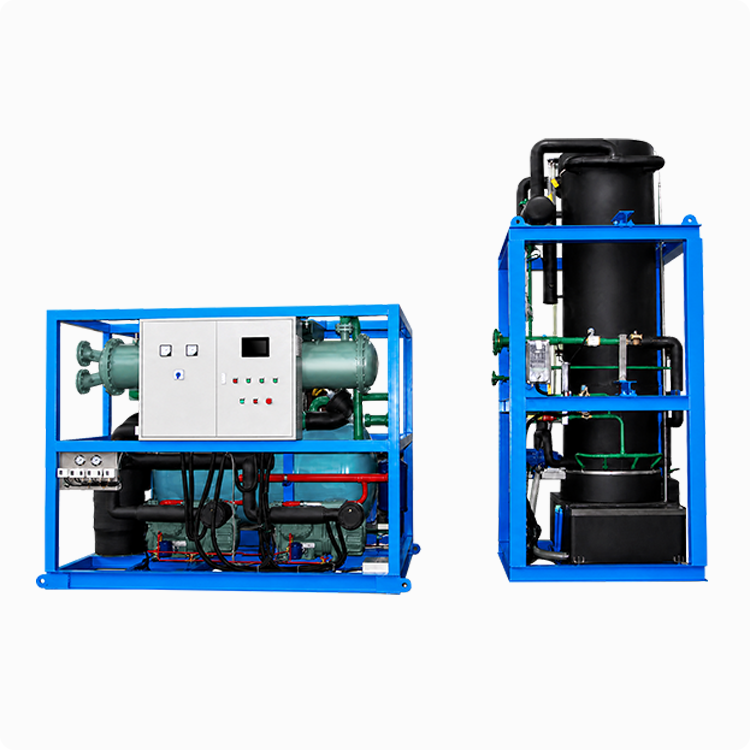
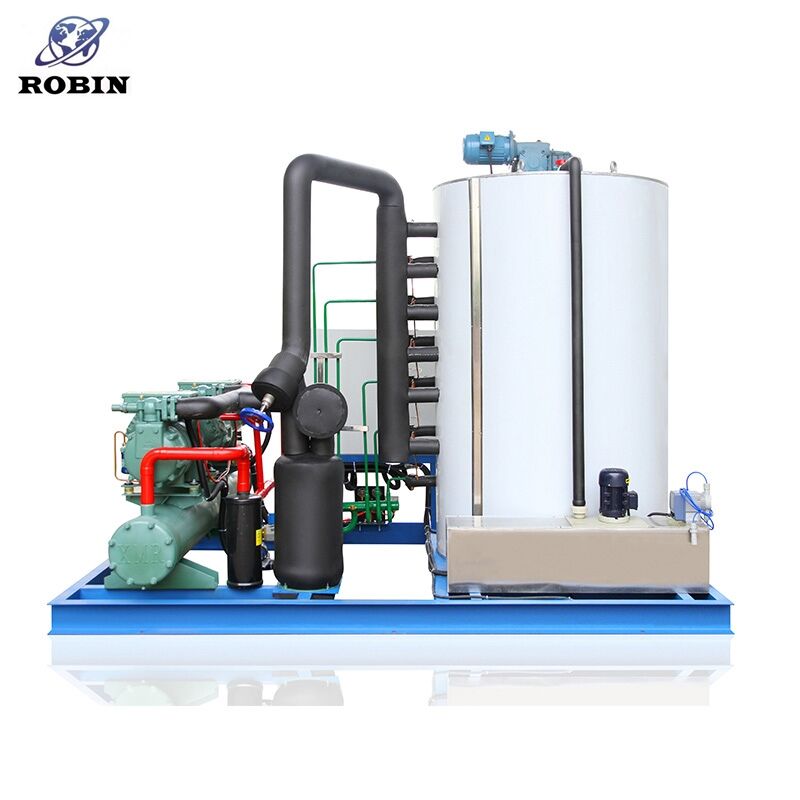
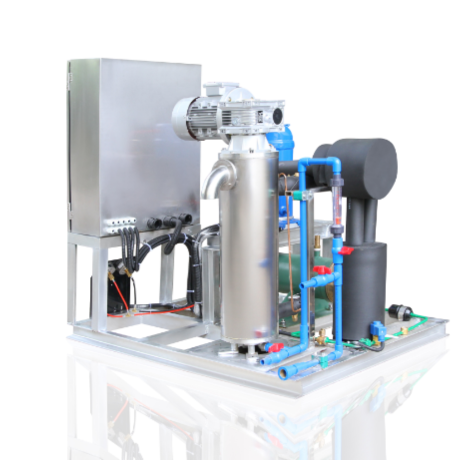
Customized Flake Ice Machine Solutions - Precision Cooling for Commercial and Industrial Applications

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

customized flake ice machine

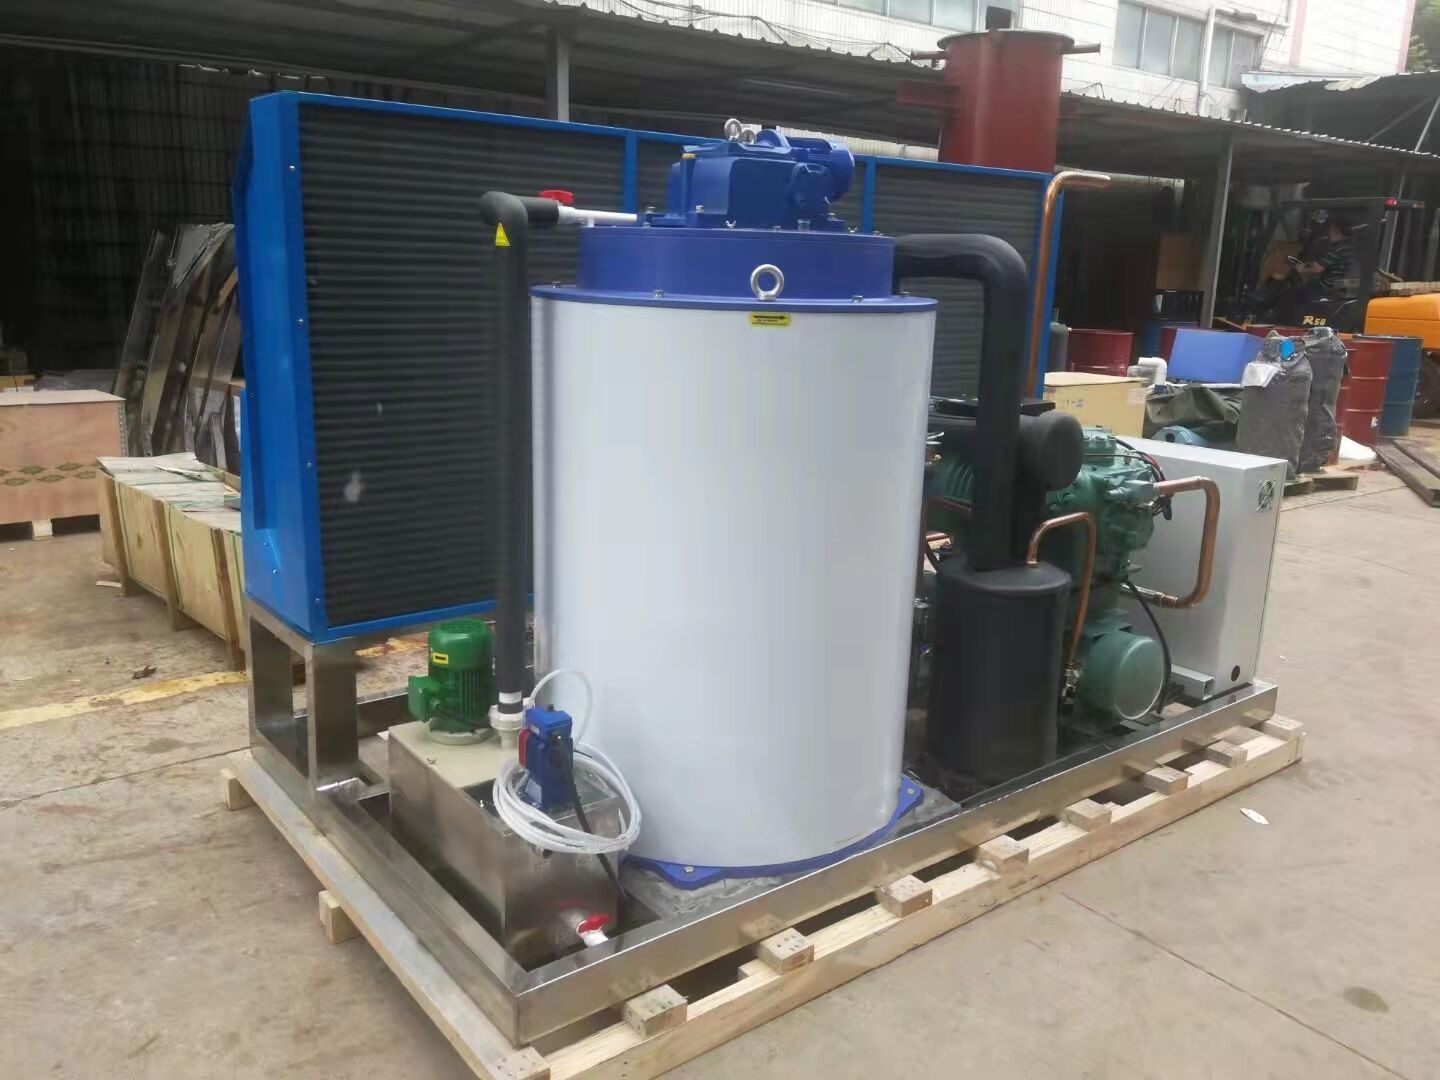
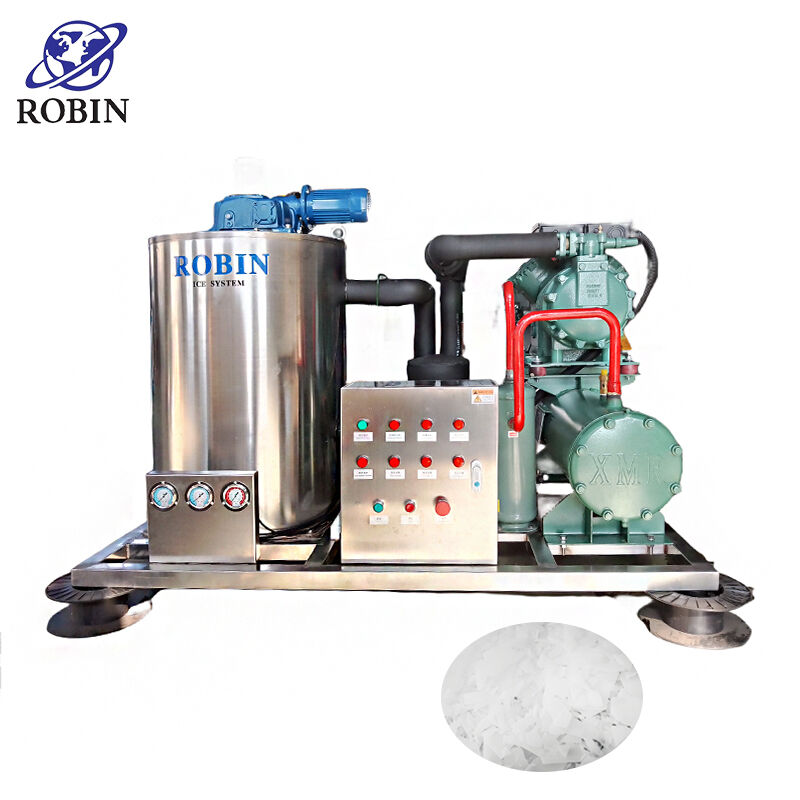
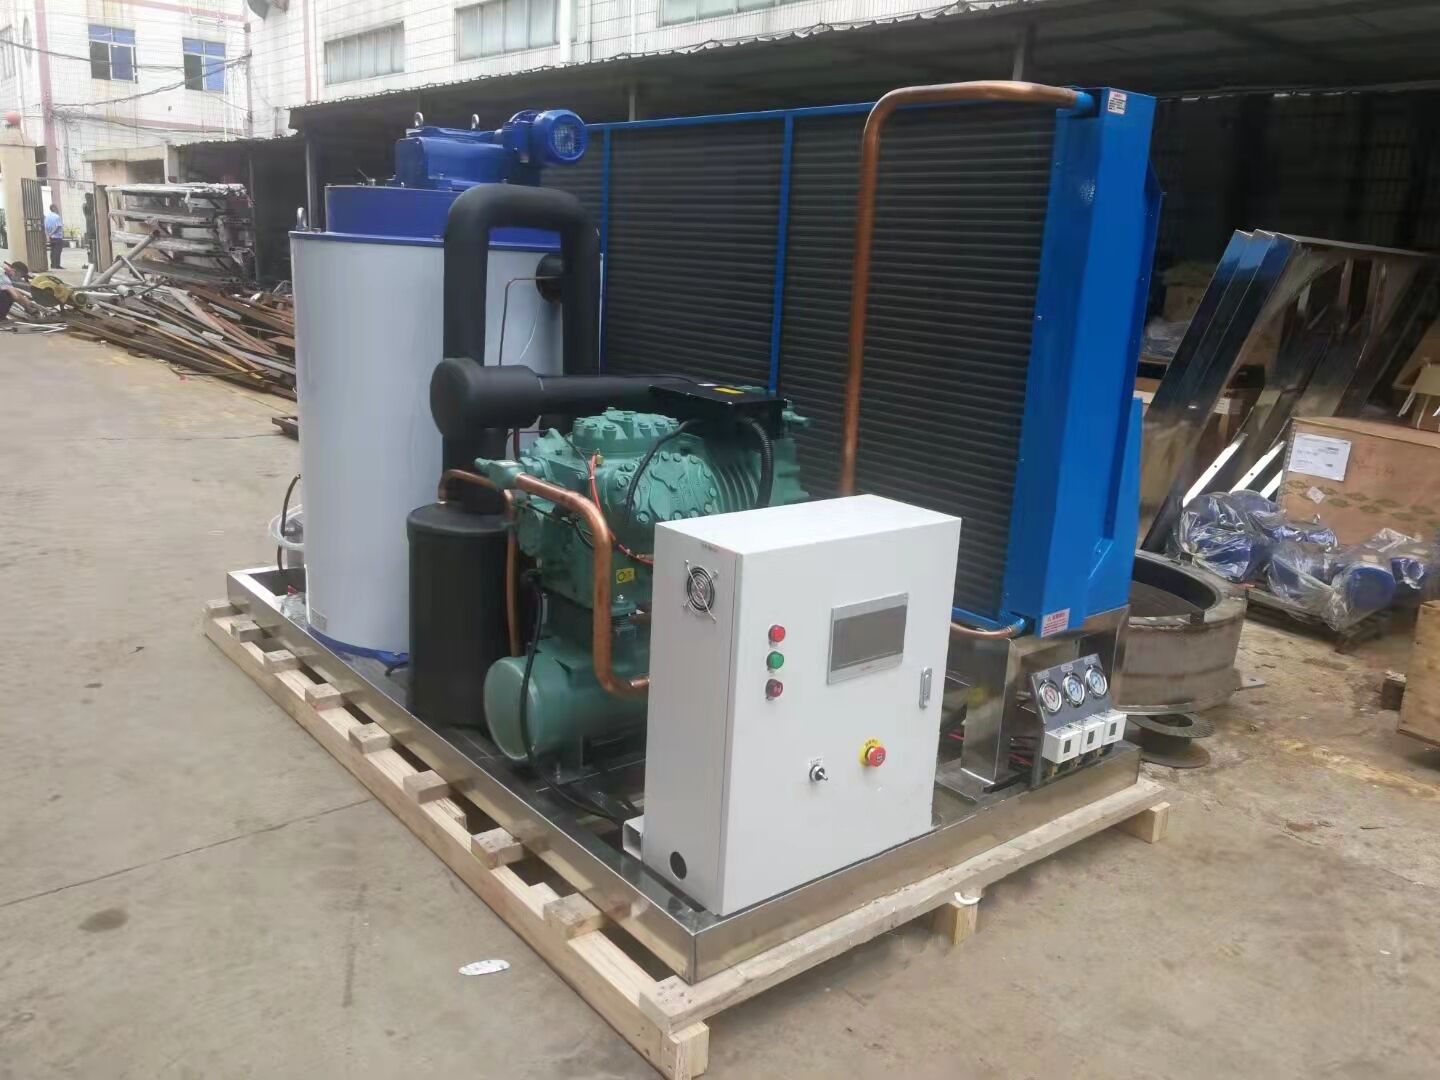
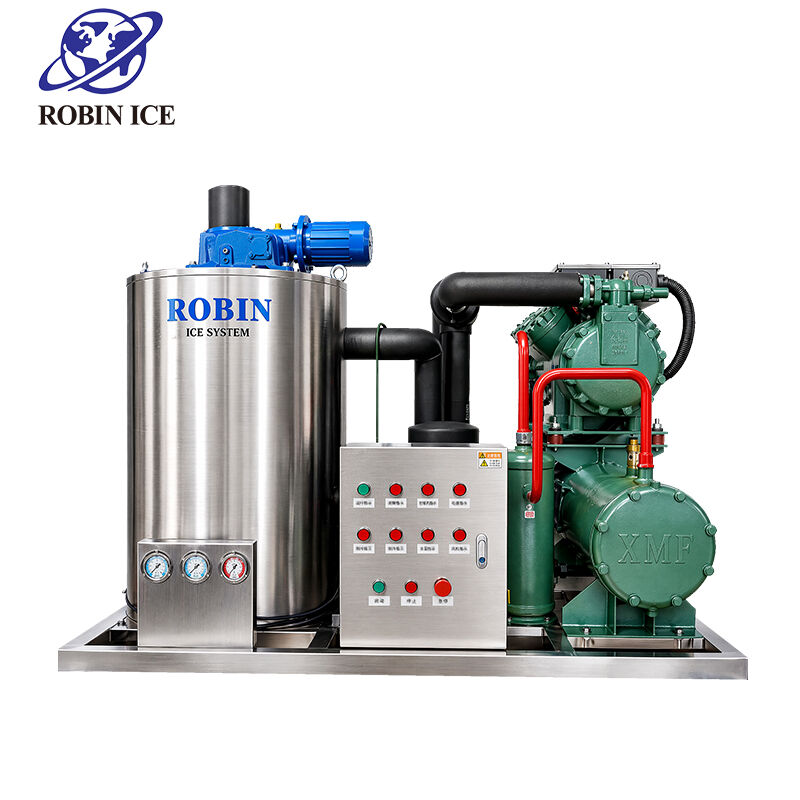
A customized flake ice machine represents a specialized refrigeration solution designed to produce thin, flat ice crystals that offer superior cooling performance across diverse industrial and commercial applications. Unlike standard ice-making equipment, these machines are engineered to meet specific operational requirements, allowing businesses to optimize their ice production according to unique environmental conditions, production volumes, and quality standards. The core function of a customized flake ice machine centers on generating consistent, high-quality flake ice through an advanced evaporator drum system where water freezes on a rotating cylinder and is continuously scraped off by specialized blades. This process creates ice flakes typically measuring 1-2mm in thickness with irregular shapes that maximize surface area contact. The technological features integrated into these systems include variable-speed compressors that adjust cooling capacity based on demand, intelligent control panels with programmable settings for different production schedules, and corrosion-resistant materials that ensure longevity in harsh operating environments. Modern customized flake ice machines incorporate energy-efficient refrigeration cycles, automatic water filtration systems, and remote monitoring capabilities that enable operators to track performance metrics in real-time. Applications for these machines span numerous sectors including seafood processing facilities where rapid cooling preserves freshness, concrete mixing operations that require temperature control during curing, medical laboratories needing sterile ice for specimen preservation, supermarket display cases maintaining optimal product temperatures, and food processing plants where ingredient cooling is critical. The customization aspect allows manufacturers to modify ice production capacity ranging from several hundred kilograms to multiple tons per day, adapt machine dimensions to fit available floor space, select appropriate power configurations matching local electrical infrastructure, and incorporate specialized features such as saltwater ice production for marine applications or ultra-clean ice generation for pharmaceutical use. This flexibility makes customized flake ice machines invaluable for businesses seeking tailored solutions that align precisely with their operational workflows and quality requirements.

New Product Releases

Investing in a customized flake ice machine delivers substantial practical benefits that directly impact your operational efficiency and bottom line. The primary advantage lies in the exceptional cooling speed that flake ice provides compared to other ice forms. Because each flake has a large surface area relative to its volume, it makes immediate contact with products and transfers cold temperatures rapidly, reducing cooling time by up to forty percent in many applications. This speed translates to better product quality, especially for perishable goods like fish, poultry, and produce that deteriorate quickly without proper temperature management. Another significant benefit comes from the machine's ability to mold around irregular shapes. Unlike cube or block ice that leaves air gaps, flake ice fills spaces completely, creating uniform cooling that prevents hot spots and ensures consistent temperature distribution throughout your storage or display areas. The customization aspect means you get equipment sized exactly for your needs, eliminating the waste of over-capacity systems that consume unnecessary energy or under-capacity units that cannot meet peak demand periods. You can specify production schedules that align with your busiest hours, reducing energy costs during slower periods while ensuring adequate supply when you need it most. Modern customized flake ice machines incorporate smart technology that monitors system performance and alerts you to maintenance needs before breakdowns occur, minimizing costly downtime and extending equipment lifespan. The dry texture of properly produced flake ice means it does not clump together, making it easy to handle, measure, and distribute across your operations without the frustration of breaking apart frozen masses. Water efficiency represents another practical advantage, as these machines recycle unused water and incorporate filtration systems that reduce waste while maintaining ice purity. The modular design of customized systems allows for future expansion, so as your business grows, you can add capacity without replacing your entire ice production infrastructure. Energy consumption receives particular attention in custom designs, with options for heat recovery systems that capture waste heat for other processes, variable-speed components that adjust power usage to actual demand, and insulation packages that minimize thermal loss. Installation flexibility means these machines can fit into tight spaces, integrate with existing refrigeration systems, or operate as standalone units depending on your facility layout. The reliability of a properly customized flake ice machine reduces your dependence on external ice suppliers, eliminating delivery delays, quality inconsistencies, and the ongoing expense of purchased ice. You gain complete control over ice production timing, quantity, and quality standards, ensuring your operations never face shortages during critical periods. Maintenance requirements are straightforward, with accessible components that service technicians can reach easily, reducing labor costs and minimizing the time your machine spends offline. The return on investment typically occurs within two to three years for businesses with consistent ice needs, after which the cost savings from eliminated ice purchases and improved operational efficiency contribute directly to profitability.

Practical Tips

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

01

May

Why Do Food Factories Choose Ice Tube Machine for Continuous Ice Supply?

In food processing and manufacturing environments, maintaining a reliable and uninterrupted supply of ice is not a luxury — it is an operational necessity. From chilling fresh produce to controlling temperatures during meat processing, the dema...
View More
How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

12

May

How Does Tube Ice Maker Machine Support Hygienic Ice Supply Operations?

In food processing, healthcare, fisheries, and beverage production, the integrity of ice directly affects product safety and regulatory compliance. A tube ice maker machine is engineered from the ground up to meet the demanding hygiene standards that...
View More
Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

14

May

Can Tube Ice Maker Machine Improve Ice Production in Commercial Facilities?

Commercial facilities that rely on consistent, high-volume ice supply face ongoing pressure to meet demand efficiently without sacrificing quality or operational reliability. Whether the context is food processing, beverages, fisheries, chemical cool...
View More
Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

23

May

Why Do Fisheries Invest in Flake Ice Machine for Fish Preservation Systems?

In the commercial fishing and seafood processing industry, the quality of the catch at the point of sale is directly tied to how well it was preserved from the moment it left the water. Temperature control is not a secondary concern — it is the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

customized flake ice machine

Precision-Engineered Cooling Performance for Maximum Product Quality

Precision-Engineered Cooling Performance for Maximum Product Quality

The customized flake ice machine delivers unmatched cooling performance through its precision-engineered design that prioritizes product quality above all else. At the heart of this capability lies the unique physical characteristics of flake ice itself, which provides superior thermal transfer properties compared to any other ice format available in commercial refrigeration. Each ice flake produced by the machine measures between one and two millimeters in thickness, creating an exceptionally high surface-area-to-volume ratio that enables instantaneous heat absorption upon contact with warm products. This geometric advantage means that when you place fresh seafood, meat, produce, or any temperature-sensitive item onto a bed of flake ice, the cooling process begins immediately and proceeds uniformly across the entire product surface. The importance of this rapid cooling cannot be overstated for businesses handling perishable goods, as every minute of delay in reaching safe storage temperatures increases bacterial growth, accelerates enzymatic degradation, and diminishes the final product quality that reaches your customers. The customized flake ice machine addresses this challenge through its continuous production cycle that maintains a steady supply of fresh, dry ice flakes at optimal temperature. Unlike cube ice that requires time to melt and create cooling contact, or block ice that must be crushed before use, flake ice arrives ready for immediate application in its most effective form. The machine's evaporator drum technology ensures consistent flake thickness and texture throughout production runs, eliminating the quality variations that plague standard ice-making equipment. This consistency matters tremendously in commercial operations where product presentation and food safety standards demand reliable performance. The value this brings to potential customers extends beyond simple temperature control into the realm of competitive advantage. Retailers using customized flake ice machines for seafood displays report longer shelf life, reduced shrinkage from dehydration, and more attractive product appearance that drives higher sales volumes. Food processors benefit from precise temperature management during mixing, blending, and forming operations where ingredient temperatures directly affect final product texture and quality. Medical and laboratory applications require the absolute temperature stability that only properly designed flake ice systems can deliver, ensuring specimen integrity and research accuracy. The customized aspect of these machines allows engineers to optimize every component for your specific cooling requirements, from compressor sizing that matches your thermal load to evaporator surface area that produces your target ice volume. This tailored approach eliminates the compromises inherent in off-the-shelf equipment, delivering cooling performance that aligns perfectly with your quality standards and operational demands.
Energy Efficiency and Operational Cost Reduction Through Smart Customization

Energy Efficiency and Operational Cost Reduction Through Smart Customization

The financial benefits of a customized flake ice machine extend far beyond the initial purchase price, with energy efficiency and operational cost reduction representing perhaps the most compelling value proposition for businesses evaluating ice production solutions. Modern customized flake ice machines incorporate advanced refrigeration technology that dramatically reduces energy consumption compared to older equipment designs or generic ice makers not optimized for specific applications. The customization process begins with a detailed analysis of your actual ice requirements, including daily production volumes, peak demand periods, ambient temperature conditions, and available utility infrastructure. Engineers use this information to select compressor types, sizes, and control strategies that match your load profile precisely, eliminating the energy waste that occurs when oversized equipment cycles on and off frequently or undersized systems run continuously at maximum capacity. Variable-speed compressor technology represents one of the most significant efficiency improvements available in customized systems, allowing the machine to modulate its cooling output in response to actual demand rather than operating at fixed capacity regardless of need. This intelligent adjustment can reduce energy consumption by twenty-five to forty percent compared to fixed-speed designs, with the savings accumulating month after month throughout the machine's operational life. The importance of these energy savings becomes clear when you calculate the total cost of ownership over a typical fifteen to twenty-year equipment lifespan. For a medium-sized operation producing two tons of ice daily, the difference between an efficient customized system and a standard machine can amount to thousands of dollars annually in electricity costs alone. Beyond compressor efficiency, customized flake ice machines incorporate numerous design features that minimize energy waste throughout the refrigeration cycle. Enhanced insulation packages reduce thermal gain from ambient air, keeping the evaporator drum colder with less compressor work. Optimized refrigerant circuits ensure maximum heat transfer efficiency, allowing the system to produce more ice per kilowatt-hour of electricity consumed. Heat recovery options capture waste heat from the condensing process and redirect it to useful purposes such as water preheating or space heating, effectively getting double value from the same energy input. Water efficiency contributes to operational cost reduction as well, with customized systems incorporating recirculation pumps that minimize waste and filtration systems that extend the intervals between cleaning cycles. The smart controls integrated into these machines provide real-time monitoring of energy consumption, ice production rates, and system efficiency metrics, allowing operators to identify optimization opportunities and track the financial returns from their equipment investment. Maintenance cost reduction represents another dimension of operational savings, as customized designs can specify components rated for your specific operating conditions, reducing premature wear and extending service intervals. The value proposition for potential customers becomes compelling when you consider the cumulative effect of these efficiency improvements over time, with many businesses recovering their initial investment premium for customization within three to five years through reduced utility bills, lower maintenance expenses, and eliminated costs for purchased ice from external suppliers.
Uncompromising Hygiene Standards and Food Safety Compliance

Uncompromising Hygiene Standards and Food Safety Compliance

For businesses operating in food service, food processing, healthcare, or any industry where product safety and hygiene are non-negotiable, a customized flake ice machine offers critical advantages in maintaining the highest sanitation standards and regulatory compliance. The importance of ice quality in food safety cannot be overstated, as contaminated ice can introduce pathogens directly into products, beverages, and food preparation processes, creating serious health risks and potential liability exposure. Customized flake ice machines address these concerns through design features specifically engineered to prevent contamination and facilitate thorough cleaning. The evaporator drum surface where ice forms can be specified in food-grade stainless steel with electropolished finishes that resist bacterial adhesion and allow complete sanitization during cleaning cycles. Water filtration systems integrated into customized designs remove sediment, chlorine, minerals, and microbiological contaminants before water enters the ice-making process, ensuring that every flake produced meets or exceeds drinking water quality standards. The closed-loop design of properly engineered systems prevents airborne contaminants from entering the ice production chamber, while antimicrobial materials in water contact surfaces provide an additional layer of protection against bacterial growth. Customization allows you to specify cleaning-in-place systems that automate sanitization procedures, reducing the labor required for maintenance while ensuring consistent application of approved cleaning agents at proper concentrations and contact times. The value this brings to potential customers operating under food safety regulations such as HACCP, FDA guidelines, or local health department requirements is substantial, as documented ice quality control becomes a straightforward process rather than a constant concern. Audit readiness improves dramatically when your ice production equipment incorporates design features that demonstrate your commitment to food safety, from easily accessible components that inspectors can examine to data logging capabilities that document production conditions and cleaning schedules. The smooth surfaces and minimal crevices in properly designed customized flake ice machines eliminate the hiding places where bacteria typically colonize in standard equipment, making visual inspection and verification of cleanliness much simpler. Drainage systems can be customized to prevent standing water that could harbor microbial growth, while air filtration on condenser intakes keeps dust and debris from accumulating on heat exchange surfaces. For businesses serving vulnerable populations such as hospitals, nursing homes, or schools, the enhanced hygiene standards achievable with customized flake ice machines provide essential protection and peace of mind. The ability to produce ice that consistently tests free from coliform bacteria, yeast, mold, and other contaminants supports your broader food safety program and protects your reputation from the devastating consequences of a foodborne illness outbreak. Customization also allows specification of materials and components that withstand aggressive cleaning chemicals without degradation, ensuring that your commitment to sanitation does not compromise equipment longevity. The documentation and traceability features available in modern customized systems create the audit trail that regulatory agencies expect, with time-stamped records of production volumes, cleaning cycles, and any deviations from normal operating parameters that might indicate a food safety concern requiring investigation.


Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000